With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Moisture-containing sodium nitrate is a critical industrial material widely used in sectors such as fertilizer production, chemical synthesis, and energy storage. The efficient and safe transportation of this material is vital for industrial operations, and air-flow transport systems have become a reliable solution. This article provides an overview of the air-flow transport of moisture-containing sodium nitrate, focusing on its structural principles and operational mechanisms.
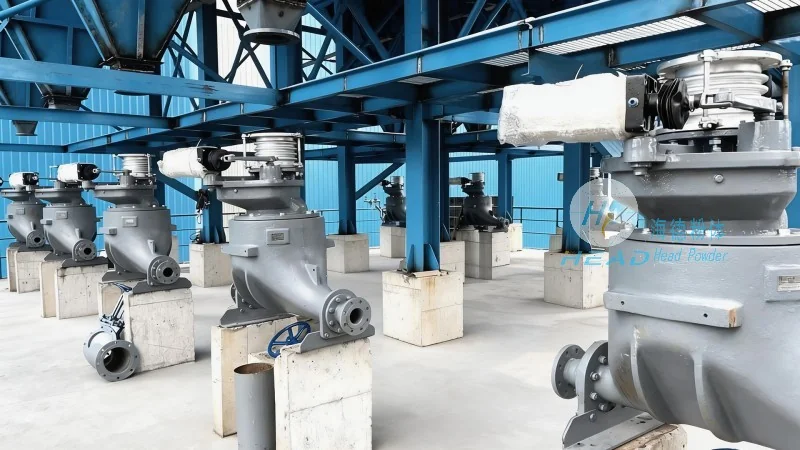
Air-flow transport, or pneumatic conveying, uses compressed air to move bulk materials through a pipeline. This technology is particularly suited for moisture-containing sodium nitrate due to its ability to handle materials with varying moisture levels and particle sizes. The system typically includes a hopper for material storage, a feeder to control flow rate, a pipeline for conveying the material-air mixture, and a receiver for material collection. Compressed air is introduced at controlled pressure and flow to lift and transport material particles.
The air-flow transport system for moisture-containing sodium nitrate features key components designed for efficient operation. The material hopper stores the sodium nitrate, while the feeder regulates the material's entry into the pipeline. The pipeline conveys the material-air mixture, and the receiver collects the material at the destination. Compressed air creates a flow that suspends and moves the material particles through the system.
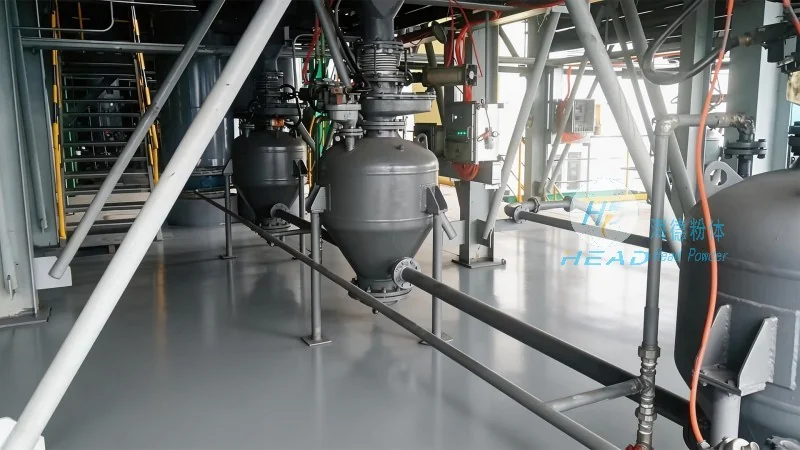
Several structural principles ensure the effectiveness of air-flow transport for moisture-containing sodium nitrate. First, maintaining a consistent air-to-material ratio prevents blockages and pressure drops. This ratio is crucial for smooth material movement through the pipeline. Second, pipeline design—considering diameter and length—optimizes friction losses and maintains necessary air velocity to keep material suspended. Third, using corrosion-resistant materials for the hopper and pipeline ensures durability and safety, especially when handling moisture-containing materials.
Implementing air-flow transport for moisture-containing sodium nitrate requires attention to operational considerations and safety measures. Regular system maintenance, including pipeline cleaning and air pressure checks, prevents material buildup and ensures consistent performance. Monitoring material moisture content and adjusting air flow maintains optimal conveying conditions. Safety measures, such as explosion-proof designs and proper ventilation, protect personnel and equipment from hazards associated with the material.
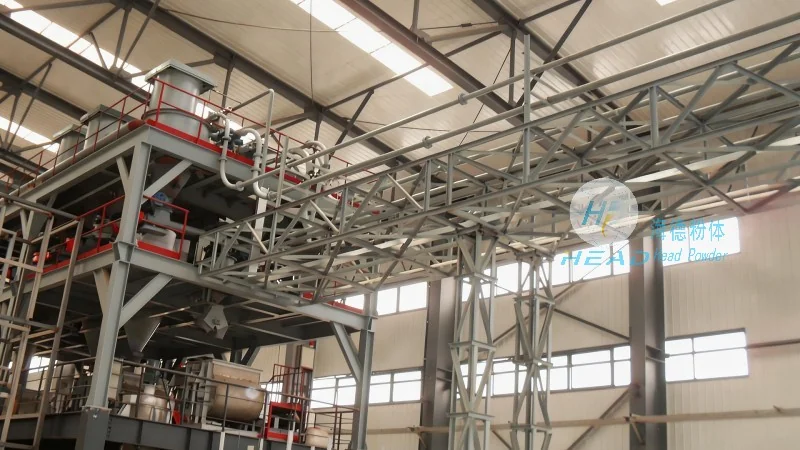
The air-flow transport of moisture-containing sodium nitrate offers benefits for industrial applications. It provides a flexible, space-saving solution for long-distance material transport without extensive infrastructure. Precise flow rate control enables better process management and quality control. The enclosed system reduces dust emissions and environmental impact, making it a more sustainable option compared to traditional methods.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading provider of bulk material handling engineering solutions. Headquartered in Shandong, China, the company specializes in designing and manufacturing air-flow transport systems tailored to industry needs. headpowder's expertise ensures products meet high efficiency, safety, and reliability standards, making them a trusted choice for businesses requiring robust material transport solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top