With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Bulk bag material handling systems are essential in various industrial applications, providing efficient and cost-effective solutions for transporting and handling large quantities of bulk materials. These systems are designed to streamline material flow, enhance operational efficiency, and reduce labor costs in industrial settings. The principle behind these systems revolves around the use of flexible containers, commonly known as bulk bags or super sacks, which are loaded with bulk materials and then transported using specialized equipment. This approach offers significant advantages over traditional methods, such as reduced material handling time and improved safety in the workplace.
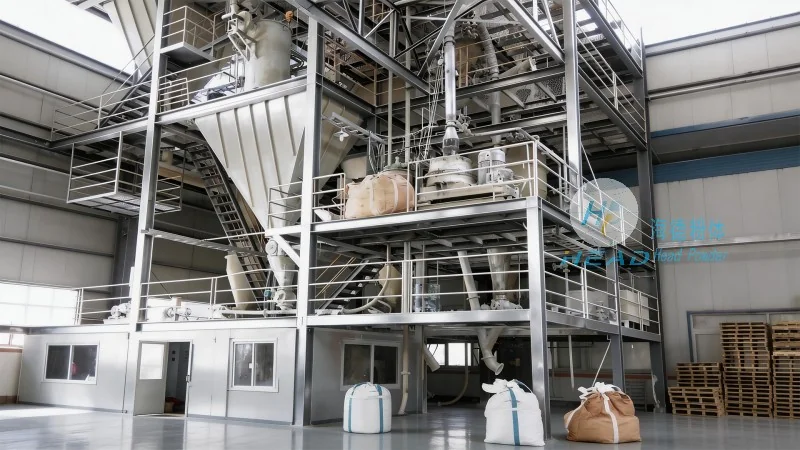
The core principle of bulk bag material handling systems is the utilization of flexible, reusable containers that can hold substantial volumes of bulk materials. These containers are typically made from durable materials like polypropylene or polyester, ensuring they can withstand the weight and stress of heavy loads. The system operates by loading the bulk bag with the desired material, often through a top-loading mechanism or a spout for discharge. Once loaded, the bulk bag is secured and transported to the destination using equipment such as forklifts, cranes, or conveyor systems. The discharge process is usually controlled, allowing for precise material release as needed. This principle ensures that the entire handling process is systematic, reducing the risk of material spillage and improving overall operational safety. Key components of the system include the bulk bag itself, which is designed with reinforced edges and seams to prevent tearing, and a discharge spout or valve that allows for controlled release of the material. Additionally, the system may incorporate a base or pallet to provide stability during transport and storage. These components work together to create an efficient and reliable material handling solution.
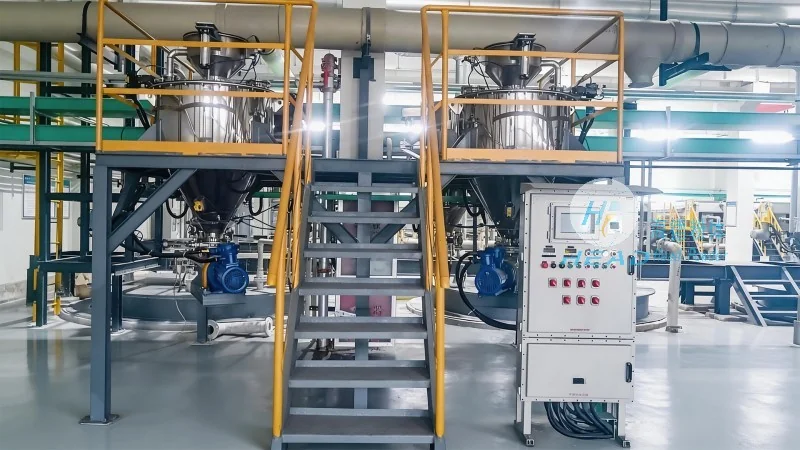
The working scene characteristics of bulk bag material handling systems vary based on the industry and application. In manufacturing facilities, these systems are commonly used for transporting raw materials like chemicals, powders, and granules. The systems are designed to integrate seamlessly with existing production lines, ensuring a continuous flow of materials. For example, in a chemical plant, bulk bag material handling systems are used to transport chemicals such as sodium hydroxide or sulfuric acid, where precise control over material release is critical. The systems allow for gradual discharge, preventing overloading of processing equipment and ensuring safety. In construction sites, bulk bag handling systems are utilized for transporting building materials such as cement, sand, and gravel. The flexibility of bulk bags allows for easy storage and transportation, even in confined spaces. A construction site may use bulk bag material handling systems to deliver cement to a concrete mixing plant, where the cement is discharged directly into the mixer. This approach reduces the need for manual handling and minimizes the risk of material contamination. Additionally, in agricultural settings, these systems are used for handling bulk crops and fertilizers, providing an efficient way to move large quantities of agricultural products. For instance, a farm may use bulk bag material handling systems to transport harvested grains or fertilizers to processing facilities. The systems are designed to handle the varying textures and weights of agricultural products, ensuring efficient transport and storage. The working scene characteristics also include the ability to handle different material types, from fine powders to coarse granules, making bulk bag systems versatile and adaptable to various industrial needs. This adaptability is crucial in industries where material types and processing requirements change frequently.
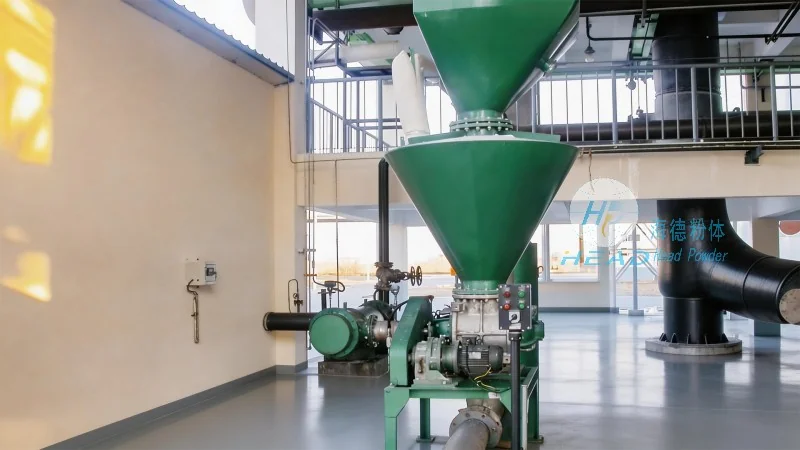
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of bulk bag material handling solutions. With a strong commitment to innovation and quality, HeadPowder specializes in designing and manufacturing efficient material handling systems tailored to the needs of various industries. The company's headquarters is located in Shandong, China, where it leverages advanced technology and expertise to develop cutting-edge solutions. HeadPowder's bulk bag material handling systems are engineered to meet international standards, ensuring reliability and durability in demanding industrial environments. The company focuses on providing comprehensive solutions, including system design, installation, and maintenance, to support clients in optimizing their material handling processes. By combining expertise in engineering and customer service, HeadPowder aims to enhance operational efficiency and reduce costs for its clients worldwide. HeadPowder's team of experienced engineers and technicians work closely with clients to understand their specific material handling challenges and develop customized solutions. The company utilizes state-of-the-art design software and testing facilities to ensure that each system is optimized for performance and safety. HeadPowder also provides training and support services to help clients maximize the benefits of their material handling systems. This comprehensive approach ensures that clients receive not only high-quality products but also long-term support to maintain operational efficiency. The company's dedication to quality and customer satisfaction has earned it a reputation as a trusted partner in the industrial material handling sector.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top