With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Coal ash, a byproduct of coal combustion in thermal power plants, poses significant challenges in handling and transportation due to its granular nature and potential environmental impact. Pneumatic conveying systems have emerged as an efficient and reliable solution for transporting coal ash particles over long distances or within industrial facilities. This article explores the working principle and key features of coal ash particle pneumatic conveying systems, highlighting their applications and benefits in modern industrial operations, provided by Shandong HeadPowder Engineering Co., Ltd.
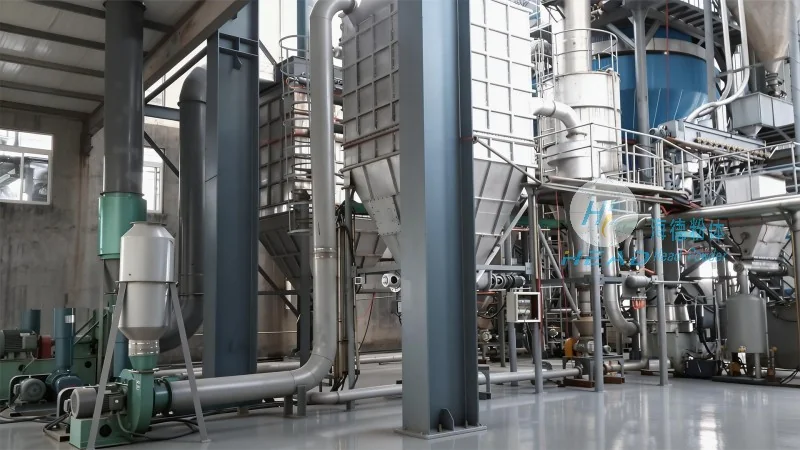
The core mechanism of a coal ash particle pneumatic conveying system involves the use of compressed air or gas to transport solid particles through a pipeline. The system typically consists of a hopper for material storage, a conveyor line (often a flexible or rigid pipe), and a discharge device. When the system is activated, compressed air is introduced into the pipeline, creating a low-pressure zone that draws the coal ash particles into the air stream. The particles are then carried through the pipeline to the destination point, where the air is separated from the solids, and the ash is discharged. The working principle can be categorized into two main types: dilute-phase and dense-phase conveying. Dilute-phase systems use higher air velocities to transport particles in a dispersed state, suitable for short to medium distances. Dense-phase systems, on the other hand, operate at lower air velocities, allowing particles to form a slurry-like flow, which is ideal for long-distance or high-density transport. The choice between these two depends on factors such as the particle size, moisture content, and required transport distance. The system's efficiency is influenced by the air pressure, flow rate, and pipeline design, all of which are optimized to ensure consistent and reliable material transport. Additionally, the system may include components like air filters, cyclone separators, and pressure regulators to maintain performance and prevent particle buildup or air leakage. These components work together to ensure that the coal ash particles are conveyed smoothly and without clogging, which is crucial for maintaining the system's operational efficiency and longevity.
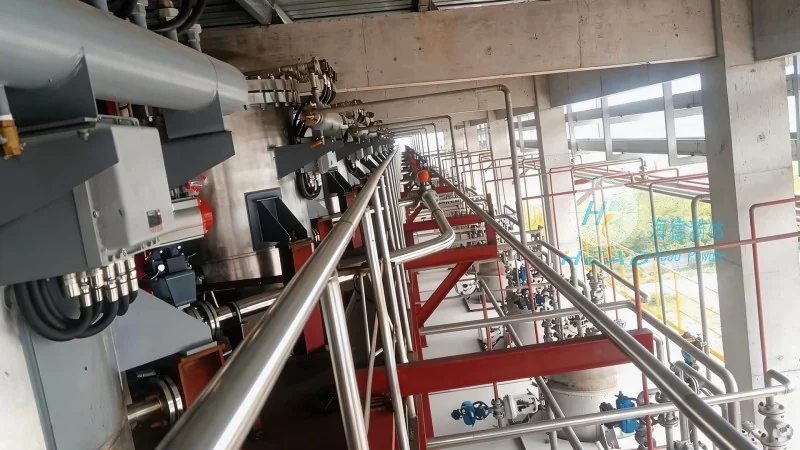
Coal ash particle pneumatic conveying systems offer several distinct features that make them a preferred choice for industrial applications. One of the primary advantages is their ability to handle abrasive and corrosive materials, such as coal ash, without causing significant wear or damage to the equipment. The system's design, which includes robust pipelines and wear-resistant components, ensures long-term durability and minimal maintenance requirements. Another key feature is the flexibility in system layout, as pneumatic conveying systems can be easily adapted to existing industrial facilities or new installations. This adaptability allows for customized solutions that fit specific operational needs, whether for short-distance transport within a power plant or long-distance transport to disposal sites. The systems also provide high transport efficiency, with minimal material loss and reduced environmental impact compared to traditional methods like trucking or belt conveyors. This efficiency is further enhanced by the ability to control the flow rate and pressure, ensuring that the system operates at optimal performance levels. Additionally, the systems are designed to be energy-efficient, with the use of compressed air that can be integrated with existing plant infrastructure, reducing operational costs. The safety features of these systems are also noteworthy, as they eliminate the need for manual handling of coal ash, reducing the risk of dust exposure and accidents. The systems are equipped with safety valves, pressure relief devices, and monitoring systems to prevent over-pressurization and ensure safe operation. Furthermore, the modular design of the systems allows for easy expansion or modification as operational needs change, providing a scalable solution for growing industrial requirements. These features collectively contribute to the effectiveness and reliability of coal ash particle pneumatic conveying systems, making them a vital component in modern coal-fired power plant operations.
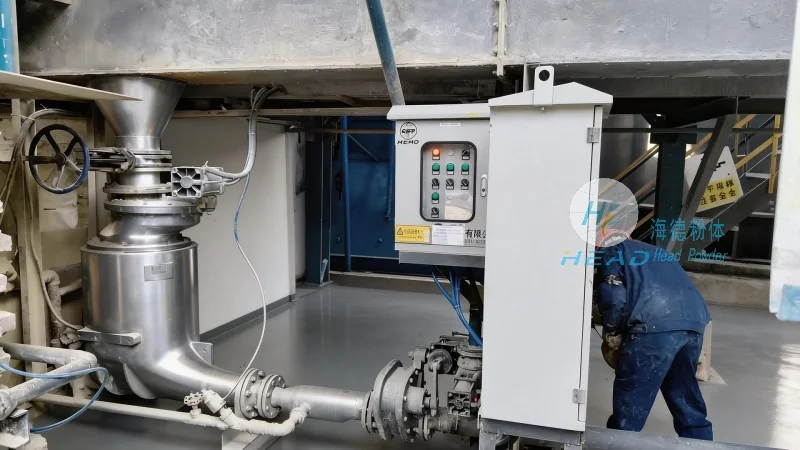
Pneumatic conveying systems for coal ash particles find widespread application in various industrial sectors, particularly in thermal power plants and waste management facilities. In power plants, these systems are used to transport coal ash from the boiler to storage silos or disposal sites, ensuring a continuous and efficient material flow. The ability to handle large volumes of ash particles at high speeds makes these systems ideal for maintaining the operational efficiency of power generation plants. In waste management, the systems are used to transport ash from incineration facilities to landfills or recycling centers, reducing the environmental impact of ash disposal. The benefits of using pneumatic conveying systems in these applications include reduced labor costs, improved safety, and lower environmental emissions compared to traditional transport methods. The systems also contribute to the overall sustainability of industrial operations by minimizing the carbon footprint associated with ash transport. Additionally, the systems can be integrated with other industrial processes, such as ash utilization for cement production or road construction, enhancing the value of the ash as a resource. The adaptability of the systems allows them to be used in diverse applications, from small-scale power plants to large industrial complexes, making them a versatile solution for coal ash handling. The consistent performance of these systems ensures that the ash is transported without degradation or contamination, which is critical for maintaining the quality of the final product in ash utilization processes. Overall, the applications and benefits of coal ash particle pneumatic conveying systems highlight their importance in modern industrial operations, providing a reliable and efficient solution for handling one of the most challenging byproducts of coal combustion.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top