With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industries dealing with bicarbonate of soda, efficient and reliable material handling is crucial. The pneumatic conveying system, specifically designed for bicarbonate of soda, offers a solution that combines performance with safety. This article explores the working principle and key features of such equipment, highlighting how it enhances operational efficiency in various industrial applications.
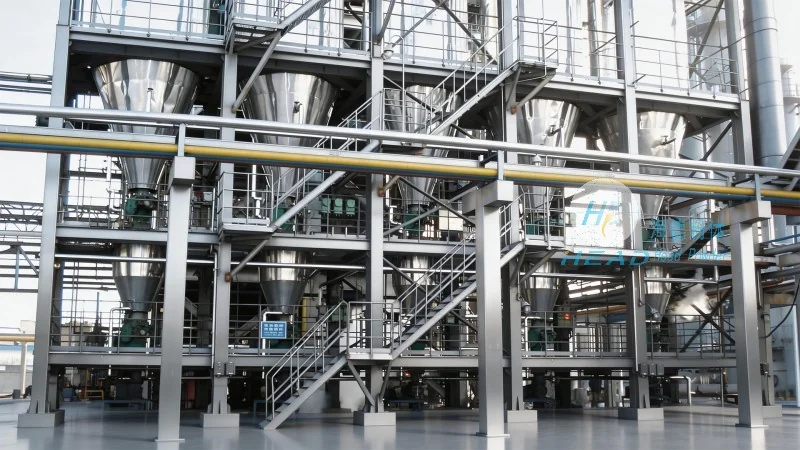
The core of a bicarbonate of soda pneumatic conveying system lies in its ability to transport dry powders like bicarbonate of soda through an air stream. There are primarily two types of pneumatic conveying systems: positive pressure and negative pressure. In a positive pressure system, air is blown into the conveying line, pushing the material forward. Conversely, negative pressure systems use suction to draw the material into the system. For bicarbonate of soda, which is a fine powder, a positive pressure system is often preferred as it provides better control over the material flow and reduces the risk of dust accumulation. The system typically includes a hopper for material storage, a feeder to control the flow rate, a compressor to generate the air pressure, and a conveying line that transports the material to the destination. The air and material are mixed in the line, and the mixture is then separated at the end of the line, with the air being filtered and recycled or vented. This process ensures that the bicarbonate of soda is transported without degradation, maintaining its quality and effectiveness.
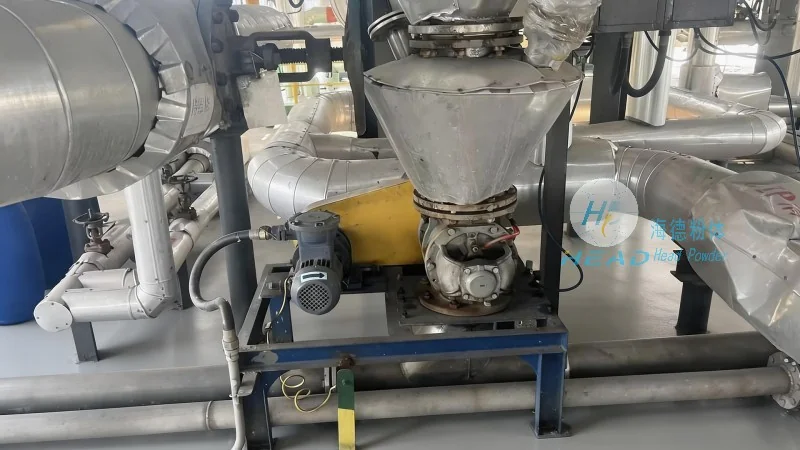
When considering the features of bicarbonate of soda pneumatic conveying equipment, several aspects stand out as critical for industrial use. First, the system is designed to handle the specific properties of bicarbonate of soda, such as its fine particle size and low bulk density. The equipment is constructed with materials that are resistant to corrosion and chemical reactions, ensuring durability and long-term performance. Another important feature is the ability to maintain a clean and dust-free environment, which is essential for food and pharmaceutical industries where contamination must be avoided. The system also offers flexibility in terms of layout, allowing it to be adapted to different plant configurations and space constraints. Additionally, modern systems incorporate advanced controls that allow for precise regulation of flow rates and pressure, enhancing operational control and reducing waste. Safety features are also integrated, such as pressure relief valves and dust collection systems, to prevent accidents and protect personnel. These features collectively contribute to the overall efficiency and reliability of the pneumatic conveying system for bicarbonate of soda.
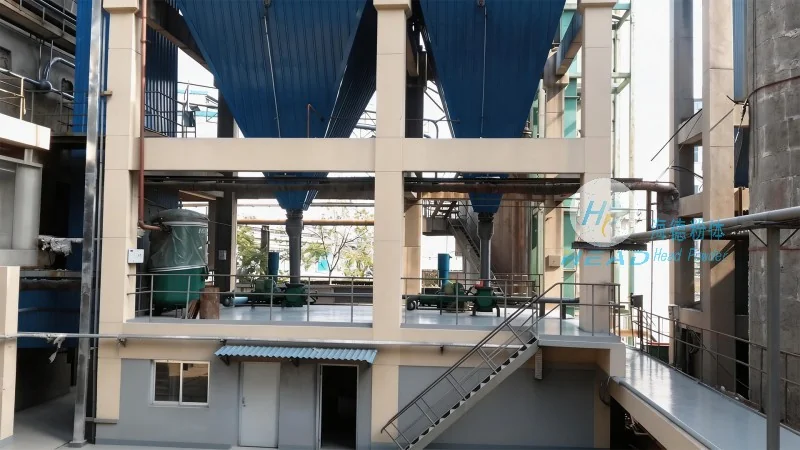
As a leading manufacturer in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in the design and production of high-quality pneumatic conveying systems tailored for various industrial needs. With years of experience and a commitment to innovation, the company has developed equipment that meets the stringent requirements of industries dealing with bicarbonate of soda. HeadPowder's systems are engineered to provide optimal performance, ensuring that clients can achieve efficient material handling while maintaining safety and product quality. The company's headquarters is located in Shandong, China, where it leverages local expertise and resources to deliver reliable solutions to customers worldwide. By focusing on customer needs and technological advancements, Shandong HeadPowder Engineering Co., Ltd. continues to be a trusted partner in the material handling industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top