

Working Principle and Features of Beer Brewery Pneumatic Conveying System
For the efficient handling of beer brewery byproducts such as spent grain or beer pellets, pneumatic conveying systems have become a critical solution in modern brewing operations. This article explores the working principle and key features of a beer brewery pneumatic conveying system, highlighting how it enhances process efficiency and operational reliability.
Introduction to Beer Brewery Pneumatic Conveying Systems
Beer breweries generate substantial amounts of solid waste, including spent grain and beer pellets, which require effective and hygienic handling to maintain production standards and comply with environmental regulations. Pneumatic conveying systems offer a versatile and reliable method for transporting these materials from one location to another within the brewery or to external storage facilities. The system is designed to handle the unique characteristics of beer byproducts, such as moisture content, bulk density, and potential caking, ensuring smooth and continuous operation.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
As a leading provider in the field of material handling solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing advanced pneumatic conveying systems tailored to the needs of the brewing industry. With a strong commitment to quality and innovation, the company has established itself as a trusted partner for breweries seeking efficient and sustainable material transport solutions. HeadPowder's expertise lies in customizing systems to meet specific process requirements, ensuring optimal performance and longevity.
Working Principle of the Beer Brewery Pneumatic Conveying System
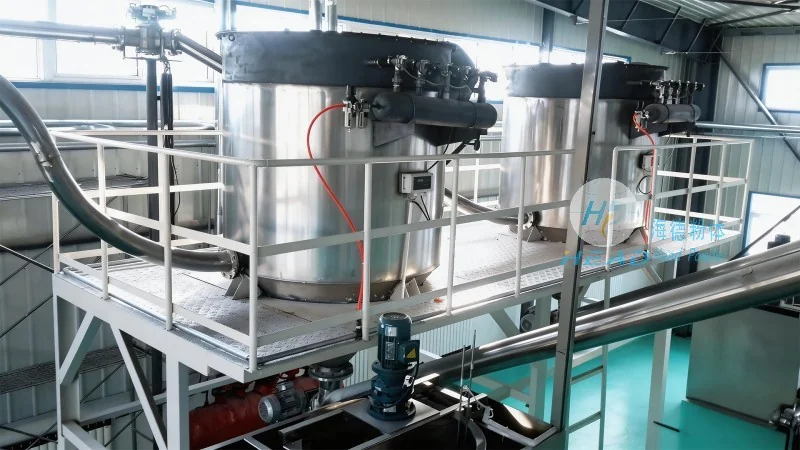
The core of a pneumatic conveying system is the ability to transport bulk materials using air or gas as the conveying medium. In the case of beer brewery applications, the system typically operates under positive pressure, where compressed air is used to move the material through a pipeline network. The process begins with the material being fed into a hopper or feeder, where it is then introduced into the conveying line. As the air flows through the pipeline, it creates a flow of material, carrying it from the inlet to the discharge point. The system may include components such as rotary valves, airlocks, and filters to ensure consistent material flow and prevent blockages.
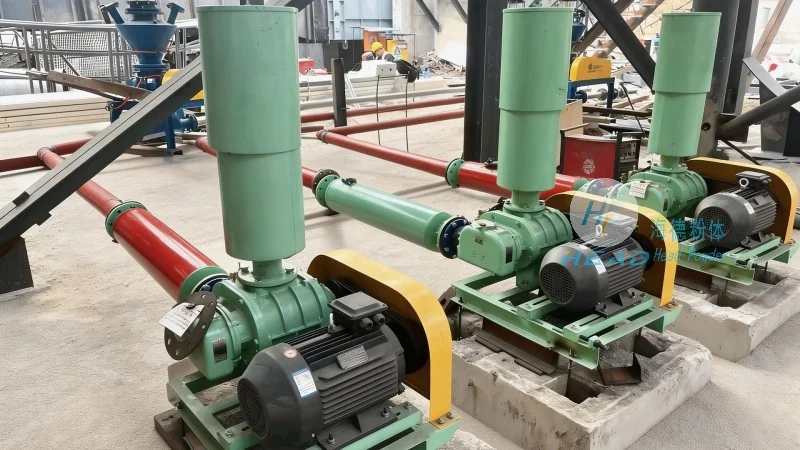
Key components of the system include a blower or compressor that generates the necessary air pressure, a hopper for material storage, and a series of pipes connected to various points of the brewery. The design of the system is optimized to handle the specific properties of beer byproducts, such as high moisture content and potential stickiness, by incorporating features like heated lines or anti-caking agents to maintain material flowability. The system also includes control mechanisms to regulate air pressure and material feed rate, ensuring precise and reliable operation.
Key Features and Advantages of the System
The beer brewery pneumatic conveying system offers several distinct advantages that make it an ideal choice for modern breweries. One of the primary benefits is its ability to handle high volumes of material with minimal labor requirements, reducing operational costs and improving overall efficiency. The system is also highly hygienic, as it operates in closed pipelines, preventing contamination from external sources and maintaining product quality. Additionally, the system is flexible and can be easily integrated into existing brewery infrastructure, allowing for seamless expansion or modification of the conveying network.
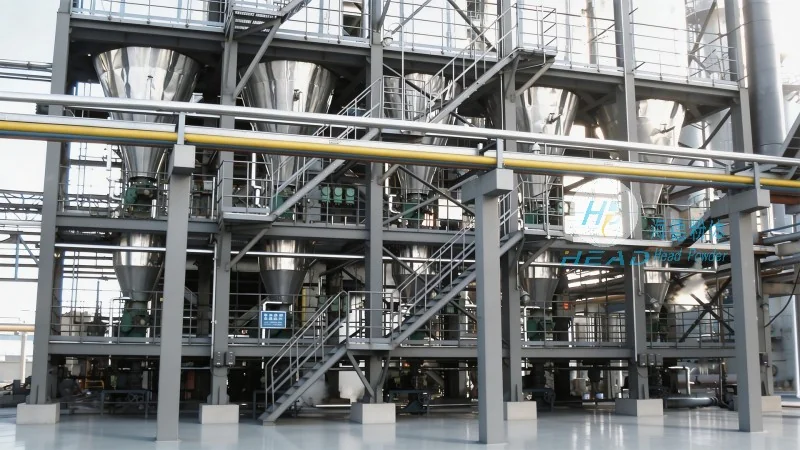
Another significant feature is the system's energy efficiency, which helps reduce operational costs and environmental impact. By using compressed air as the conveying medium, the system minimizes the need for mechanical conveyors, which can be less efficient and more prone to maintenance issues. The system also provides better control over material handling, allowing for precise dosing and delivery of the byproducts to processing or storage areas. This level of control is crucial for maintaining consistent product quality and meeting regulatory standards.
Conclusion and Application
Beer brewery pneumatic conveying systems, as exemplified by the solutions offered by Shandong HeadPowder Engineering Co., Ltd., represent a sophisticated and effective approach to handling brewery byproducts. By leveraging the principles of pneumatic transport, these systems enhance operational efficiency, improve hygiene, and reduce environmental impact. The working principle, which relies on compressed air to move material through closed pipelines, combined with key features such as flexibility, energy efficiency, and hygienic design, makes it a preferred choice for breweries seeking to optimize their material handling processes. With its ability to handle the unique challenges of beer byproducts, the system ensures reliable and consistent performance, supporting the long-term success of brewing operations.