

Working Principle and Features of Centralized Feeding System Equipment
Centralized feeding system equipment is a specialized industrial device designed to efficiently manage and distribute bulk materials within a production environment. This system is crucial for optimizing material handling processes, ensuring consistent material flow, and enhancing overall operational efficiency in various industrial applications.
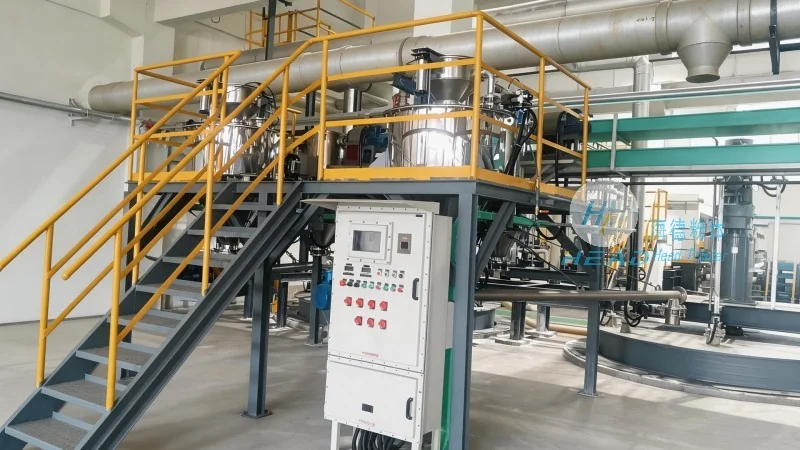
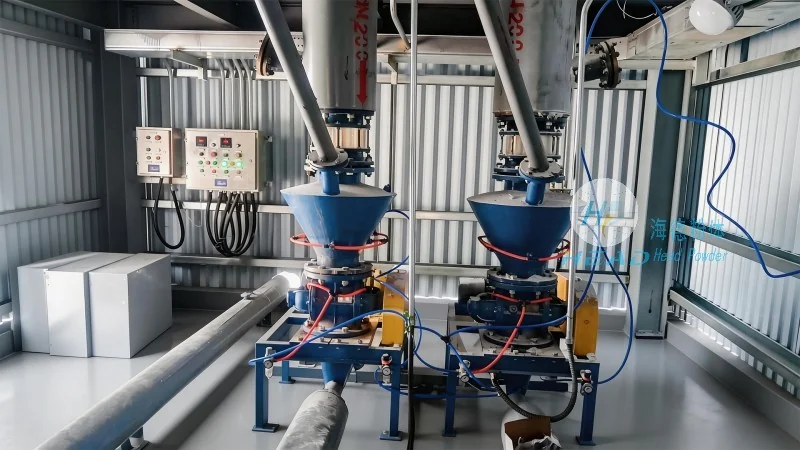
Working Principle of Centralized Feeding System Equipment
The working principle of centralized feeding system equipment revolves around a centralized control mechanism that coordinates the movement and distribution of bulk materials from a single source to multiple destinations. Typically, the system comprises a main hopper or storage unit, a feeding mechanism (such as a screw conveyor, belt conveyor, or pneumatic system), and a network of distribution lines or outlets. The control system, often integrated with sensors and automation technology, monitors material levels, flow rates, and operational status to maintain optimal performance. When material is needed at a specific workstation or processing point, the system activates the appropriate feeding and distribution pathways, ensuring that the right amount of material is delivered at the right time. This centralized approach eliminates the need for individual material handling equipment at each workstation, reducing redundancy and improving material management consistency.
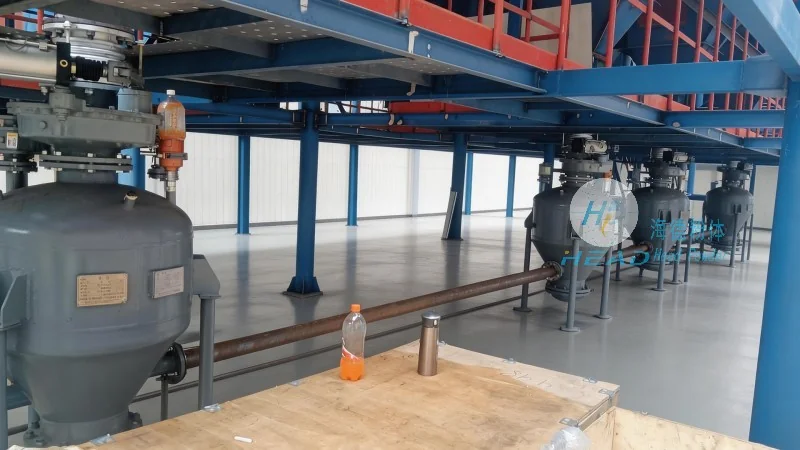
Key Features of Centralized Feeding System Equipment
Centralized feeding system equipment offers several distinct features that enhance its functionality and suitability for industrial applications. One of the primary features is its ability to provide uniform material flow, which is essential for maintaining consistent production quality and reducing material waste. The system's design allows for precise control over material quantity and speed, enabling manufacturers to adjust feeding rates according to production demands. Another notable feature is its space-saving design, as the centralized unit consolidates material storage and handling functions, minimizing the footprint required for material management. Additionally, the system often includes advanced monitoring and diagnostic capabilities, such as real-time data tracking and predictive maintenance alerts, which help in proactive equipment management and reduce downtime. The modular construction of many centralized feeding systems also facilitates easy integration with existing production lines and future expansion, providing flexibility for evolving production needs. Furthermore, the system's ability to handle a wide range of bulk materials, from powders and granules to small parts, makes it versatile for diverse industrial sectors, including manufacturing, pharmaceuticals, and food processing.
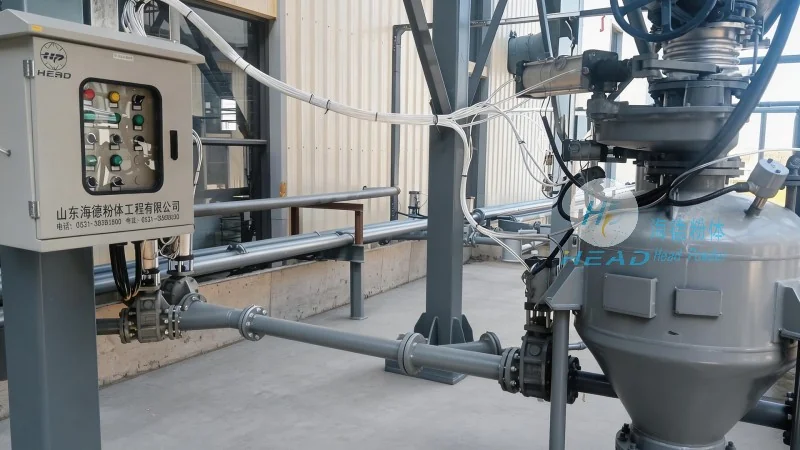
Company Information: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer specializing in the design, development, and supply of centralized feeding system equipment. With a focus on innovation and quality, the company has established itself as a trusted partner in the industrial material handling sector. HeadPowder's products are engineered to meet the specific requirements of various industries, ensuring reliability, efficiency, and durability in demanding operational environments. The company's commitment to customer satisfaction and technological advancement has enabled it to deliver solutions that enhance productivity and streamline material management processes for its clients. Based in Shandong, China, HeadPowder leverages local manufacturing capabilities and industry expertise to provide comprehensive support and tailored solutions for its global clientele.