

What is a Crystal Material Conveying System Equipment? What Are Its Design Principles?
Crystal material conveying systems are specialized equipment designed to handle and transport crystalline materials efficiently and safely. These systems are crucial in various industrial applications, particularly in the chemical, pharmaceutical, and food processing sectors, where the precise movement of such materials is essential for maintaining product quality and operational efficiency. The equipment is engineered to address the unique challenges posed by crystalline substances, such as their tendency to clump, agglomerate, or require controlled temperature and humidity conditions during transport.
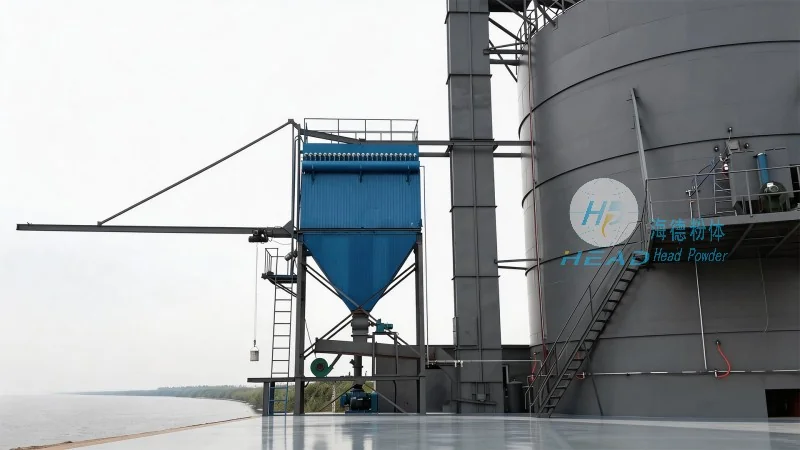
Key Components of Crystal Material Conveying Systems
At the core of a crystal material conveying system are several key components that work in tandem to ensure smooth operation. The primary components include a hopper or feed bin, which serves as the storage and feeding unit for the crystalline material. This component is typically designed with smooth, non-stick surfaces to prevent material buildup and ensure consistent feeding. A conveyor mechanism, often a screw conveyor or a belt conveyor, is then used to transport the material from the hopper to the processing or packaging area. The conveyor system is equipped with adjustable speed controls and may include features like variable speed drives to accommodate different material types and flow rates. Additionally, a control panel or a PLC (Programmable Logic Controller) is integrated to monitor and regulate the entire conveying process, ensuring that the system operates within specified parameters.
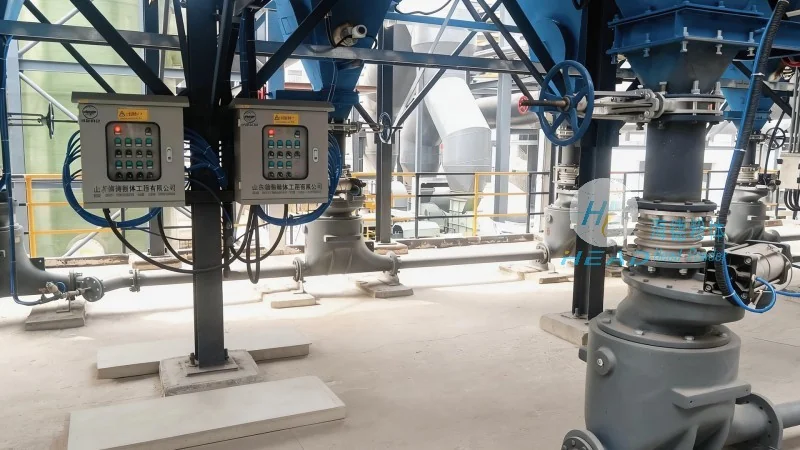
Design Principles for Crystal Material Conveying Systems
The design principles of crystal material conveying systems are centered on several critical factors that ensure optimal performance and reliability. One of the most important principles is the minimization of material degradation during transport. This is achieved through the use of materials for the conveyor components that are resistant to the chemical properties of the crystalline substance, preventing corrosion or reaction that could alter the material's quality. Another key principle is the prevention of material clogging or blockages. This is addressed by incorporating features such as self-cleaning mechanisms, adjustable screw pitch, or the use of flexible conveyor belts that can accommodate irregularly shaped crystals without causing obstruction. Temperature control is also a critical design consideration, as many crystalline materials are sensitive to temperature changes. The system may include heating or cooling elements within the conveyor or the hopper to maintain the material at the optimal temperature, preventing moisture absorption or melting.
Applications and Benefits of Crystal Material Conveying Systems
Crystal material conveying systems find extensive applications across various industries. In the pharmaceutical industry, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients, ensuring that the materials are handled hygienically and without contamination. The precision and control offered by these systems help maintain the purity and stability of the drugs. In the chemical industry, they are employed to transport bulk chemicals, including those that are sensitive to moisture or air, such as fertilizers or specialty chemicals. The food processing industry also benefits from these systems, particularly in the handling of sugar, salt, or other food-grade crystalline products, where maintaining product quality and preventing contamination is paramount. The benefits of using such systems include improved operational efficiency, reduced labor costs, enhanced product quality through better control over the conveying process, and increased safety by minimizing the risk of material spills or accidents.
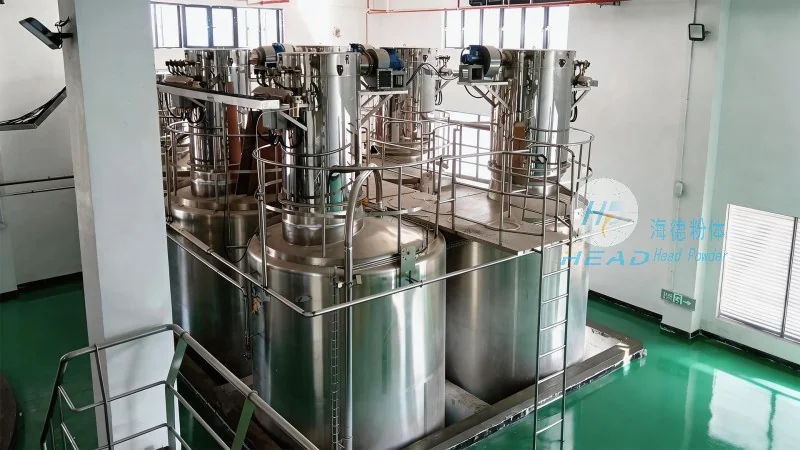
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of specialized material handling equipment, including crystal material conveying systems. The company is headquartered in Shandong, China, and has established itself as a trusted provider of high-quality, customized solutions for various industrial needs. HeadPowder's expertise lies in designing and manufacturing equipment that meets the specific requirements of different industries, ensuring that the systems are robust, efficient, and reliable. The company adheres to stringent quality standards and employs advanced manufacturing techniques to produce equipment that is durable and long-lasting. With a focus on customer satisfaction and innovation, HeadPowder continues to develop new solutions to meet the evolving needs of the market.