With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Phosphorus pentoxide (P₂O₅), also known as phosphoric anhydride, is a highly hygroscopic and reactive chemical compound widely used in industrial applications such as the production of phosphoric acid, flame retardants, and various chemical intermediates. The safe and efficient handling of this material is critical due to its hazardous properties, including strong acidity and potential for exothermic reactions when exposed to moisture. Pneumatic conveying systems have emerged as a preferred method for transporting P₂O₅ powder due to their ability to minimize material contact with air, reduce dust exposure, and maintain process safety. This article explores the fundamental aspects of phosphorus pentoxide pneumatic conveying systems, including their operational principles and key design considerations.
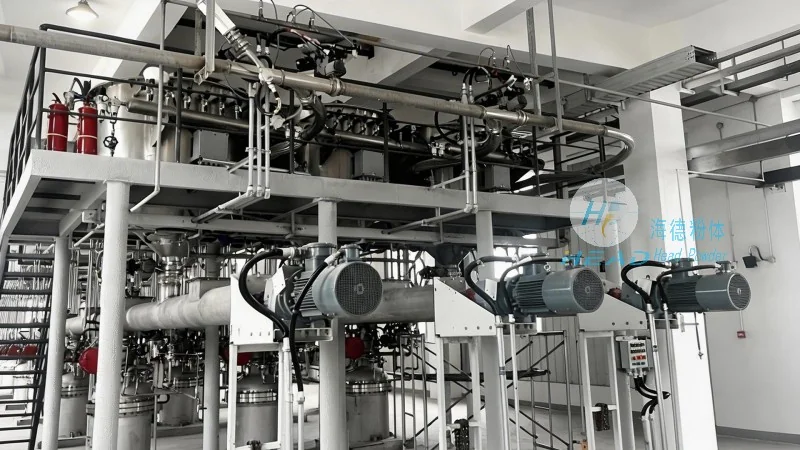
Phosphorus pentoxide pneumatic conveying systems are engineered to transport dry powders like P₂O₅ through a closed pipeline using air or other gas as the conveying medium. Unlike mechanical conveying methods (e.g., screw conveyors or belt conveyors), pneumatic systems rely on the kinetic energy of the gas to move the material, making them ideal for handling fine, abrasive, or hygroscopic powders that are difficult to transport mechanically. The primary goal of these systems is to ensure safe, reliable, and efficient transfer of P₂O₅ from storage or processing units to reactors, reactors to packaging, or between various stages of a production line.
At the core of any P₂O₅ pneumatic conveying system are several critical components that work in tandem to achieve effective material transport. These components typically include a hopper or feeder to control the flow of the powder, a conveying line (usually made of corrosion-resistant materials like stainless steel or PTFE-coated pipes to withstand the acidic nature of P₂O₅), a blower or compressor to generate the necessary air pressure, and a receiver or collection vessel to store the conveyed material. Additionally, systems may incorporate filters, cyclones, or dust collectors to capture any fine particles that escape the conveying line, ensuring environmental compliance and process safety. The selection of each component is critical and must be tailored to the specific properties of P₂O₅, such as its particle size distribution, moisture content, and reactivity.
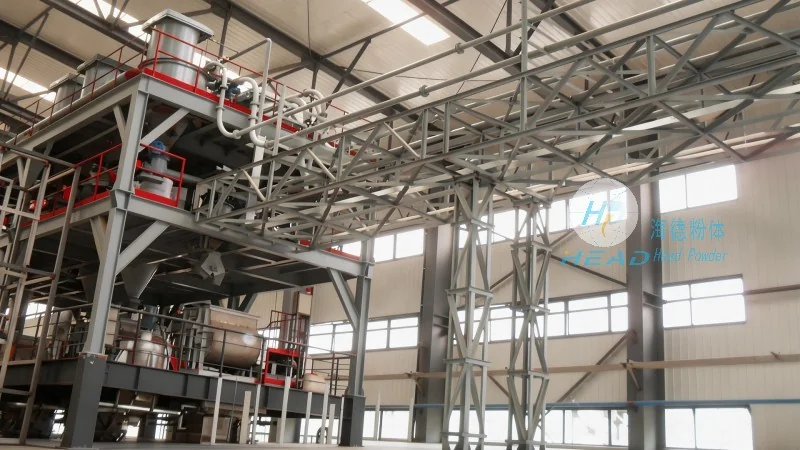
The design of a P₂O₅ pneumatic conveying system follows several fundamental principles aimed at optimizing performance, safety, and longevity. One of the most important considerations is the choice of conveying method—whether it is a dilute-phase or dense-phase system. Dilute-phase systems use high air velocities to transport the powder in a dispersed state, while dense-phase systems use lower air velocities and higher material concentrations to minimize particle degradation and reduce the likelihood of blockages. For P₂O₅, which is a fine powder prone to agglomeration, a dense-phase system is often preferred as it provides better control over particle movement and reduces the likelihood of clogging in the pipeline. Another critical design principle is the prevention of moisture ingress, as P₂O₅ reacts violently with water, generating heat and potentially causing explosions. Therefore, all system components must be hermetically sealed, and the conveying line must be equipped with moisture-proofing measures, such as dry air or nitrogen purging. The system also needs to incorporate pressure relief valves and explosion-proof features to mitigate any potential hazards associated with the material's reactivity.
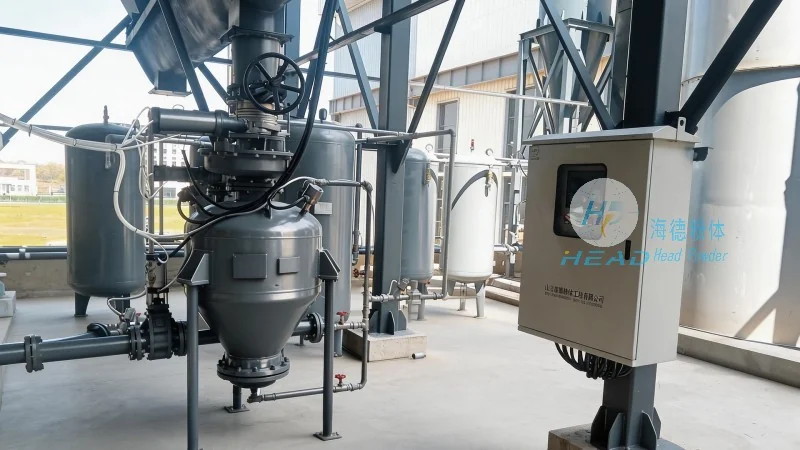
Operating a phosphorus pentoxide pneumatic conveying system requires strict adherence to safety protocols due to the material's hazardous nature. Proper training for operators is essential to understand the risks associated with P₂O₅ handling, including skin and eye irritation, respiratory hazards, and the potential for fire or explosion. The system must be equipped with emergency shutdown (ESD) systems that can quickly stop the flow of air and material in case of an anomaly. Regular maintenance is also crucial to prevent equipment failure, which could lead to leaks or blockages. This includes inspecting the conveying line for wear and tear, cleaning filters and cyclones to prevent clogging, and checking the blower or compressor for proper operation. Additionally, the system should be designed with access points for routine inspections and maintenance, ensuring that all components are easily reachable and serviceable. Environmental considerations are also important, as the system must comply with local regulations regarding dust emissions and waste disposal. Proper filtration and dust collection systems are essential to minimize the release of P₂O₅ particles into the environment.
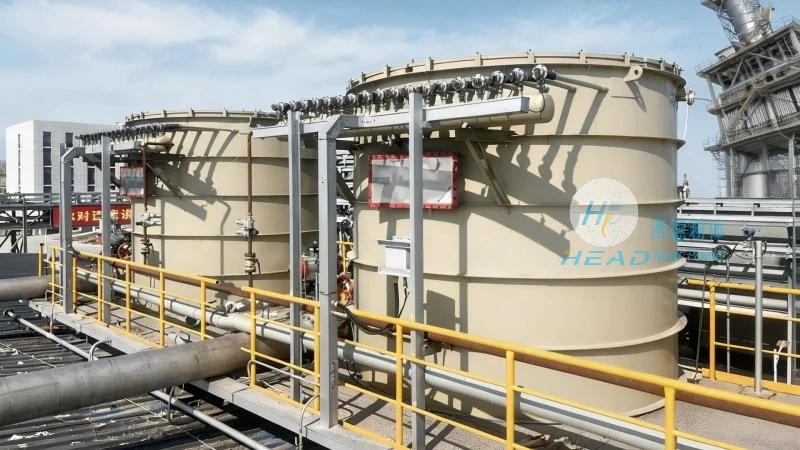
Phosphorus pentoxide pneumatic conveying systems are widely used in various industrial sectors, including chemical manufacturing, pharmaceuticals, and food processing. In the chemical industry, these systems are commonly employed in the production of phosphoric acid, where P₂O₅ is used as a raw material. The ability to transport P₂O₅ safely and efficiently to reactors is critical for maintaining production rates and minimizing downtime. In the pharmaceutical industry, P₂O₅ is used as a desiccant or in the synthesis of certain active pharmaceutical ingredients (APIs), and pneumatic conveying ensures that the material is handled in a sterile and controlled environment. The benefits of using pneumatic conveying for P₂O₅ include improved process safety, reduced labor costs (as manual handling is minimized), and enhanced product quality due to the minimized exposure to moisture and air. Additionally, these systems can be integrated with other process equipment, such as reactors and mixers, to create a seamless production line, further improving operational efficiency.
Phosphorus pentoxide pneumatic conveying systems represent a sophisticated solution for the safe and efficient handling of a highly reactive and hazardous chemical. By leveraging the principles of pneumatic transport, these systems minimize material contact with air, reduce dust exposure, and maintain process safety. The design of such systems requires careful consideration of component selection, conveying method, and safety measures to ensure optimal performance and longevity. As industries continue to rely on P₂O₅ for various applications, the importance of reliable and efficient conveying systems will only grow. Companies like Shandong HeadPowder Engineering Co., Ltd., with their expertise in engineering and manufacturing, play a vital role in providing customized solutions that meet the specific needs of P₂O₅ handling processes. With proper design, operation, and maintenance, P₂O₅ pneumatic conveying systems can contribute significantly to the productivity and safety of industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top