With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Red sugar, a vital ingredient in various food and beverage applications, requires efficient and reliable handling systems to ensure quality and safety throughout the production process. Pneumatic conveying systems have emerged as a preferred solution for transporting red sugar due to their ability to handle fine powders and maintain product integrity. This article provides an in-depth analysis of the red sugar pneumatic conveying system, exploring its components, operational principles, and benefits for industrial applications.
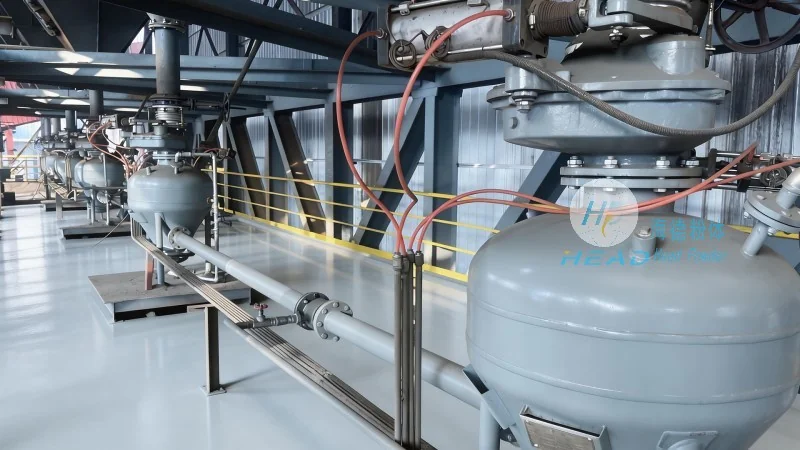
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and installation of advanced material handling solutions. With years of experience in the industry, HeadPowder has established itself as a trusted partner for businesses seeking efficient and cost-effective pneumatic conveying systems. The company's commitment to innovation and customer satisfaction has enabled it to deliver high-quality solutions tailored to the unique needs of the food processing sector.
The red sugar pneumatic conveying system consists of several critical components that work in tandem to ensure smooth and efficient material transport. These components include the hopper for material storage, the feeder to control the flow rate, the air compressor to generate the necessary air pressure, the pipeline network for conveying the material, and the receiver for collecting the conveyed product. Each component plays a crucial role in maintaining the system's performance and ensuring the safe handling of red sugar.
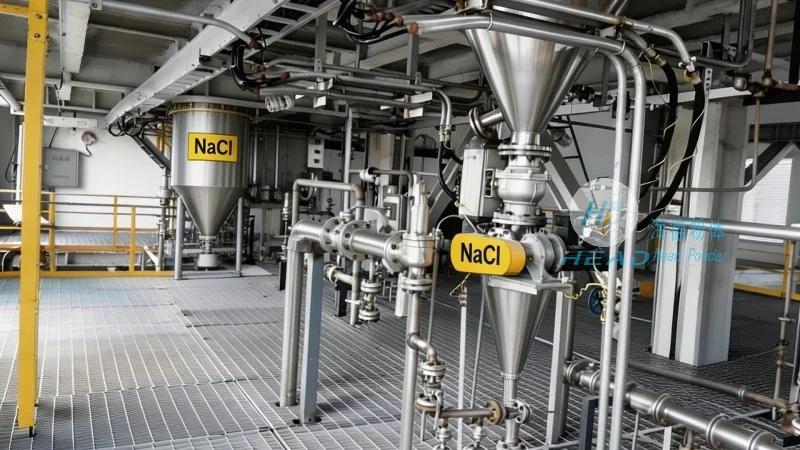
The pneumatic conveying system operates by using compressed air to transport red sugar particles through a pipeline. The process typically involves the following steps: first, red sugar is fed into the hopper from the storage silo. The feeder then regulates the flow of sugar into the pipeline, ensuring a consistent feed rate. The air compressor generates high-pressure air, which is introduced into the pipeline. As the air flows through the pipeline, it entrains the red sugar particles, creating a slurry-like mixture that moves through the system. The receiver at the end of the pipeline collects the conveyed sugar, separating it from the air. This process allows for the efficient transport of red sugar over long distances without the need for mechanical components that could cause contamination or product degradation.
Implementing a pneumatic conveying system for red sugar offers numerous benefits that enhance operational efficiency and product quality. One of the primary advantages is the ability to maintain product integrity, as the system minimizes contact with external contaminants and reduces the risk of dust exposure. Additionally, pneumatic conveying systems are highly flexible, allowing for easy integration into existing production lines and adaptation to changing production volumes. The system also reduces labor costs by automating the material handling process and minimizing the need for manual handling. Furthermore, the compact design of the system saves valuable floor space in industrial facilities, making it an ideal solution for space-constrained environments.
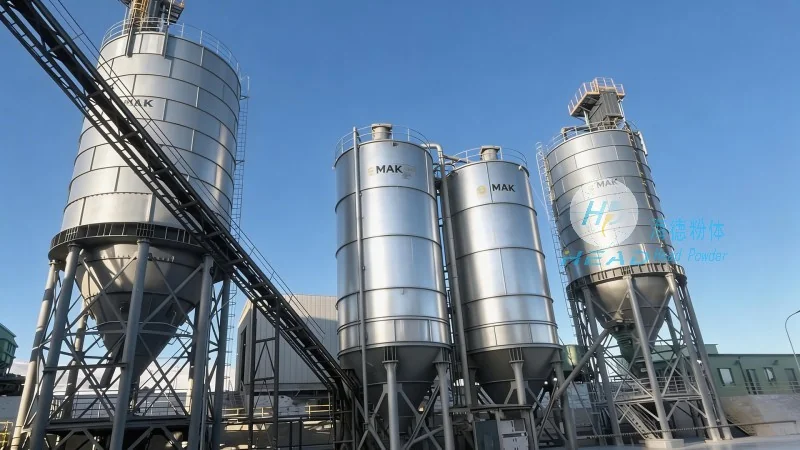
The red sugar pneumatic conveying system is widely used in various industries, including food processing, pharmaceuticals, and chemical manufacturing. In the food industry, it is commonly employed in sugar refineries, confectionery plants, and beverage production facilities to transport red sugar from storage to processing equipment. The system's ability to handle fine powders makes it suitable for applications where product purity is paramount. For example, in the production of red sugar-based confectionery, the system ensures that the sugar is transported without clumping or degradation, maintaining the final product's quality and texture.
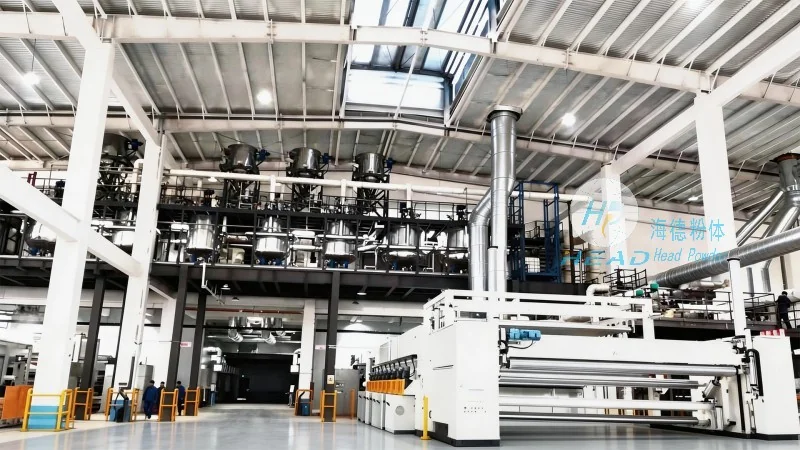
Proper installation and regular maintenance are essential to ensure the optimal performance and longevity of the red sugar pneumatic conveying system. During installation, it is crucial to consider factors such as the system's layout, pipeline routing, and air pressure requirements to minimize energy consumption and maximize efficiency. Regular maintenance tasks include cleaning the hopper and feeder to prevent material buildup, inspecting the air compressor for proper operation, and checking the pipeline for any signs of wear or damage. By adhering to a regular maintenance schedule, businesses can prevent system downtime and ensure consistent product quality.
Red sugar pneumatic conveying systems offer a reliable and efficient solution for handling red sugar in industrial applications. With its ability to maintain product integrity, reduce labor costs, and save space, the system is a valuable asset for businesses in the food processing industry. HeadPowder, with its expertise and commitment to quality, provides comprehensive solutions that meet the specific needs of its clients. By investing in a well-designed pneumatic conveying system, companies can enhance their operational efficiency and ensure the consistent quality of their red sugar products.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top