With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Biological enzyme pneumatic conveying systems represent a sophisticated technology designed to transport powdered or granular materials, particularly those sensitive to moisture or temperature, using compressed air. This method offers advantages such as minimal material degradation, reduced contamination risk, and enhanced operational efficiency compared to traditional mechanical conveying systems. The system integrates specialized components like airlocks, cyclones, and flexible hoses to ensure safe and effective material handling in various industrial applications.
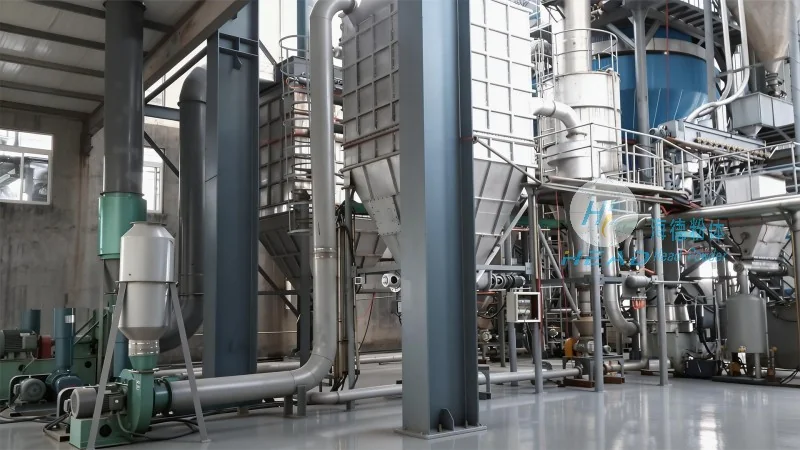
At the core of this technology is the pneumatic conveying principle, where materials are transported through a pipeline by the force of compressed air. For biological enzymes, which are often heat-sensitive and prone to degradation, the system is engineered to maintain optimal conditions. The design typically includes a feeding hopper equipped with a rotary valve to control the flow of material, ensuring a consistent feed rate. Compressed air is introduced into the system, creating a low-pressure or high-pressure environment depending on the application, and propels the material through the pipeline. The system may incorporate features such as air filtration and moisture control to preserve the integrity of the enzymes during transport.
The biological enzyme pneumatic conveying system comprises several critical components, each playing a vital role in the overall operation. The primary components include the material hopper, rotary airlock feeder, conveying pipeline, and receiving hopper. The material hopper stores the biological enzymes and provides a controlled environment to prevent contamination. The rotary airlock feeder acts as a seal between the hopper and the pipeline, allowing material to be discharged into the system while maintaining an airtight seal to prevent air leakage or material spillage. The conveying pipeline, often made of stainless steel or other corrosion-resistant materials, ensures the safe transport of the enzymes. The receiving hopper collects the material at the destination, and may include a cyclone separator to separate any entrained air or fine particles from the material.
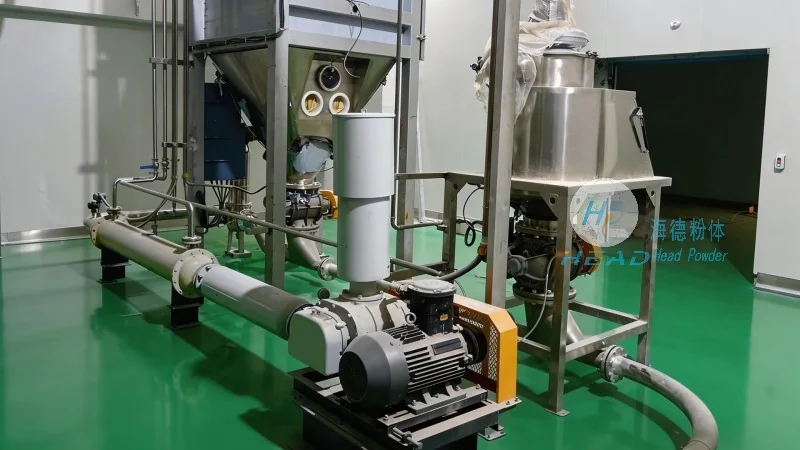
Compared to traditional mechanical conveying methods, biological enzyme pneumatic conveying systems offer several key advantages. Firstly, the system minimizes material degradation by avoiding direct contact with moving parts, which can cause friction and heat generation. This is particularly important for enzymes, as even slight temperature increases can reduce their activity and effectiveness. Secondly, the enclosed system reduces the risk of contamination from external sources, ensuring the purity of the biological enzymes. Thirdly, the system provides greater flexibility in material handling, allowing for vertical, horizontal, or inclined transport of the enzymes. Additionally, the system can handle a wide range of particle sizes and flow rates, making it suitable for various industrial processes.
Biological enzyme pneumatic conveying systems are widely used in industries that rely on enzyme-based processes, such as the food and beverage industry, pharmaceuticals, and biotechnology. In the food industry, these systems are used to transport enzymes used in baking, brewing, and dairy processing. For example, in the production of bread, enzymes like amylases and proteases are transported using pneumatic systems to ensure consistent quality and flavor. In the pharmaceutical industry, enzymes used in drug synthesis and formulation are handled with care to maintain their activity, and pneumatic conveying systems provide a sterile and controlled environment for this purpose. In biotechnology, the system is used to transport enzymes used in genetic engineering and fermentation processes, where maintaining the enzyme's activity is crucial for successful outcomes.
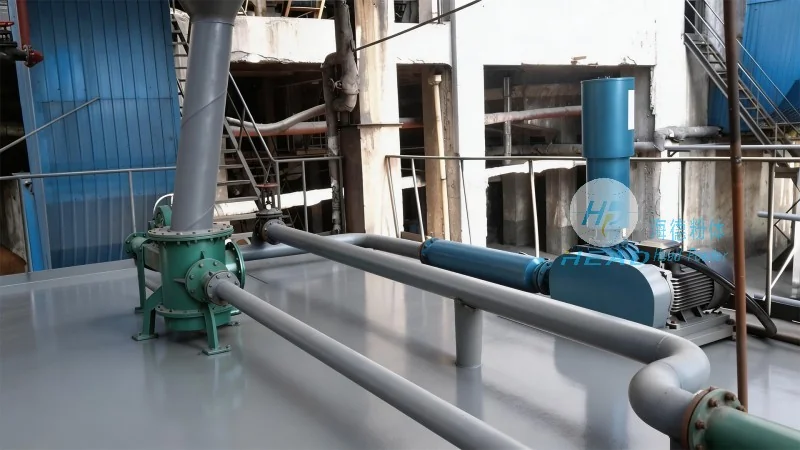
Proper operation and maintenance of the biological enzyme pneumatic conveying system are essential to ensure optimal performance and longevity. Regular cleaning and maintenance of the system components, such as the rotary airlock feeder and conveying pipeline, are necessary to prevent material buildup and contamination. The system should be equipped with air filtration and moisture control systems to maintain the quality of the biological enzymes. Additionally, monitoring the system's pressure and flow rates is important to detect any issues early and prevent material blockages or system failures. Proper training of operators on the system's operation and safety procedures is also critical to ensure safe and efficient operation.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of pneumatic conveying systems and related equipment. The company is headquartered in Shandong, China, and has a strong reputation for providing high-quality, reliable, and efficient solutions for material handling in various industries. With years of experience in the field, headpowder has developed advanced technologies and expertise in designing and manufacturing biological enzyme pneumatic conveying systems that meet the specific needs of its clients. The company's commitment to quality and customer satisfaction has made it a trusted partner for businesses in the food, pharmaceutical, and biotechnology sectors.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top