With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
The recent implementation of a specialized material handling system in Riyadh, Saudi Arabia, stands as a testament to advanced engineering capabilities in the field of industrial logistics. This project specifically addresses the critical need for efficient transfer of sodium bicarbonate powder, a material requiring precise handling due to its unique physical properties. The successful execution of this initiative highlights the growing demand for reliable systems in the Middle East, where industrial efficiency and environmental compliance are paramount. The project was executed by a team dedicated to delivering robust infrastructure, ensuring that the powder handling process meets the rigorous standards expected in the Kingdom's expanding industrial sector.
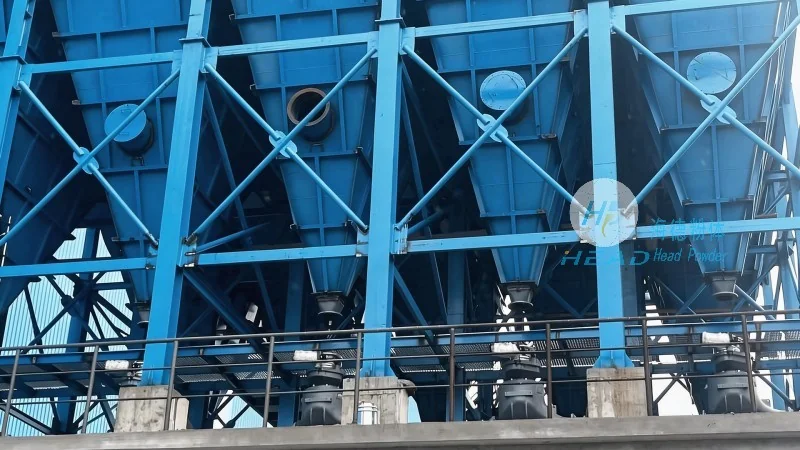
The selection of a negative pressure pneumatic conveying system for this specific application in Riyadh is strategic and technically sound. Unlike positive pressure systems, which force air and material through pipes, negative pressure systems operate by creating a vacuum that pulls material through the pipeline. This method offers several distinct advantages, particularly in dusty environments like industrial facilities in Saudi Arabia. The primary benefit is the containment of dust at the source; because the system is under suction, any potential leaks occur outward, preventing the escape of fine powder into the surrounding atmosphere. This is crucial for maintaining air quality and adhering to strict environmental regulations often found in the Middle East.
Furthermore, negative pressure systems are exceptionally versatile regarding the layout of the facility. In a complex industrial plant, it is often necessary to transfer materials from multiple collection points to a single central receiving hopper or silo. A vacuum system excels in this configuration, allowing for the centralized handling of materials without the need for multiple air compressors or complex piping networks that might be required for positive pressure setups. The system design for the Riyadh project likely utilized this flexibility to optimize the plant layout, reducing the footprint of the piping infrastructure and minimizing the energy required for material transfer.
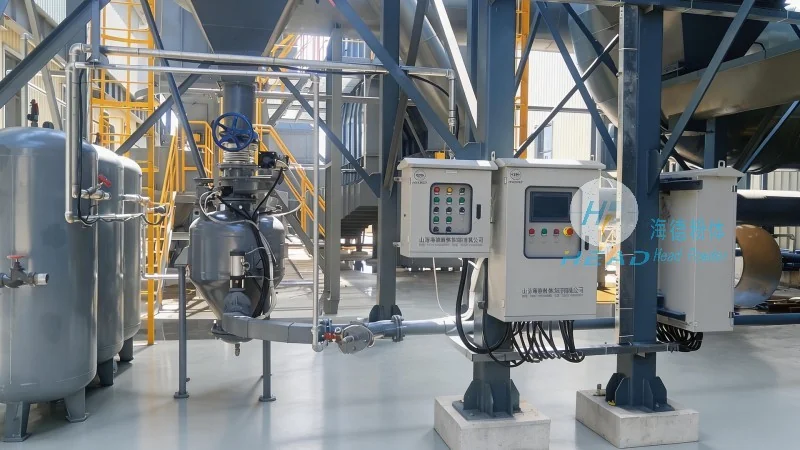
Sodium bicarbonate, commonly known as baking soda, presents specific challenges during the manufacturing and processing stages. It is a fine, white powder that is highly sensitive to physical stress and moisture. When selecting a material handling solution, it is essential to consider the friability of the product; excessive impact or turbulence can cause the powder to break down into finer particles, which can lead to clogging in the conveying lines and inconsistent flow rates. The system designed for the Riyadh facility must therefore balance the need for high transport speed with the need to preserve the integrity of the sodium bicarbonate crystals.
Another critical factor is the flowability of the powder. Sodium bicarbonate can be prone to arching and rat-holing in storage vessels, but in a pneumatic conveying system, the air stream must be carefully controlled to ensure a consistent density of the material in the pipe. The engineers involved in this project focused on optimizing the air-to-material ratio to ensure a stable plug flow. This prevents the powder from bouncing around the pipe walls, which would increase wear on the equipment and risk product degradation. The result is a smooth, uninterrupted transfer of the material that maintains the quality of the sodium bicarbonate from the source to the destination.
Behind the successful deployment of this system is the technical expertise of Shandong Headpowder Engineering Co., Ltd., a company headquartered in Shandong, China. As a specialized provider of bulk material handling solutions, the company brings decades of experience to the table, having completed numerous successful projects across various industries. The Riyadh project is a prime example of their capability to adapt their standard technologies to meet the specific climatic and operational requirements of the Middle East. The engineering team worked closely with the client to understand the nuances of the local facility, ensuring that the equipment was not only functional but also durable enough to withstand the operational demands.
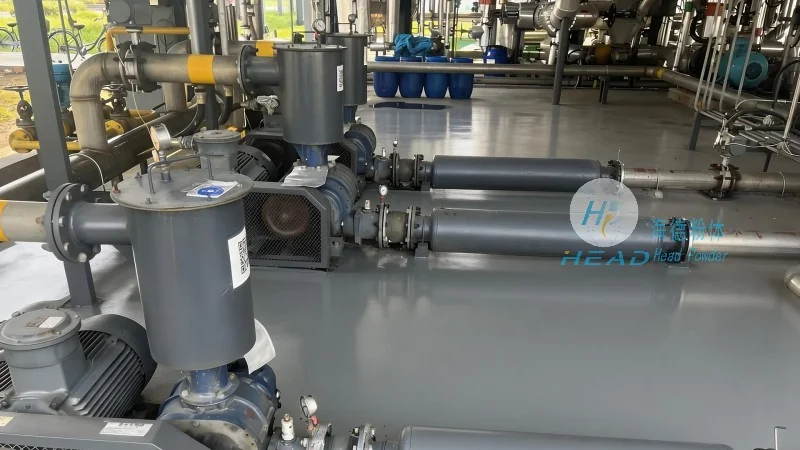
The company’s reputation is built on a foundation of innovation and reliability. By utilizing advanced simulation software and rigorous testing protocols, Shandong Headpowder Engineering Co., Ltd. ensures that every component of the pneumatic conveying system is designed for longevity. From the high-efficiency vacuum pumps to the specialized rotary valves and dust collectors, every piece of equipment is selected to minimize maintenance requirements and maximize uptime. This focus on quality assurance is what sets the company apart in the competitive landscape of industrial engineering and makes them a preferred partner for projects in the region.
This project serves as a significant milestone in the development of pneumatic conveying infrastructure within the Middle East. As industries in Saudi Arabia continue to modernize and expand, the need for dust-free, efficient material handling becomes increasingly critical. The Riyadh facility, by implementing this state-of-the-art system, has set a new standard for operational efficiency. The use of a negative pressure system demonstrates a commitment to safety and environmental stewardship, which are increasingly important considerations for international businesses operating in the region.
The success of this implementation reinforces the viability of pneumatic conveying as a preferred method for handling fine powders like sodium bicarbonate. It provides a clear case study for other facilities in the region looking to upgrade their material handling capabilities. By minimizing manual intervention and reducing the risk of dust explosions, the system enhances the overall safety profile of the plant. The project highlights how modern engineering can address the specific logistical challenges faced by the food, chemical, and pharmaceutical sectors in the Middle East.
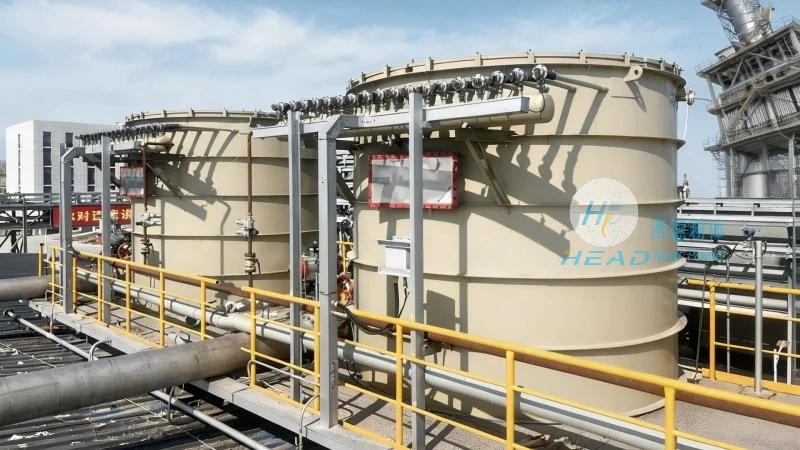
The successful execution of the small soda ash powder negative pressure pneumatic conveying project in Riyadh, Saudi Arabia, underscores the critical role of advanced material handling technology in modern industrial operations. By leveraging the expertise of Shandong Headpowder Engineering Co., Ltd., the facility has achieved a seamless, efficient, and environmentally responsible method for transferring materials. This case exemplifies the high standards of quality and performance that can be expected from a dedicated engineering partner.
For businesses in the Middle East and beyond seeking reliable solutions for powder handling, the experience gained from this Riyadh project offers valuable insights into the benefits of specialized pneumatic conveying systems. To discuss how similar solutions can be tailored to specific operational needs, potential clients are encouraged to reach out to the project team. Contact Mr. Zhang, the project manager, for detailed consultations and technical support. You may reach him via WeChat at 15662777102 to initiate a discussion regarding your material handling requirements and how a customized pneumatic conveying system can enhance your facility's efficiency and safety.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top