With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
In the industrial landscape of South America, the city of Santiago, Chile, stands as a hub for chemical manufacturing and processing. As the sector continues to expand, the demand for reliable, efficient, and safe material handling systems has become paramount. A prime example of this technological advancement is the implementation of a specialized chemical powder negative pressure dilute phase pneumatic conveying system. This project, executed with precision, addresses the critical challenges associated with transporting fine, powdery materials in a chemical environment. The solution not only enhances operational efficiency but also ensures the safety and integrity of the product throughout the entire transfer process.
Chemical powders present a unique set of difficulties for material handling engineers. Unlike bulk solids that are easily handled by gravity or simple belt conveyors, fine powders are prone to issues such as arching, rat-holing, and severe dust generation. In a chemical plant, where dust control is a strict regulatory requirement and product purity is essential, traditional mechanical methods are often insufficient. The risk of cross-contamination, explosion hazards due to fine particulate matter, and energy inefficiency are significant concerns. Therefore, the engineering team in Santiago sought a solution that could provide a sealed, dust-free, and continuous flow of materials from storage silos to processing units.
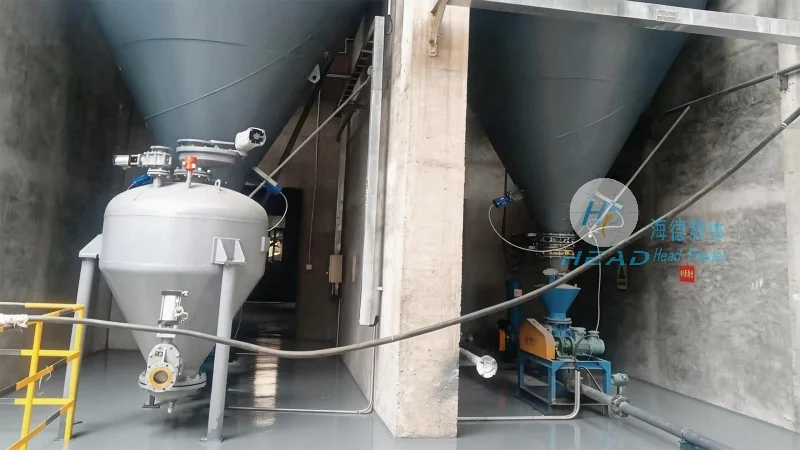
The core of this successful project is the utilization of negative pressure dilute phase pneumatic conveying technology. This method is distinguished by the use of a vacuum source to draw the material into the conveying pipeline. Unlike dense phase systems that use high pressure to push materials, the negative pressure system creates a suction effect that gently pulls the powder through the system.
The "dilute phase" aspect refers to the low density of the material-air mixture within the pipe. This allows for high conveying velocities, which ensures that even cohesive powders remain suspended in the air stream, preventing them from settling and blocking the lines. This technology is particularly advantageous for chemical powders because it minimizes the attrition or breakage of fragile particles, preserving the chemical properties and granulometry of the product. Furthermore, the negative pressure design inherently prevents dust leaks at transfer points, making it an ideal choice for environments where environmental safety is a priority.
Behind the success of this Santiago project is Shandong Headpowder Engineering Co., Ltd., a company renowned for its expertise in pneumatic conveying systems. Headpowder, based in Shandong, China, brought a wealth of experience in designing and manufacturing complex bulk material handling equipment to the table. The company’s engineering team worked closely with the client to analyze the specific flow properties of the chemical powder being handled.
The project required a customized approach, taking into account the specific layout of the Santiago facility and the high standards required by the chemical industry. Headpowder’s engineers designed a robust pipeline network that integrated seamlessly with the client's existing processing equipment. The system was engineered to handle varying flow rates and to accommodate different types of chemical additives, ensuring versatility for future production needs. This level of customization is a hallmark of Shandong Headpowder’s service, distinguishing them from generic equipment suppliers.
The deployment of this negative pressure dilute phase system has yielded significant benefits for the Santiago plant. First and foremost, the system has drastically reduced the labor costs associated with manual handling and cleaning of dust. By automating the transfer process, the plant has achieved a continuous operation that is free from the bottlenecks often caused by manual intervention.
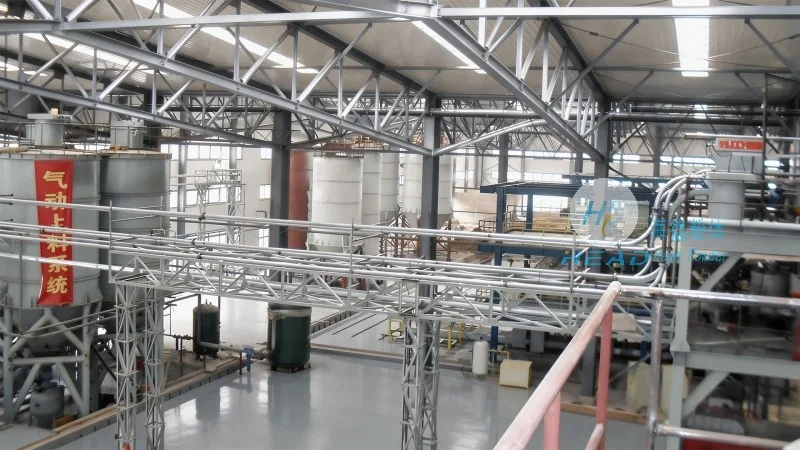
Energy efficiency is another critical advantage. The dilute phase system, while operating at high velocities, is optimized to use compressed air efficiently. The system design minimizes pressure drop across the piping, reducing the energy consumption of the vacuum pump or blower. Additionally, the system's ability to transport materials over long distances and through multiple bends without significant pressure loss ensures that the plant can scale its operations without the need for frequent system overhauls. The sealed nature of the system also protects the chemical powder from moisture and external contaminants, ensuring a higher quality end product.
This project in Santiago is a testament to the growing capability of Chinese engineering firms in the global market. Shandong Headpowder Engineering Co., Ltd. has established itself as a key player in the field of pneumatic conveying, with a strong focus on international markets, including Latin America. The successful delivery of this system highlights the company's ability to meet the rigorous demands of the chemical industry in diverse geographical locations.
The "pneumatic conveying case" in Santiago serves as a reference point for other potential clients in the region who are looking to modernize their material handling infrastructure. It demonstrates that with the right technology and expertise, it is possible to overcome the inherent challenges of powder handling. The system's reliability and low maintenance requirements ensure a high return on investment for the client, solidifying the partnership between the Chilean facility and the engineering team from Shandong.
Safety is the cornerstone of any chemical plant operation. The negative pressure dilute phase system installed in Santiago is designed with multiple safety features to protect both the personnel and the facility. The system is equipped with explosion-proof components and is designed to handle the specific electrostatic properties of the chemical powder being conveyed. By maintaining a negative pressure within the system, any potential leak is immediately drawn back into the pipe, preventing the release of hazardous dust into the atmosphere.
Furthermore, the materials used in the construction of the pipes and components are selected for their chemical resistance and durability. This ensures that the system can withstand the harsh environments often found in chemical processing plants without corroding or degrading over time. The design also incorporates easy-access points for maintenance and inspection, ensuring that the system remains in optimal condition throughout its operational life.
Shandong Headpowder Engineering Co., Ltd. is a premier manufacturer and engineering firm dedicated to the development and supply of advanced powder handling solutions. Headquartered in Shandong, China, the company has built a reputation for excellence through innovation and customer-centric service. The company specializes in a wide range of products, including screw conveyors, bucket elevators, and various types of pneumatic conveying systems.
The company’s philosophy is rooted in providing comprehensive solutions that address the specific needs of each client. Whether it is a small-scale batch process or a large continuous production line, Shandong Headpowder Engineering Co., Ltd. has the technical capability to deliver. Their team of experienced engineers works tirelessly to ensure that every system they design is efficient, reliable, and cost-effective. The Santiago project is just one of many success stories that showcase their global footprint and technical prowess.
For businesses interested in implementing similar advanced material handling systems, the expertise of Shandong Headpowder Engineering Co., Ltd. is readily available. The company is committed to fostering long-term relationships with its clients, providing ongoing support and technical consultation. The success of the Santiago pneumatic conveying case serves as an invitation for other industries to explore the benefits of negative pressure dilute phase technology.
For detailed inquiries and project discussions, interested parties are encouraged to contact the project manager directly. Zhang Manager is available to discuss specific requirements, provide technical documentation, and offer customized solutions tailored to individual production needs. By reaching out to Zhang Manager, clients can take the first step towards optimizing their powder handling operations and enhancing their overall plant efficiency.
Effective communication is essential for the successful execution of large-scale engineering projects. Shandong Headpowder Engineering Co., Ltd. places a high value on clear and responsive communication with its partners. Zhang Manager serves as the primary point of contact for this Santiago project and is ready to assist with any questions regarding the pneumatic conveying system.
For immediate assistance and to discuss how a negative pressure dilute phase system can benefit your facility, please connect with Zhang Manager via WeChat at 15662777102. The team at Headpowder looks forward to collaborating with you to achieve operational excellence in your material handling processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top