With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industries dealing with sulfate of soda, efficient material handling is crucial to maintain production efficiency and operational safety. Air-driven or pneumatic conveying systems offer a reliable solution for transporting this material, especially in scenarios where traditional methods like belt conveyors or bucket elevators may face challenges due to material properties or process requirements. This article explores the fundamental principles behind air-driven sulfate of soda material handling and highlights key working scene characteristics that define its application in various industrial settings.
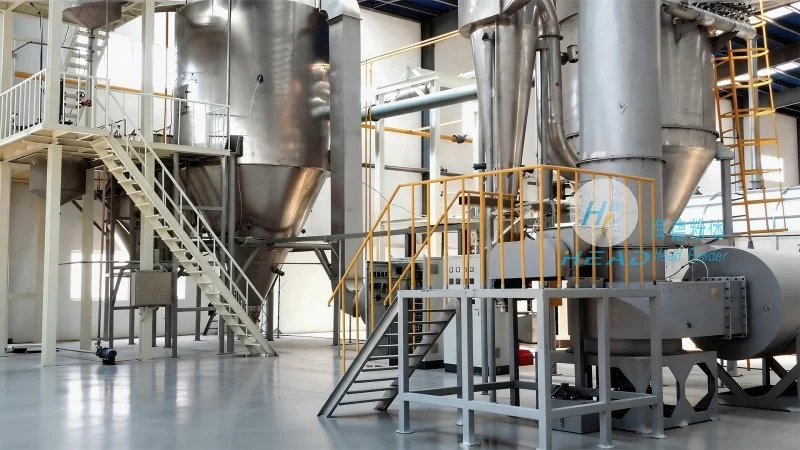
As a leading provider of material handling solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and implementing advanced air-driven systems tailored to the unique needs of industries processing sulfate of soda. With a strong focus on innovation and customer-centric design, the company leverages decades of experience to deliver efficient, reliable, and cost-effective solutions that enhance operational performance and ensure compliance with industry standards. Based in China, the company serves a diverse range of sectors, including chemical processing, food manufacturing, and pharmaceutical production, where the safe and efficient transport of sulfate of soda is critical to overall process success.
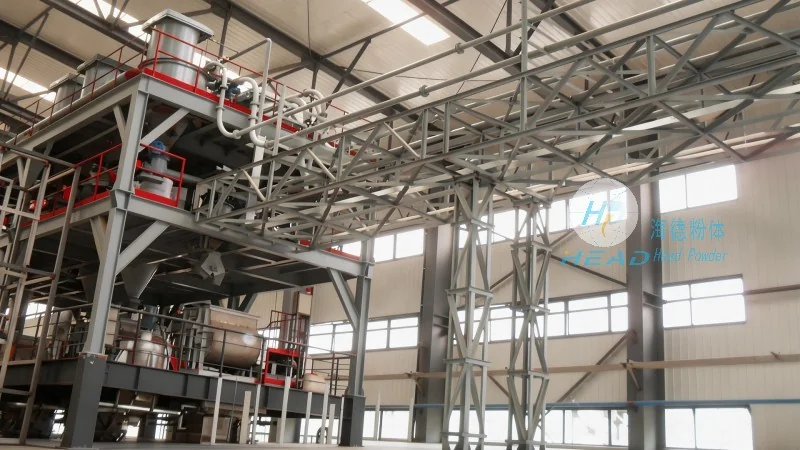
At its core, air-driven material handling relies on the use of compressed air or vacuum to move bulk materials through a network of pipes. For sulfate of soda, which is typically a fine or granular powder, the system operates by creating a flow of air that lifts and transports the material particles. There are two primary modes of operation: positive pressure (pressure) and negative pressure (vacuum). Positive pressure systems use a blower to generate air pressure that pushes the material through the pipeline, while negative pressure systems employ a vacuum pump to draw the material into the system. The choice between these modes depends on factors such as material characteristics, distance to be conveyed, and system layout. In the case of sulfate of soda, its relatively low moisture content and moderate particle size make it well-suited for both positive and negative pressure applications, though positive pressure is often preferred for longer distances or when handling larger quantities due to its higher efficiency and lower energy consumption.
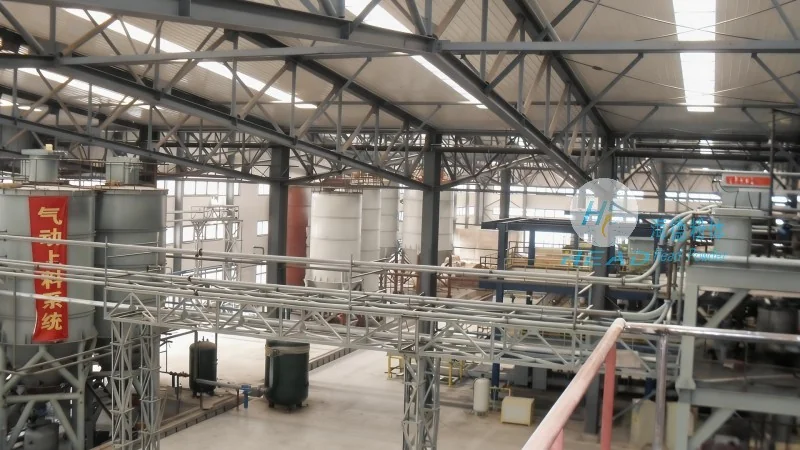
The application of air-driven sulfate of soda material handling is defined by several key characteristics that make it ideal for specific industrial scenarios. First, the system’s ability to handle fine or granular materials without the need for mechanical components like belts or buckets reduces the risk of material degradation or contamination. This is particularly important for sulfate of soda, which is often used in applications where purity is critical, such as in the production of detergents or food additives. Second, the enclosed pipeline system minimizes dust emissions and environmental impact, aligning with modern industrial standards for safety and sustainability. Third, the flexibility of the system allows for easy integration into existing production lines, enabling seamless material transfer between processing stages. Additionally, air-driven systems offer high throughput rates, making them suitable for high-volume operations where continuous material flow is essential. These characteristics make air-driven sulfate of soda handling a preferred choice in industries where efficiency, safety, and material integrity are paramount.
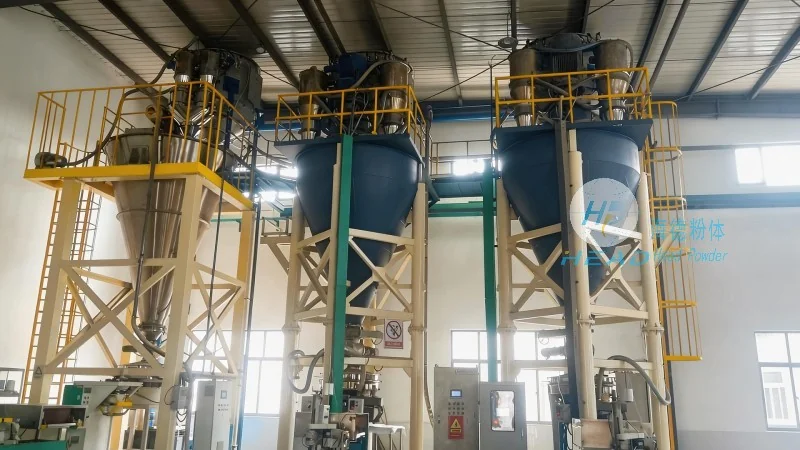
For industries processing sulfate of soda, air-driven material handling systems provide a robust and efficient solution that addresses the unique challenges of material transport. By leveraging the principles of pneumatic conveying and incorporating advanced design features, these systems ensure reliable operation while minimizing downtime and maintenance costs. Shandong HeadPowder Engineering Co., Ltd. continues to lead in the development of customized air-driven solutions for sulfate of soda handling, helping businesses achieve optimal performance and compliance in their operations. With a strong commitment to quality and innovation, the company remains a trusted partner for industries seeking to enhance their material handling capabilities and improve overall process efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top