With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, officially known as Shandong HeadPowder Engineering Co., Ltd., is a professional enterprise based in Shandong, China, specializing in the design, manufacturing, and installation of material handling systems. The company focuses on providing efficient and reliable solutions for limestone and other bulk material transport applications.
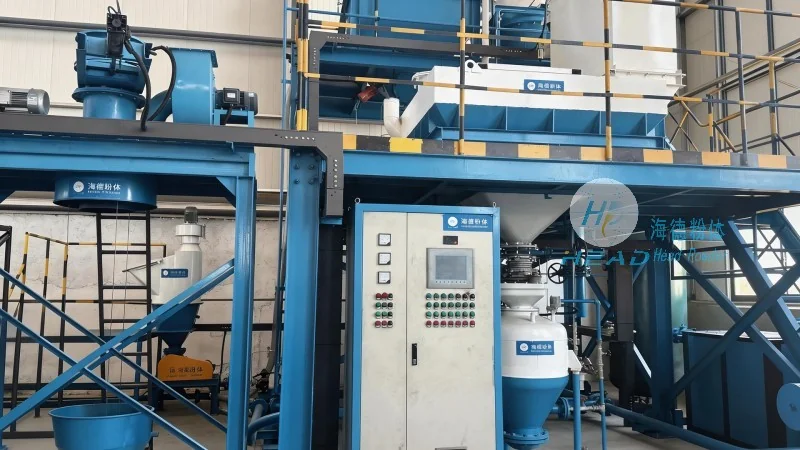
Limestone material transport primarily involves the movement of bulk limestone from storage or production sites to processing facilities or end-use locations. The core principles revolve around the selection of appropriate conveying equipment, such as belt conveyors, screw conveyors, or pneumatic systems, based on factors like material characteristics, distance, and throughput requirements. Key principles include ensuring proper material flow, minimizing friction and wear, and maintaining consistent speed to optimize efficiency and reduce operational costs. The system design considers the physical properties of limestone, including its density, particle size, and abrasiveness, to select suitable components and configurations that enhance durability and performance.
The working scene characteristics of limestone material transport vary widely depending on the specific application and industrial environment. For example, in mining operations, the transport systems must handle large volumes of raw limestone from open-pit or underground mines, often over long distances with steep inclines. The equipment used in such scenarios typically includes heavy-duty belt conveyors with reinforced structures and robust drive systems to withstand harsh conditions and heavy loads. In cement production plants, limestone is transported from stockpiles to crushers and grinding mills, requiring precise control of flow rates and alignment to ensure smooth processing. Additionally, in construction material supply chains, limestone is transported from quarries to construction sites, where the systems may need to adapt to varying terrain and weather conditions. The characteristics also include the need for dust control measures, as limestone is a fine-grained material that can generate significant airborne particles during handling. Proper sealing and filtration systems are integrated into the transport equipment to maintain air quality and comply with environmental regulations. Furthermore, the working scenes may involve integration with other industrial processes, such as blending with other raw materials or packaging, requiring the transport system to be compatible with downstream equipment and processes.
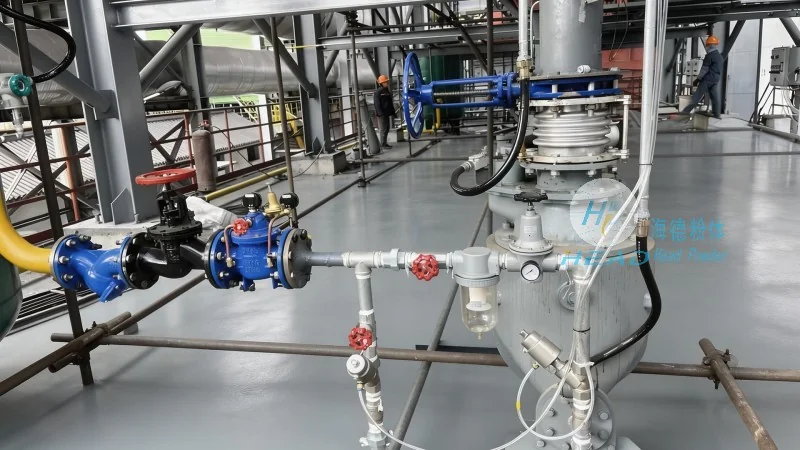
The effectiveness of limestone material transport systems depends heavily on the integration of various components and the adaptability to different operational needs. HeadPowder’s solutions often incorporate advanced control systems, such as PLC (Programmable Logic Controller) and SCADA (Supervisory Control and Data Acquisition), to monitor and adjust the transport process in real-time. This integration allows for dynamic adjustments to flow rates, speed, and pressure, ensuring optimal performance under varying conditions. The equipment selection also considers the compatibility with existing infrastructure, minimizing the need for extensive modifications and reducing installation time and costs. For instance, in retrofitting existing mining sites, the company may adapt existing conveyors with upgraded components or add supplementary systems to enhance capacity. Additionally, the systems are designed with modular components, enabling easy maintenance and replacement of parts without disrupting the entire operation. This modularity enhances the long-term reliability and reduces downtime, which is critical for continuous production in limestone processing industries.
Operational efficiency is a key focus in limestone material transport, as it directly impacts production output and cost management. The principles of energy conservation and reduced downtime are central to the design and operation of these systems. HeadPowder’s conveyors are engineered with energy-efficient motors and variable speed drives, allowing for adjustments based on the load and distance, thus minimizing energy consumption. Regular maintenance is also a critical aspect of maintaining efficiency, and the company provides comprehensive maintenance services, including preventive maintenance schedules, on-site inspections, and spare parts availability. The use of durable materials, such as high-strength steel and wear-resistant coatings, in the construction of conveyor components extends the lifespan of the equipment and reduces the frequency of replacements. Additionally, the integration of monitoring systems helps in early detection of potential issues, such as belt wear or motor overheating, allowing for timely interventions and preventing costly breakdowns. This proactive approach to maintenance ensures that the transport systems operate at peak performance, supporting the overall productivity of limestone processing facilities.
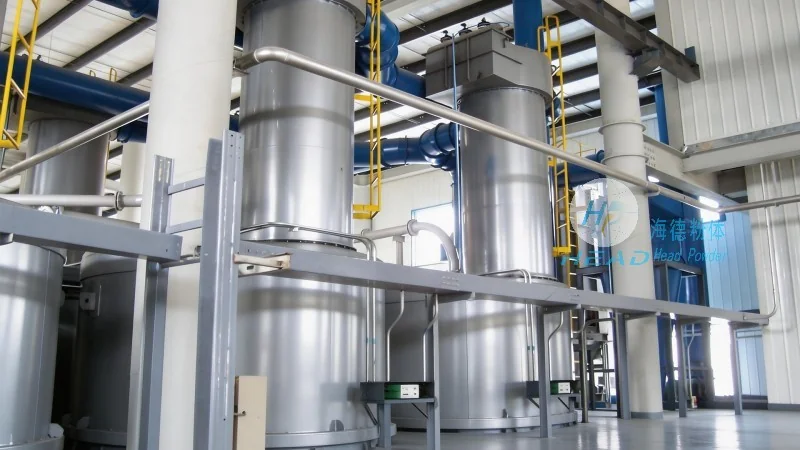
Environmental considerations play a significant role in modern limestone material transport, especially in light of increasing regulatory requirements and sustainability goals. The systems are designed to minimize environmental impact through various measures, such as dust suppression and noise reduction. Dust control is achieved through the use of enclosed conveyor systems, dust collection hoods, and wet scrubbing systems, which capture and neutralize airborne particles before they are released into the environment. This not only improves air quality but also helps in maintaining compliance with environmental regulations. Noise reduction is addressed by using soundproof enclosures and low-noise components, particularly in systems located near residential or sensitive areas. Additionally, the energy-efficient design of the equipment contributes to lower carbon emissions, aligning with the industry’s push towards sustainable practices. The company also emphasizes the use of recyclable materials in the construction of components and the implementation of waste management strategies to minimize the environmental footprint of the transport operations. These measures reflect the commitment of HeadPowder to provide not only efficient but also environmentally responsible limestone material transport solutions.
HeadPowder recognizes that each limestone material transport project has unique requirements, and thus, the company offers customized solutions tailored to specific needs. The customization process begins with a thorough analysis of the client’s operational conditions, including the type and volume of limestone, the distance and elevation changes, and the integration with existing processes. Based on this analysis, the company designs and manufactures equipment that meets the exact specifications, ensuring optimal performance and compatibility. For example, in mining operations, the company may design a multi-stage conveyor system with incline and decline sections to handle the terrain effectively. In cement plants, the system may include feeding mechanisms that precisely control the flow of limestone into crushers and grinding mills. The flexibility of the systems also allows for integration with other bulk materials, such as clay or sand, in mixed processing applications. This adaptability makes the HeadPowder solutions suitable for a wide range of limestone transport scenarios, from small-scale quarry operations to large-scale industrial plants. The company’s expertise in material handling and its commitment to customer satisfaction ensure that each customized solution is tailored to meet the specific challenges and opportunities of the client’s operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top