With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
When it comes to handling and transporting bulk powders in industrial settings, the choice of equipment is critical for efficiency, safety, and product integrity. Among the various solutions available, the purified powder bulk material conveyor stands out as a specialized system designed to meet the stringent requirements of industries dealing with sensitive or high-purity materials. This article aims to explore what these conveyors are and delve into their fundamental design principles, providing a comprehensive understanding for professionals in the field. Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in this domain, specializes in developing and supplying such advanced equipment to meet the diverse needs of modern industries.
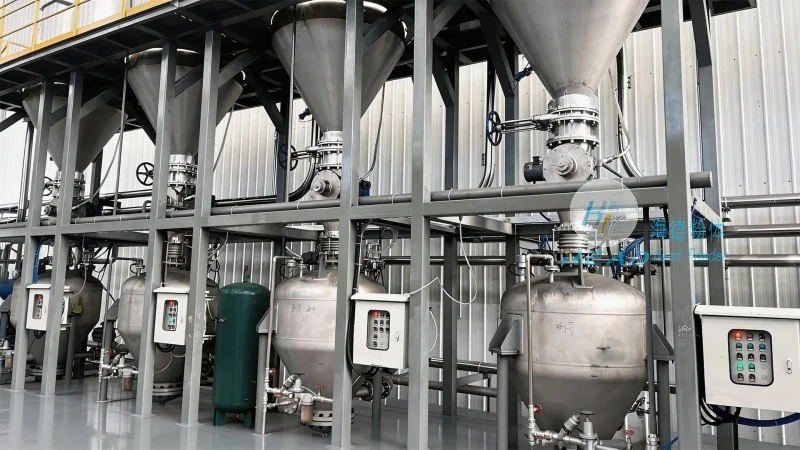
A purified powder bulk material conveyor is a specialized piece of industrial equipment engineered to transport dry powders and granules while maintaining a high level of purity and preventing contamination. These systems are commonly used in sectors such as pharmaceuticals, food processing, chemical manufacturing, and electronics, where even minor impurities can have significant impacts on product quality and safety. The primary goal of such conveyors is to ensure that the material being transported remains uncontaminated throughout the process, from the source to the destination.
The design of a purified powder bulk material conveyor incorporates several key components that work in harmony to achieve its objectives. These typically include a hopper or feeder for material storage and controlled discharge, a conveyor mechanism (such as a screw, belt, or pneumatic system) that moves the material, and a series of seals, filters, and cleaning mechanisms to prevent dust and contaminants from entering or exiting the system. The materials used in the construction of these conveyors are often chosen for their non-reactive properties, such as stainless steel or specialized plastics, to avoid any interaction with the conveyed powders.
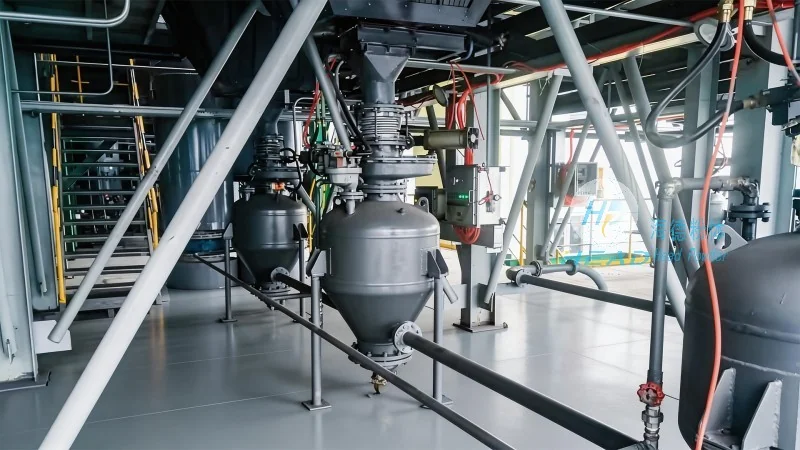
A critical aspect of the design is the incorporation of an efficient airflow system combined with filtration. Many purified powder conveyors utilize a closed-loop or positive pressure system to maintain a controlled environment. This system ensures that the material is transported within a sealed chamber, preventing exposure to ambient air and external contaminants. The air used in the system is typically filtered through high-efficiency particulate air (HEPA) or similar filters to remove any particles that could compromise the purity of the powder. Additionally, the conveyor may include features like dust collection hoods and automatic cleaning cycles to maintain the integrity of the filtration system over time.
Modern purified powder bulk material conveyors are often equipped with advanced control systems that allow for precise regulation of the conveying process. These systems may include variable speed drives, level sensors, and pressure monitoring to ensure that the material is transported at the optimal rate and under the correct conditions. Automation plays a vital role in maintaining consistency and reducing the risk of human error, which is particularly important in industries where product quality is paramount. The control panels are typically designed to be user-friendly, allowing operators to easily adjust settings and monitor the system's performance in real-time.
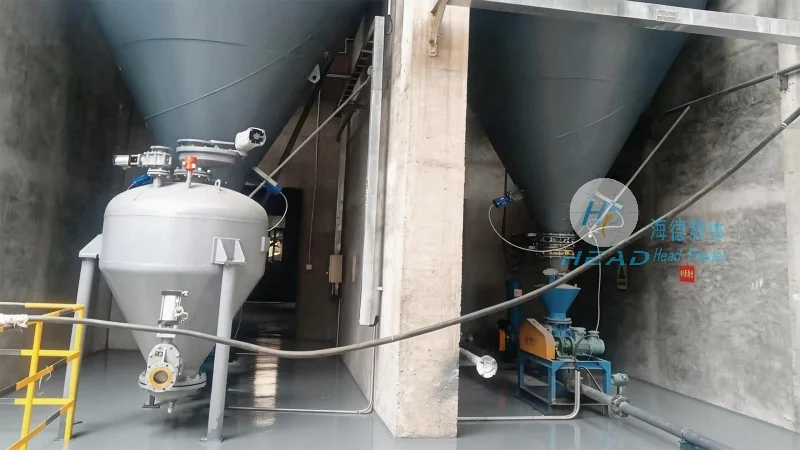
The use of purified powder bulk material conveyors offers numerous benefits across various industries. In pharmaceutical manufacturing, for example, these systems help maintain the sterility and purity of active pharmaceutical ingredients (APIs), ensuring compliance with stringent regulatory standards. In the food industry, they prevent cross-contamination and maintain the quality of food powders, which is essential for consumer safety and brand reputation. Similarly, in chemical and electronics manufacturing, they help preserve the integrity of sensitive materials, reducing the risk of product defects and costly rework.
In summary, a purified powder bulk material conveyor is a sophisticated and essential piece of equipment for industries that require the safe and efficient transport of high-purity powders. Its design, incorporating components like sealed conveyors, advanced filtration, and automated control systems, ensures that the material remains uncontaminated throughout the process. By understanding the design principles and benefits of these systems, businesses can make informed decisions about their material handling solutions, ultimately enhancing operational efficiency and product quality.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top