With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Understanding the NCA Powder Pneumatic Conveying System and Its Design Principles
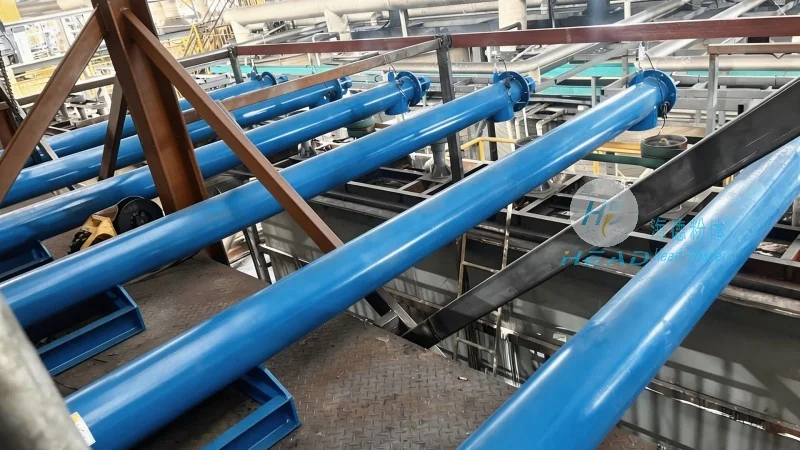
For industries dealing with Nickel Cobalt Aluminum Lithium (NCA) powders, efficient and reliable material handling is crucial. The NCA powder pneumatic conveying system is a specialized piece of equipment designed to transport these fine powders through a system of pipes using air or other gases. This technology offers a clean, dust-free, and flexible solution for moving NCA powders from one location to another, making it an essential component in battery manufacturing and other high-tech applications.
HeadPowder, a leading provider of pneumatic conveying systems, specializes in designing and manufacturing equipment tailored to the unique needs of NCA powder handling. With years of experience in the industry, HeadPowder has developed a reputation for delivering high-quality, durable, and efficient solutions that meet the stringent requirements of modern battery production. The company’s headquarters is located in Shandong, China, where it combines advanced engineering with local manufacturing expertise to serve global clients.
The design of an NCA powder pneumatic conveying system is based on several key principles to ensure optimal performance and safety. First, the system must be capable of handling the specific properties of NCA powders, such as their particle size, density, and flowability. This often involves using specialized materials for the conveying lines and components to prevent corrosion or contamination, as NCA powders are sensitive to moisture and other environmental factors.
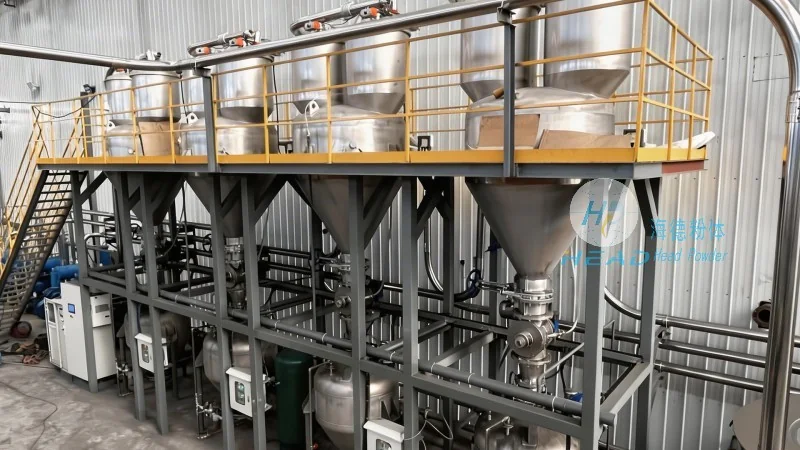
Second, the system’s design focuses on maintaining a consistent flow rate and pressure to prevent blockages or uneven distribution of the powder. This is achieved through the use of positive displacement blowers or rotary air locks, which provide a steady supply of air while controlling the flow of the powder. The system also incorporates features like pulse-jet cleaning and air filtration to ensure that the conveying lines remain clear and that the air is clean, preventing dust accumulation and maintaining product quality.
Third, safety is a critical consideration in the design of NCA powder pneumatic conveying systems. The equipment is designed with explosion-proof components and proper ventilation to mitigate the risks associated with handling flammable or reactive powders. Additionally, the system includes monitoring and control features to detect any issues, such as pressure drops or abnormal flow, and alert operators to take corrective action.
An NCA powder pneumatic conveying system typically consists of several key components, each playing a vital role in the overall operation. The main components include the hopper, which holds the NCA powder and feeds it into the system; the conveying line, which transports the powder through the pipes; the air supply system, which provides the necessary air or gas to move the powder; and the receiver, which collects the powder at the destination.
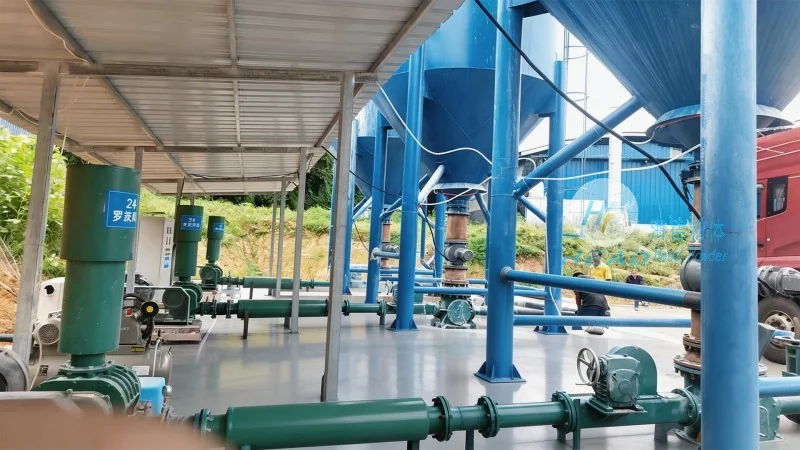
The hopper is designed with a sloped bottom and a discharge valve to ensure smooth and consistent feeding of the powder. It may also include a vibratory feeder to prevent bridging or caking, which can occur with NCA powders due to their fine particle size. The conveying line is usually made of stainless steel or other corrosion-resistant materials to prevent contamination and ensure durability. The air supply system typically uses a positive displacement blower, which provides a high-pressure, low-volume air flow that is ideal for transporting fine powders.
The receiver is a container that collects the NCA powder at the end of the conveying line. It is designed with a vent and a discharge valve to allow for easy emptying and cleaning. The system may also include additional components, such as a filter or a cyclone separator, to remove any fine particles from the air before it is released into the environment, ensuring compliance with environmental regulations.
Implementing an NCA powder pneumatic conveying system offers several benefits for businesses in the battery and related industries. First, it provides a clean and dust-free environment, which is essential for maintaining product quality and preventing contamination. Unlike traditional bulk handling methods, such as bucket elevators or screw conveyors, pneumatic conveying systems do not generate dust, reducing the risk of product degradation and improving workplace safety.
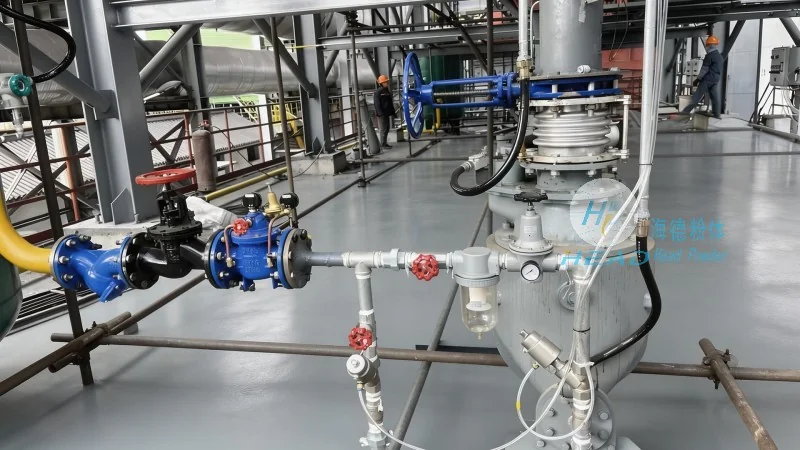
Second, the system offers high efficiency and flexibility. It can transport NCA powders over long distances and through complex layouts, making it suitable for large-scale production facilities. The system can also be easily adjusted to handle different powder types or flow rates, providing versatility for changing production needs.
Third, the system is relatively low maintenance compared to other material handling equipment. The use of positive displacement blowers and rotary air locks reduces the need for frequent repairs, and the design of the conveying lines minimizes the risk of blockages. This results in lower operational costs and increased uptime for the equipment.
The NCA powder pneumatic conveying system is a critical piece of equipment for industries dealing with Nickel Cobalt Aluminum Lithium powders. Its design, based on specialized principles and components, ensures efficient, safe, and reliable transport of these fine powders. With the expertise of companies like HeadPowder, businesses can implement high-quality pneumatic conveying systems that meet their specific needs and contribute to their overall success in the battery manufacturing sector.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top