With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading engineering company based in Shandong, China, specializes in advanced material handling solutions. The company's expertise lies in the development and implementation of efficient pneumatic conveying systems, particularly for sodium nitrate, a critical chemical widely used in various industries. This article explores the fundamental principles, practical applications, and emerging trends in sodium nitrate pneumatic conveying technology, highlighting the technical advancements and operational benefits that define modern material transport solutions.
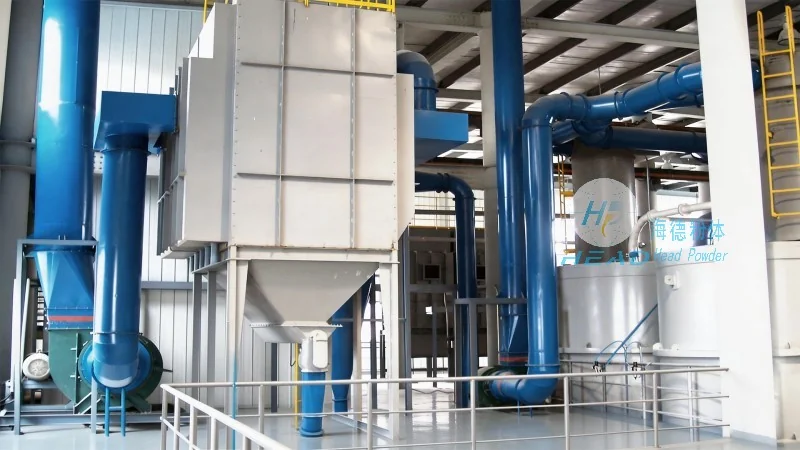
Pneumatic conveying, also known as air conveying, is a method of transporting bulk materials through a pipeline using a stream of pressurized or vacuum air. In the context of sodium nitrate, this technology leverages the principles of fluid dynamics to move the solid material efficiently. The process typically involves a conveying line where air is introduced at a controlled pressure, creating a flow that entrains the sodium nitrate particles. Key components of the system include a feed hopper, a rotary airlock valve, a conveying pipe, and a receiver. The air velocity is carefully managed to ensure that the sodium nitrate particles are suspended and transported without excessive wear or degradation. The choice between positive pressure and negative pressure systems depends on the specific application, with positive pressure being more common for long-distance or high-capacity transport due to its ability to maintain consistent air flow and prevent material buildup in the line.
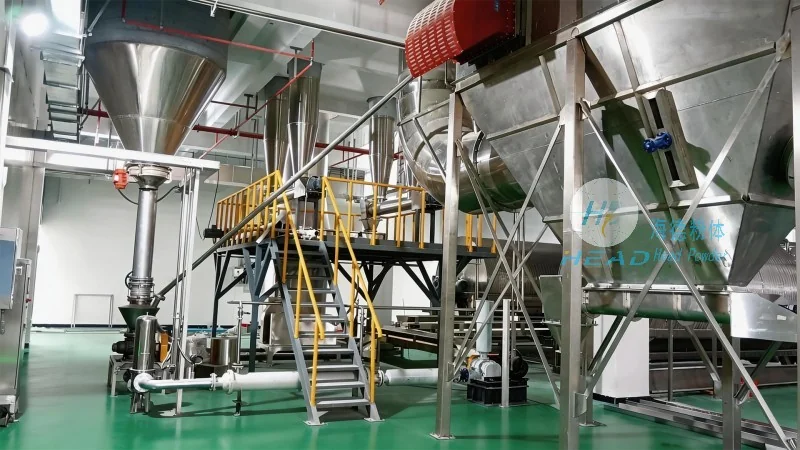
The application of sodium nitrate pneumatic conveying technology spans multiple sectors, including chemical manufacturing, agricultural fertilizer production, and industrial processing. In chemical plants, this system is utilized to transfer sodium nitrate from storage silos to processing units, ensuring a continuous and controlled supply of raw material. The efficiency of the system minimizes downtime and reduces the risk of material spillage, which is crucial for maintaining operational safety and compliance with environmental regulations. In the agricultural sector, sodium nitrate is a key component in fertilizer blends, and pneumatic conveying enables precise and hygienic handling of the material during production and packaging. The technology also finds use in industrial applications where sodium nitrate is used as a oxidizer or in the production of other chemical compounds. HeadPowder's systems are designed to meet the specific requirements of each application, ensuring optimal performance and reliability. For instance, in fertilizer production lines, the system can handle large volumes of sodium nitrate at high speeds, facilitating seamless integration with downstream processing equipment. The versatility of pneumatic conveying makes it an ideal solution for industries that require consistent and high-quality material transport.
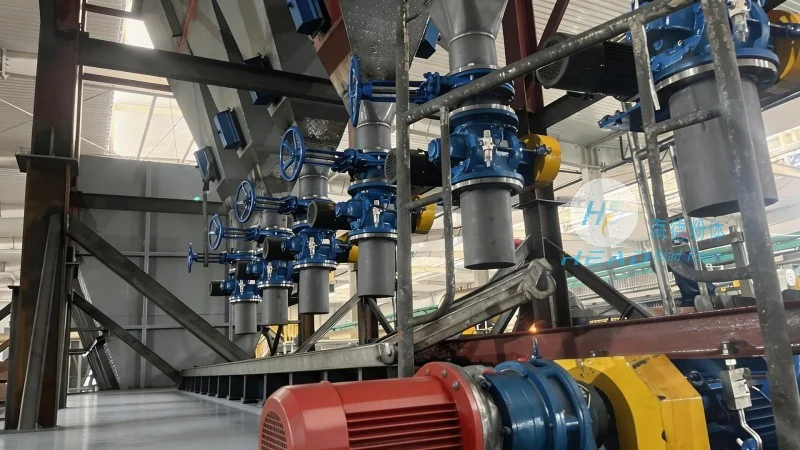
As technology advances, the sodium nitrate pneumatic conveying industry is witnessing several key developments aimed at enhancing efficiency, reducing costs, and improving sustainability. One significant trend is the adoption of advanced control systems that optimize air pressure and flow rates in real-time. These systems use sensors and automation to adjust the conveying parameters based on the material characteristics and system conditions, leading to energy savings and reduced operational costs. Another trend is the integration of materials with improved wear resistance, such as high-density polyethylene or specialized coatings, to extend the lifespan of conveying components. This reduces maintenance frequency and lowers long-term operational expenses. Additionally, there is a growing focus on environmental considerations, with companies like HeadPowder developing systems that minimize air emissions and noise pollution. The use of energy-efficient motors and variable frequency drives (VFDs) further contributes to the sustainability of the process. Furthermore, research is ongoing to develop more compact and flexible conveying systems that can adapt to changing production needs, such as modular designs that allow for easy expansion or reconfiguration. These advancements are driven by the need for higher productivity and lower environmental impact in modern industrial operations. The future of sodium nitrate pneumatic conveying technology is likely to involve more intelligent and automated solutions that leverage data analytics and artificial intelligence to predict maintenance needs and optimize system performance. As industries continue to seek more efficient and sustainable material handling solutions, the development of advanced pneumatic conveying systems will remain a critical area of focus.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top