

How to Choose the Right Edible Salt Pneumatic Conveying Manufacturer? What Factors to Consider?
When it comes to selecting a manufacturer for edible salt pneumatic conveying systems, businesses in the food processing industry face a critical decision. The choice of manufacturer directly impacts the efficiency, safety, and overall performance of the conveying process. This article aims to guide you through the essential factors to consider when evaluating potential manufacturers, with a focus on the expertise and capabilities of Shandong HeadPowder Engineering Co., Ltd., a leading provider in this field.
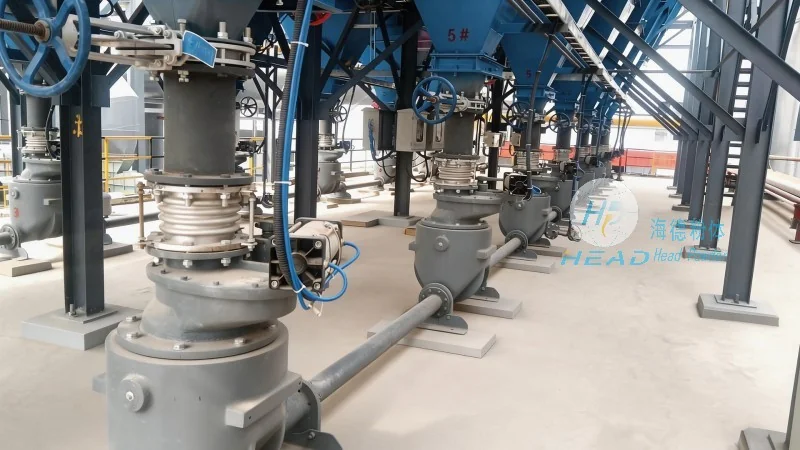
Understanding the Importance of Edible Salt Pneumatic Conveying Systems
Edible salt, a staple in food production, requires specialized handling to maintain its quality and purity. Pneumatic conveying systems offer a hygienic and efficient method for transporting bulk materials like edible salt, ensuring minimal contamination and product integrity. The right manufacturer understands these unique requirements and designs systems that meet stringent industry standards.
Key Factors to Consider When Choosing a Manufacturer
Choosing the right manufacturer involves evaluating several critical aspects to ensure the system meets your operational needs. Here are the key factors to consider:
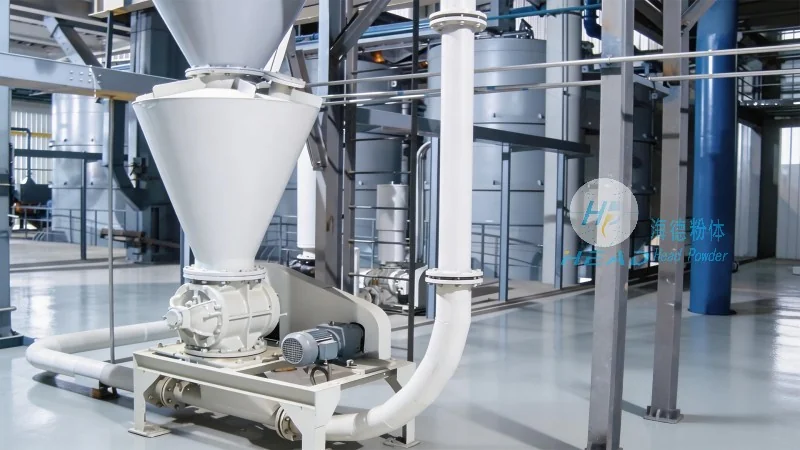
1. **Technical Expertise and Experience**: A reputable manufacturer should have extensive experience in designing and manufacturing pneumatic conveying systems for the food industry. They should possess in-depth knowledge of material properties, flow dynamics, and the specific challenges associated with handling edible salt. Shandong HeadPowder Engineering Co., Ltd. brings decades of experience in engineering solutions tailored to the food processing sector.
2. **Compliance with Industry Standards**: The food industry is governed by strict regulations regarding hygiene, safety, and material handling. The manufacturer must ensure that their systems comply with relevant standards such as FDA, HACCP, and local regulations. This includes using food-grade materials, easy-to-clean components, and robust design to prevent cross-contamination. HeadPowder specializes in creating systems that adhere to these standards, providing peace of mind for food manufacturers.
3. **Customization and Scalability**: Every food processing facility has unique requirements. The manufacturer should offer customized solutions that can be scaled to meet current and future production needs. Whether you need a small-scale system for a pilot plant or a large-scale system for a full production line, the manufacturer should be able to adapt their designs to your specific workflow. Shandong HeadPowder Engineering Co., Ltd. works closely with clients to understand their operational needs and develop tailored solutions that enhance productivity.
4. **Reliability and After-Sales Support**: The longevity and reliability of the conveying system depend on the manufacturer's commitment to quality and support. Look for a company that provides comprehensive after-sales services, including maintenance, troubleshooting, and spare parts availability. A reliable manufacturer will also offer technical support to address any issues promptly, minimizing downtime and ensuring smooth operations. HeadPowder provides ongoing support to its clients, ensuring that their systems operate at peak efficiency throughout their lifecycle.
5. **Cost-Effectiveness and ROI**: While quality and performance are paramount, the overall cost of the system is also a critical factor. The manufacturer should offer competitive pricing without compromising on quality. Additionally, consider the return on investment (ROI) by evaluating how the system can improve operational efficiency, reduce labor costs, and enhance product quality. A well-designed system from a reputable manufacturer like HeadPowder can lead to long-term cost savings and increased profitability.
Why Choose Shandong HeadPowder Engineering Co., Ltd.?
With its headquarters in Shandong, China, Shandong HeadPowder Engineering Co., Ltd. stands out as a trusted partner for edible salt pneumatic conveying solutions. The company combines advanced engineering capabilities with a deep understanding of the food industry's needs, delivering systems that are both efficient and compliant with industry standards.
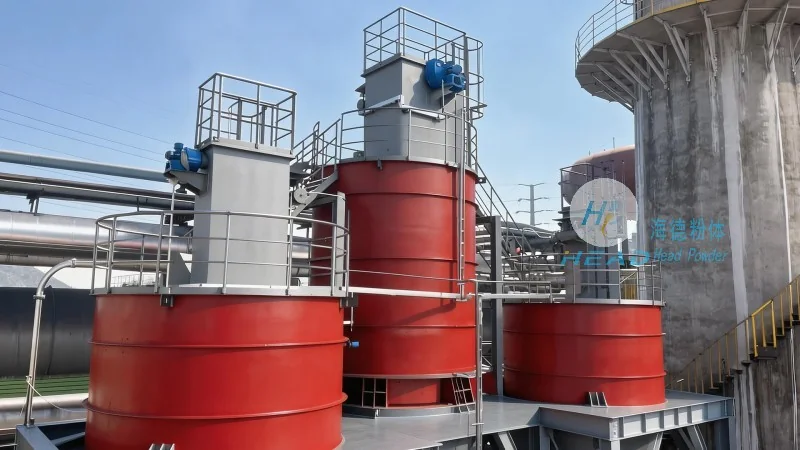
HeadPowder's team of experienced engineers designs customized pneumatic conveying systems tailored to the unique requirements of edible salt handling. The company uses high-quality, food-grade materials and advanced technology to ensure that the systems are hygienic, durable, and easy to maintain. Whether you are a small-scale food processor or a large-scale manufacturer, HeadPowder offers scalable solutions that can adapt to your growing needs.
The company's commitment to customer satisfaction is evident in its comprehensive after-sales support. From installation and commissioning to ongoing maintenance and technical assistance, HeadPowder ensures that its clients receive the support they need to maximize the performance of their conveying systems. By choosing HeadPowder, businesses can enhance their operational efficiency, maintain product quality, and comply with regulatory requirements.