With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Efficient and reliable transportation of wheat is a critical aspect of the agricultural and food processing industries. Pneumatic conveying systems have emerged as a preferred solution for handling wheat due to their ability to transport bulk materials with minimal dust, reduced labor costs, and enhanced safety. This article explores the different types of pneumatic conveying systems commonly used in wheat transportation and their practical applications, highlighting the technological advancements and operational benefits they offer.
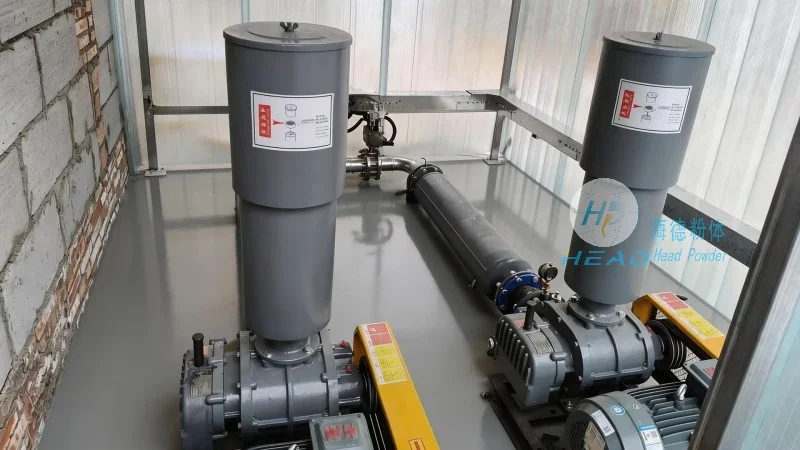
Pneumatic conveying systems utilize air or gas to transport solid materials like wheat from one location to another. Unlike traditional methods such as belt conveyors or bucket elevators, pneumatic systems can handle fine powders and granules with precision, making them ideal for wheat processing facilities. The choice of system depends on factors like the distance of transport, the volume of material, and the required speed of operation. Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in this field, specializes in designing and manufacturing customized pneumatic conveying solutions tailored to the specific needs of wheat handling operations.
There are primarily two types of pneumatic conveying systems used in wheat transportation: suction (or negative pressure) systems and pressure (or positive pressure) systems. Each type has distinct characteristics and is suitable for different scenarios.
Suction systems operate by creating a negative pressure in the conveying line, drawing the wheat from the source and transporting it to the destination. These systems are commonly used for short to medium distances and are particularly effective when the wheat is to be moved from a storage bin or silo to a processing unit. The primary advantage of suction systems is their ability to handle large volumes of material with relatively low air velocity, which helps in reducing wear and tear on the system components. Shandong HeadPowder Engineering Co., Ltd. offers advanced suction systems equipped with high-efficiency filters and adjustable air flow controls to ensure optimal performance and minimal dust emissions.
Pressure systems, on the other hand, operate by forcing air or gas through the conveying line under positive pressure, pushing the wheat from the source to the destination. These systems are ideal for longer distances and can handle higher material loads compared to suction systems. They are commonly used in large-scale wheat processing plants where the material needs to be transported over several hundred meters. The key benefits of pressure systems include higher conveying speeds, reduced energy consumption per unit of material, and the ability to handle more abrasive materials without significant degradation. Shandong HeadPowder Engineering Co., Ltd. provides pressure systems with robust construction and advanced control mechanisms to ensure consistent and reliable operation.
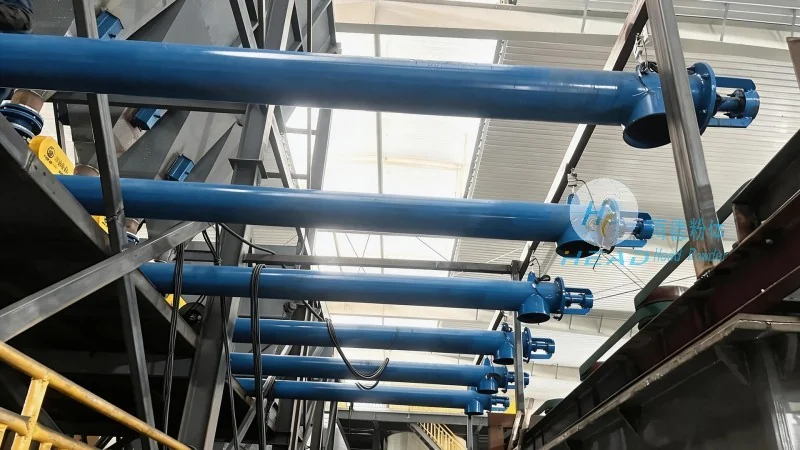
Pneumatic conveying systems find widespread application in various stages of wheat processing, from storage and handling to milling and packaging. Here are some key practical applications:
In modern wheat storage facilities, pneumatic conveying systems are used to transfer wheat from large storage silos to processing units such as flour mills or cleaning stations. The suction type of system is often preferred for this application as it can efficiently draw wheat from the silo and transport it to the processing line without the need for complex infrastructure. Shandong HeadPowder Engineering Co., Ltd. has developed specialized suction systems with large-diameter conveying lines and high-capacity air fans to handle the high volume of wheat in silos, ensuring smooth and continuous operation.
Before processing, wheat often requires cleaning to remove impurities such as dust, stones, and foreign materials. Pneumatic conveying systems can be integrated with cleaning equipment to transport the cleaned wheat to the next stage of processing. The pressure system is particularly useful here as it can handle the material at higher speeds, allowing for efficient separation of impurities. Shandong HeadPowder Engineering Co., Ltd. offers conveying systems that are compatible with various cleaning technologies, ensuring that the wheat is cleaned effectively while maintaining the integrity of the material.
During the flour milling process, pneumatic conveying systems are used to transport the ground wheat products, such as flour and bran, from the milling units to storage silos or packaging lines. The pressure system is commonly used for this application due to its ability to handle fine powders over longer distances. Shandong HeadPowder Engineering Co., Ltd. provides pressure conveying systems with fine filters and adjustable air flow to prevent the accumulation of dust and ensure the quality of the final products.
Compared to traditional conveying methods, pneumatic conveying systems offer several advantages that make them the preferred choice for wheat transportation:
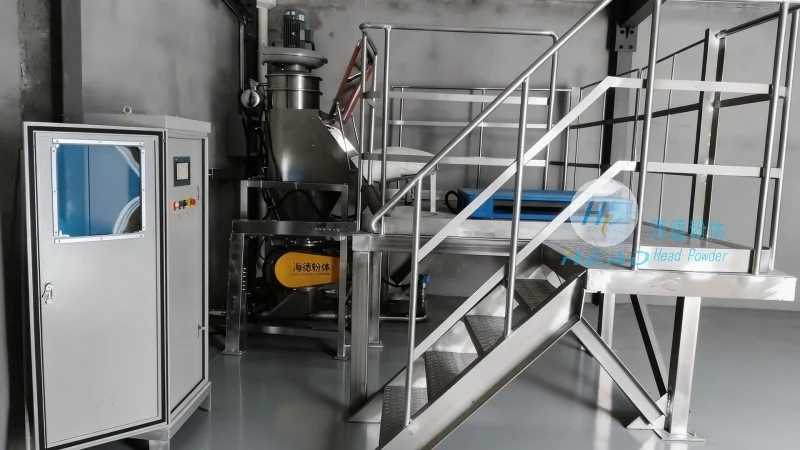
Pneumatic systems are enclosed, which helps in containing dust and preventing it from spreading into the environment. This not only improves workplace safety but also reduces the risk of fire hazards associated with dust accumulation. Shandong HeadPowder Engineering Co., Ltd. incorporates advanced dust control features in their systems, such as high-efficiency particulate air (HEPA) filters, to ensure compliance with environmental and safety regulations.
Automated pneumatic conveying systems reduce the need for manual handling of wheat, thereby lowering labor costs and increasing operational efficiency. The systems can operate continuously without the need for frequent maintenance, as they are designed with durable components that can withstand the abrasive nature of wheat particles. Shandong HeadPowder Engineering Co., Ltd. provides maintenance-friendly designs and easy-to-access components to minimize downtime and maximize productivity.
Pneumatic conveying systems can be customized to suit the specific requirements of wheat handling operations. Whether it's a small-scale farm or a large industrial mill, Shandong HeadPowder Engineering Co., Ltd. offers flexible solutions that can be scaled up or down as per the needs of the client. The systems can be integrated with other processing equipment, such as cleaning, drying, or packaging machines, to create a seamless workflow.
Pneumatic conveying systems play a vital role in the efficient and safe transportation of wheat in modern agricultural and food processing industries. With their ability to handle bulk materials with minimal dust and reduced labor costs, these systems have become indispensable in wheat handling operations. Shandong HeadPowder Engineering Co., Ltd., with its expertise in designing and manufacturing customized pneumatic conveying solutions, continues to provide reliable and efficient systems that meet the evolving needs of the wheat industry. By leveraging advanced technology and robust construction, these systems ensure optimal performance and contribute to the overall productivity and profitability of wheat processing facilities.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top