With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Aggregate powder conveying systems are critical components in various industrial applications, designed to efficiently transport bulk materials such as aggregates, powders, and granules. These systems play a vital role in sectors like construction, mining, and manufacturing, ensuring smooth material handling and process continuity. The design and functionality of these systems are tailored to meet the specific demands of different industries, offering reliable and efficient solutions for material transport needs.
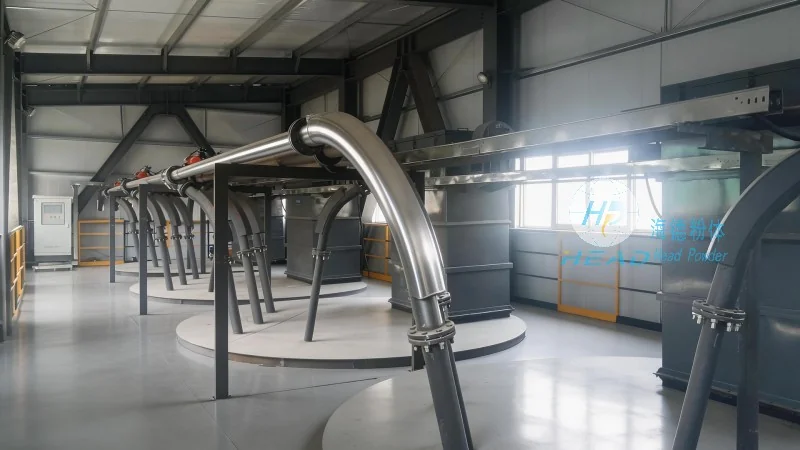
The core structure of an aggregate powder conveying system typically includes several essential components that work in harmony to achieve effective material transport. These components include the hopper for material storage, the conveyor mechanism (such as screw conveyors, belt conveyors, or pneumatic systems), and control systems for operation. Each component is engineered to handle the specific characteristics of the aggregate powder, such as particle size, density, and moisture content, ensuring optimal performance and minimal material degradation.
The operational principle of an aggregate powder conveying system involves the intake of material from the hopper, followed by the transport through the conveyor mechanism. For example, in a screw conveyor system, the material is fed into the hopper and then moved along the screw shaft by rotational motion. The screw design, including pitch and diameter, is optimized to handle the specific aggregate characteristics, ensuring consistent flow and preventing blockages. In pneumatic conveying systems, compressed air is used to transport the powder through a pipeline, where the air velocity and pressure are carefully controlled to maintain material transport efficiency.
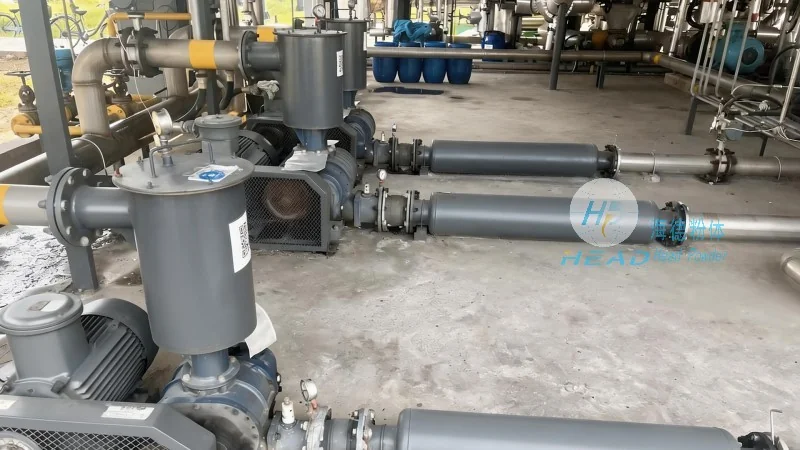
Implementing an aggregate powder conveying system offers numerous advantages for industrial operations. These systems enhance productivity by reducing manual handling and labor costs, while also improving material handling efficiency and accuracy. The automated nature of these systems minimizes human error and ensures consistent material flow, which is crucial for maintaining production quality. Additionally, the design of these systems allows for easy integration into existing production lines, providing flexibility and adaptability to changing operational needs.
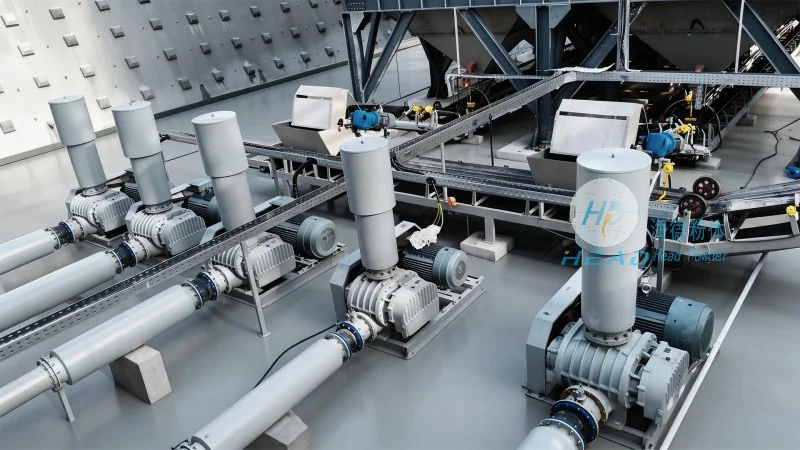
Aggregate powder conveying systems are widely used in various industrial applications. In the construction industry, these systems are essential for transporting aggregates and cement to mixing plants, ensuring a steady supply of materials for concrete production. In mining operations, they facilitate the transport of ore and powder from processing plants to storage or further processing facilities. The versatility of these systems also makes them suitable for pharmaceutical and chemical industries, where precise material handling is critical to maintain product quality and safety.
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized aggregate powder conveying systems to meet the unique requirements of different clients. The company offers a range of solutions, from standard conveyor systems to advanced pneumatic and screw conveyor configurations, tailored to handle various aggregate types and processing capacities. With a focus on quality and reliability, HeadPowder provides comprehensive support, including system design, installation, and maintenance services, ensuring that clients receive a solution that aligns with their operational goals.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top