With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industries dealing with bulk powder handling, efficient and reliable material transport is crucial. The vacuum dilute phase powder conveying system, developed by Shandong HeadPowder Engineering Co., Ltd. (commonly known as HeadPowder), offers a sophisticated solution that ensures safe and effective movement of powders over long distances. This article provides an overview of the system's structure and operational principles, highlighting its key components and how they work together to deliver optimal performance.
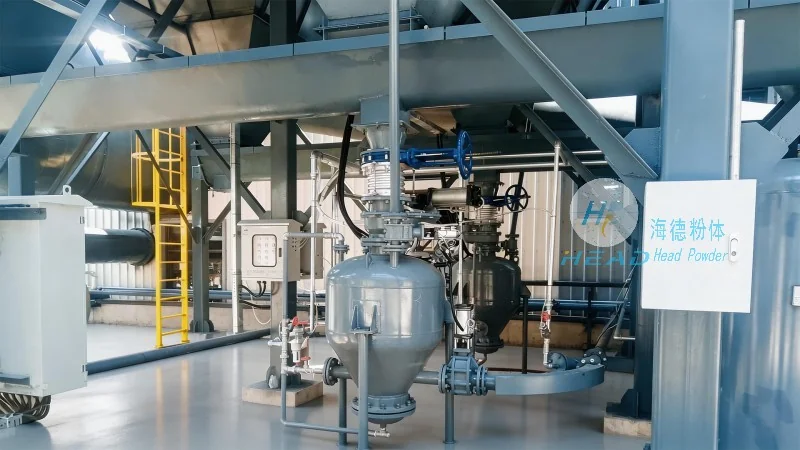
The vacuum dilute phase powder conveying system is composed of several critical components that work in tandem to achieve efficient material transport. The main elements include the vacuum pump, conveying pipeline, material feed hopper, and control system. Each component plays a vital role in the overall operation of the system.
The vacuum pump is the heart of the system, responsible for creating the negative pressure environment necessary for conveying the powder. It draws air and powder particles from the feed hopper and transports them through the pipeline. The pump's design and capacity are tailored to match the specific requirements of the application, ensuring consistent performance under various operating conditions.
The conveying pipeline is typically made of durable materials such as stainless steel or plastic, designed to withstand the pressure and temperature variations encountered during operation. The pipeline is equipped with bends, elbows, and other fittings that allow for the smooth routing of the material flow. The design of the pipeline is optimized to minimize pressure drop and maximize conveying efficiency.
The material feed hopper is where the bulk powder is loaded. It is equipped with a feeder mechanism, such as a rotary valve or a screw feeder, that controls the flow rate of the material into the pipeline. The hopper is designed to prevent material bridging and ensure a consistent feed, which is essential for maintaining the system's performance and preventing blockages.
The control system monitors and regulates the operation of the vacuum pump and feeder, ensuring that the system operates within safe and efficient parameters. It includes sensors for pressure, flow rate, and temperature, which provide real-time data to the operator. The control system also allows for adjustments to be made on the fly, enabling the system to adapt to changing conditions and maintain optimal performance.
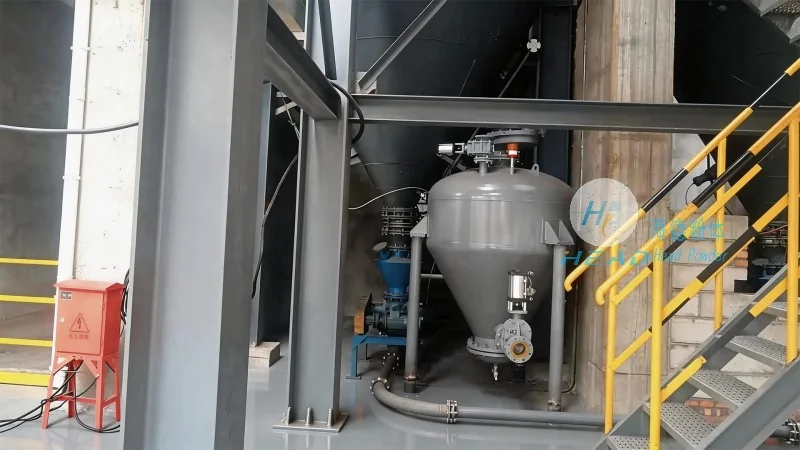
The operation of the vacuum dilute phase powder conveying system is based on the principle of negative pressure. The vacuum pump creates a low-pressure zone in the pipeline, which draws the powder particles from the feed hopper and transports them through the pipeline to the discharge point. The powder is carried in a dilute phase, meaning that the particles are suspended in the air and do not form a dense stream.
As the powder enters the pipeline, it is accelerated by the vacuum pressure and moves along the pipeline. The pipeline's design, including the use of bends and fittings, is optimized to minimize turbulence and pressure loss. The system's efficiency is enhanced by the use of a dilute phase, which reduces the risk of blockages and ensures that the powder is conveyed smoothly.
The discharge point is where the powder is released from the pipeline. It is typically equipped with a valve or a hopper that controls the flow of the material. The discharge point is designed to prevent dust emissions and ensure that the material is handled safely. The system's design allows for easy maintenance and cleaning, which is essential for maintaining its performance and extending its lifespan.
The vacuum dilute phase powder conveying system offers several advantages over traditional conveying methods. One of the key benefits is its ability to transport powders over long distances without the need for intermediate storage or handling. This reduces the risk of material contamination and improves overall efficiency.
Another advantage is the system's ability to handle a wide range of powder types, including fine, dry, and abrasive materials. The design of the components, such as the pipeline and feed hopper, is optimized to withstand the wear and tear caused by these materials, ensuring long-term reliability.
The system also offers improved safety features compared to other conveying methods. The negative pressure environment prevents dust emissions and reduces the risk of explosions or fires. The control system provides real-time monitoring and alerts, allowing operators to take immediate action in case of any issues.
Furthermore, the vacuum dilute phase powder conveying system is energy-efficient and cost-effective. The use of a dilute phase reduces the pressure drop and energy consumption, resulting in lower operating costs. The system's design also minimizes maintenance requirements, reducing downtime and maintenance expenses.
The vacuum dilute phase powder conveying system is widely used in various industries, including food processing, pharmaceuticals, chemicals, and mining. In the food industry, it is used to transport powders such as flour, sugar, and cocoa. In the pharmaceutical industry, it is used to transport active ingredients and other powders. In the chemical industry, it is used to transport raw materials and intermediates. In the mining industry, it is used to transport ore and other minerals.
The system's versatility and efficiency make it an ideal solution for industries that require reliable and safe material transport. The ability to handle a wide range of powder types and operate over long distances makes it a preferred choice for many applications.
The vacuum dilute phase powder conveying system developed by Shandong HeadPowder Engineering Co., Ltd. is a sophisticated and efficient solution for bulk powder handling. Its design and operation are optimized to ensure safe and reliable material transport, with key components working together to deliver optimal performance. The system offers several advantages over traditional conveying methods, including improved efficiency, safety, and cost-effectiveness. With its wide range of applications, the vacuum dilute phase powder conveying system is a valuable asset for industries dealing with bulk powder handling.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top