With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
When it comes to handling bone powder in industrial settings, selecting the right conveying method is crucial for efficiency, safety, and cost-effectiveness. Bone powder, a byproduct of meat processing, requires specialized equipment to transport it from one location to another without degradation or contamination. This article provides a detailed comparison of common bone powder conveying methods, highlighting their advantages, applications, and suitability for different production scales.
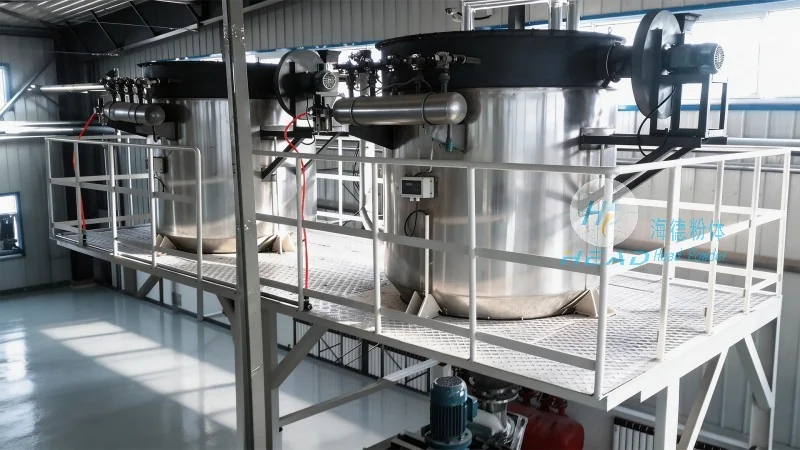
Bone powder, often used as a nutritional supplement or ingredient in animal feed, demands precise handling due to its fine texture and potential for dust generation. The choice of conveying system depends on factors such as material volume, distance, environmental conditions, and the need for hygiene. Below are the most widely used methods in the industry:
Screw conveyors, also known as auger conveyors, are among the most common solutions for bone powder transport. These systems use a rotating helical screw inside a tube to move material forward. For bone powder, which is typically dry and free-flowing, screw conveyors offer several benefits. They are enclosed, preventing dust dispersion and ensuring a clean working environment. The design allows for vertical or inclined transport, making it suitable for elevating bone powder to higher levels or moving it horizontally across production lines. The compact structure of screw conveyors makes them ideal for installations with limited space, a common requirement in meat processing facilities.
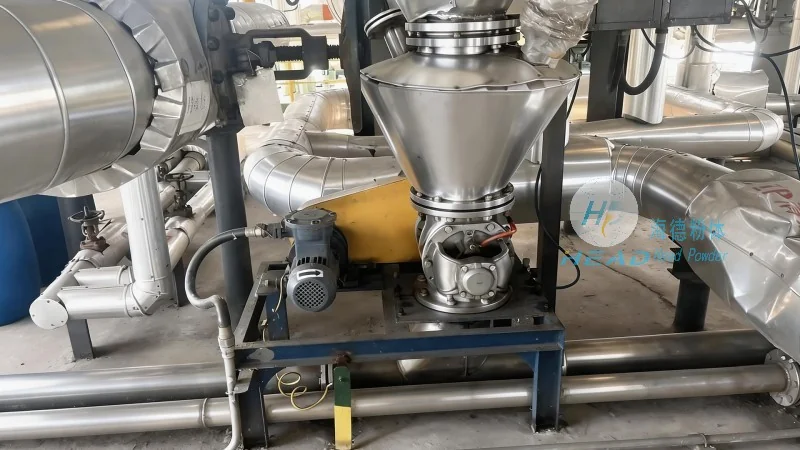
A key advantage of screw conveyors is their ability to handle varying material loads without significant performance drops. This consistency is vital for maintaining production rates in bone powder processing. Additionally, they can be integrated with other equipment, such as grinders or mixers, creating a seamless material flow. The material contact surfaces are often made of stainless steel or other corrosion-resistant materials, ensuring durability and compliance with food safety standards. For companies like Shandong HeadPowder Engineering Co., Ltd., screw conveyors are a core product, designed to meet the specific needs of bone powder handling in various industrial applications.
For applications requiring long-distance or high-volume transport, air-flow or pneumatic conveying systems are preferred. These systems use compressed air to move bone powder through a pipeline. There are two main types: pressure and vacuum systems. Pressure systems push material through the line using positive pressure, while vacuum systems pull material using negative pressure. The choice between them depends on the distance and material characteristics. Air-flow conveyors are particularly effective for fine powders like bone powder, as they minimize material degradation and prevent clogging. The enclosed pipeline design ensures that dust is contained, reducing health risks for workers and maintaining environmental compliance.
One of the significant benefits of pneumatic conveying is its ability to transport bone powder over considerable distances, sometimes up to several hundred meters, without the need for intermediate transfer points. This reduces the number of equipment and labor requirements, enhancing operational efficiency. However, air-flow systems require more energy compared to mechanical conveyors, as they rely on compressed air. Additionally, they may not be suitable for very wet or sticky bone powders, as these can cause blockages in the pipeline. For Shandong HeadPowder Engineering Co., Ltd., air-flow conveying solutions are tailored to handle the unique challenges of bone powder, ensuring reliable and efficient transport in diverse industrial settings.
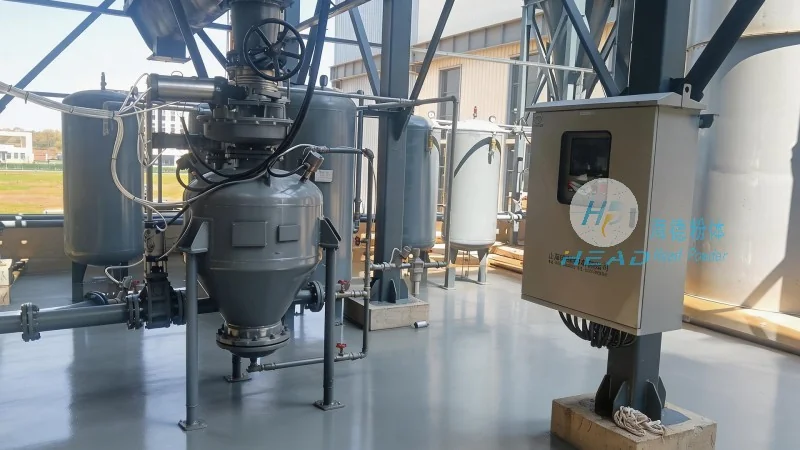
When vertical transport is necessary, bucket elevators are an excellent choice for bone powder. These systems consist of a vertical or inclined conveyor with buckets attached to a chain or belt. As the conveyor rotates, the buckets scoop up bone powder from the bottom and lift it to the top, where it is discharged. Bucket elevators are highly efficient for moving large volumes of material vertically, making them ideal for elevating bone powder from storage silos to processing areas or packaging lines.
The design of bucket elevators allows for high capacity and continuous operation, which is crucial for maintaining production throughput in bone powder processing plants. The enclosed structure prevents dust and material loss, ensuring a clean and safe environment. The buckets are typically made of durable materials like stainless steel or rubber, which can withstand the abrasive nature of bone powder. This makes bucket elevators a long-lasting solution for vertical transport, with low maintenance requirements over time. For companies like Shandong HeadPowder Engineering Co., Ltd., bucket elevators are part of a comprehensive range of bone powder handling equipment, designed to meet the specific vertical transport needs of clients.
Each bone powder conveying method has its strengths and weaknesses, and the best choice depends on the specific requirements of the operation. Screw conveyors are ideal for short to medium distances and horizontal/vertical transport, offering simplicity and low energy consumption. Air-flow systems excel at long-distance transport and fine powders, though they require more energy. Bucket elevators are perfect for vertical transport, providing high capacity and reliability. When selecting a conveying system, factors such as material characteristics, distance, space availability, and budget must be carefully considered.
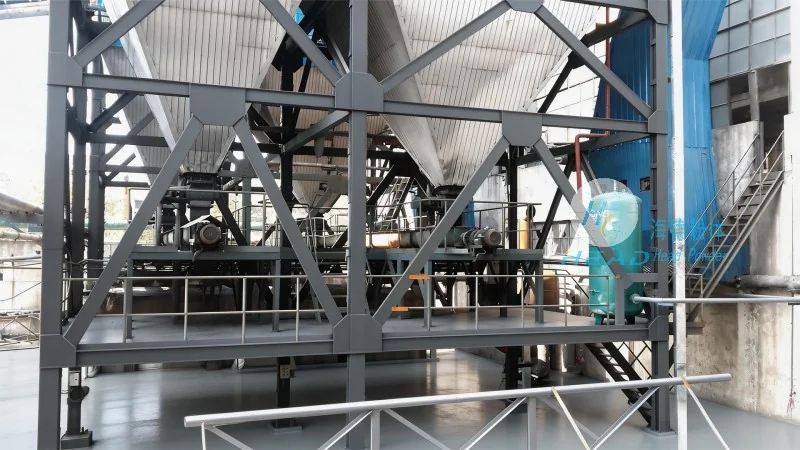
For industrial facilities dealing with bone powder, the choice of conveying method directly impacts operational efficiency, safety, and product quality. Properly designed and maintained conveying systems ensure that bone powder is transported without degradation, contamination, or loss. Companies like Shandong HeadPowder Engineering Co., Ltd. specialize in providing tailored conveying solutions that address the unique challenges of bone powder handling, helping clients optimize their production processes and meet industry standards.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of specialized conveying equipment for the food and animal feed industries. With a focus on innovation and quality, the company provides comprehensive solutions for bone powder handling, including screw conveyors, air-flow systems, and bucket elevators. Headquartered in Shandong, China, the company leverages decades of industry experience to deliver reliable and efficient equipment that meets the stringent requirements of modern processing facilities. The company’s products are designed to enhance operational efficiency, ensure safety, and maintain product integrity, making them a trusted partner for businesses in the bone powder processing sector.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top