With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
The soda ash material handling system equipment, as a critical component in the chemical industry, plays a vital role in the efficient transportation and processing of soda ash. This equipment is designed to ensure smooth material flow from storage to processing units, enhancing overall operational efficiency and safety. For companies like Shandong HeadPowder Engineering Co., Ltd., based in China, such systems are integral to their production capabilities, supporting large-scale industrial operations.

The system typically comprises several key components, each with specific functions to ensure optimal performance. These include feeders, conveyors, storage silos, and control systems. The feeders are responsible for evenly distributing the raw soda ash material into the conveyor system, preventing blockages and ensuring consistent flow. The conveyors, often using belt or screw mechanisms, transport the material horizontally or vertically as required by the production layout. Storage silos provide temporary storage, allowing for buffer capacity to accommodate fluctuations in production rates. The control systems, equipped with sensors and automation technology, monitor and regulate the entire process, ensuring that the material handling operates within safe and efficient parameters.
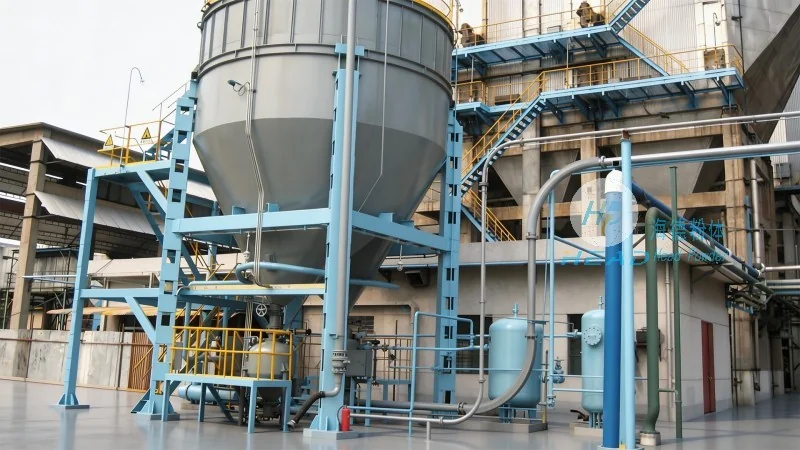
The operation process of the soda ash material handling system begins with the loading of raw soda ash into the storage silo. The feeder then activates, distributing the material into the conveyor belt. The conveyor transports the material to the processing unit or secondary storage location. Throughout this process, the control system continuously monitors the flow rate, pressure, and temperature to maintain optimal conditions. In case of any anomalies, such as blockages or excessive pressure, the system automatically triggers safety mechanisms to prevent equipment damage or material loss. This automated operation ensures high reliability and minimal downtime, which is crucial for maintaining production continuity in industrial settings.
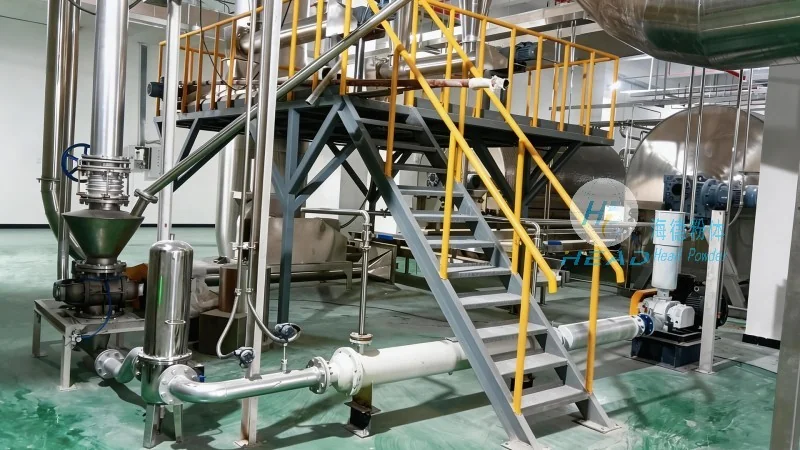
The working principle of the soda ash material handling system is based on mechanical and pneumatic principles, tailored to handle the specific characteristics of soda ash, such as its bulk density and flowability. The feeder uses a rotating mechanism to break up any agglomerates and distribute the material evenly. The conveyor system utilizes friction or gravity to move the material along the designated path. The storage silo employs a hopper design to facilitate smooth discharge, reducing the risk of material bridging. The control system integrates sensors like level detectors and pressure transmitters to provide real-time data, enabling precise control over the material flow. This integrated approach ensures that the system operates efficiently, minimizing energy consumption while maximizing throughput.
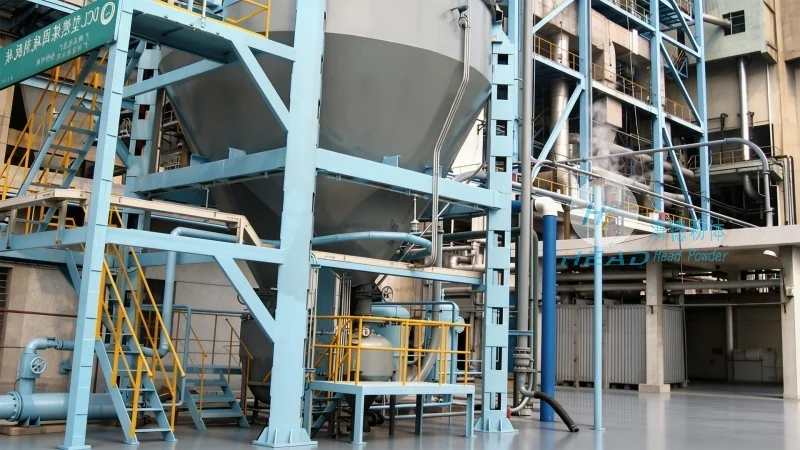
Implementing a soda ash material handling system offers numerous benefits for industrial operations. It enhances production efficiency by reducing manual handling and minimizing material loss. The automated control systems improve safety by eliminating human exposure to hazardous materials and reducing the risk of accidents. Additionally, the system's scalability allows for expansion as production needs grow, providing long-term investment value. Companies like Shandong HeadPowder Engineering Co., Ltd. utilize these systems in various applications, including chemical manufacturing, glass production, and water treatment, where soda ash is a key raw material. The system's adaptability to different production scales and operational requirements makes it a versatile solution for modern industrial needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top