With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Pharmaceutical bulk material pneumatic conveying systems are critical components in modern pharmaceutical manufacturing, designed to efficiently transport powders and granules from one location to another within a facility. These systems leverage the principles of air flow to move materials, ensuring a clean, controlled, and hygienic process that meets stringent industry standards. The core of such systems lies in their ability to handle sensitive pharmaceutical materials without contamination or degradation, making them indispensable in pharmaceutical production lines.
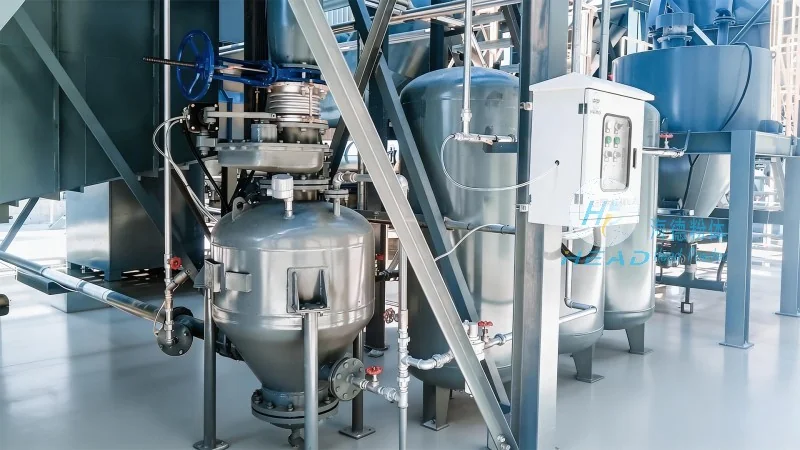
The fundamental principle behind pharmaceutical pneumatic conveying is the use of compressed air or other gases to create a flow that propels bulk materials through a pipeline. There are primarily two types of pneumatic conveying systems: pressure and vacuum. Pressure systems operate by introducing compressed air into a hopper or storage tank, which forces the material into the conveying line. Vacuum systems, on the other hand, use a vacuum pump to create a negative pressure that draws material from a source into the system. Both methods are engineered to maintain the integrity of the pharmaceutical product, ensuring that it remains free from moisture, dust, and microbial contamination. The design of these systems includes features such as air filtration, material separation, and flow control mechanisms to optimize performance and safety.
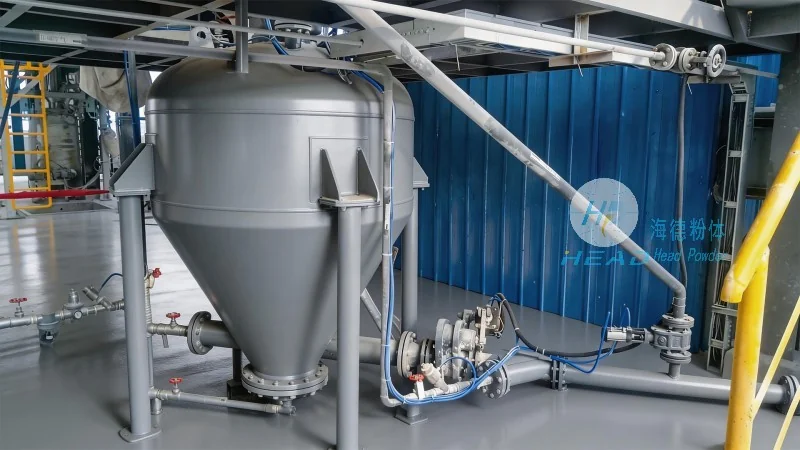
The application scenarios of pharmaceutical pneumatic conveying systems are diverse and tailored to specific manufacturing needs. In pharmaceutical facilities, these systems are commonly used in areas like raw material handling, intermediate processing, and final product packaging. For instance, in raw material storage, pneumatic conveyors can transport raw powders from bulk containers to processing units, reducing manual handling and minimizing the risk of cross-contamination. During intermediate processing, such as blending or granulation, pneumatic systems facilitate the transfer of materials between different processing stages, ensuring consistent product quality. In the final packaging stage, these systems can deliver finished products to packaging lines, maintaining the sterile environment required for pharmaceutical products. Additionally, the flexibility of pneumatic conveying allows for integration into existing production lines, enabling manufacturers to adapt to changing production demands without significant infrastructure changes.
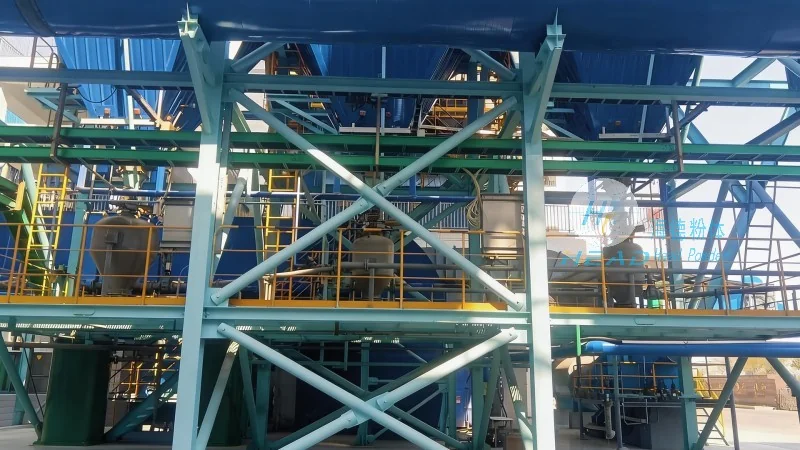
HeadPowder, a leading manufacturer of pharmaceutical processing equipment, specializes in the design, development, and production of advanced pneumatic conveying systems tailored to the pharmaceutical industry. With a strong focus on quality and compliance, HeadPowder’s products are engineered to meet the stringent requirements of GMP (Good Manufacturing Practice) and other regulatory standards. The company’s headquarters is located in Shandong, China, where it leverages advanced manufacturing capabilities and a team of experienced engineers to deliver high-performance solutions. HeadPowder’s commitment to innovation and customer satisfaction has established it as a trusted partner for pharmaceutical manufacturers worldwide, providing reliable and efficient equipment that enhances production efficiency and product quality.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top