With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced material handling solutions. Among their portfolio is the Maltose Material Pneumatic Conveying System, a sophisticated technology tailored for the efficient transport of maltose and similar bulk materials. This system integrates pneumatic conveying principles with industrial-grade engineering to ensure reliable, low-maintenance operation in various production environments.
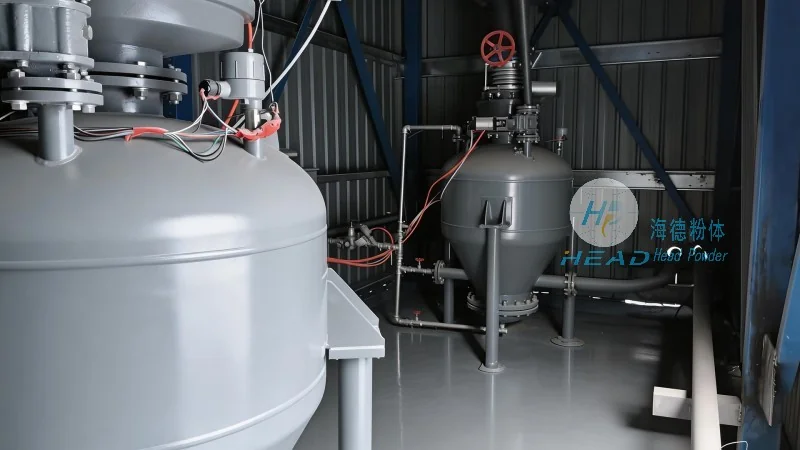
The core principle of the Maltose Material Pneumatic Conveying System revolves around the use of compressed air to transport dry, free-flowing materials like maltose through a network of pipes. The system operates by creating a pressure differential between the material feed point and the discharge point. Compressed air is introduced into the system, drawing the maltose particles into the conveying line. As the air flows through the pipes, it carries the material along, ensuring a continuous and controlled flow. This method eliminates the need for mechanical components such as belts or buckets, reducing friction and wear on the material and the equipment. The system can be configured as either a positive pressure or negative pressure system, depending on the specific requirements of the application and the characteristics of the maltose being handled.
The Maltose Material Pneumatic Conveying System is designed to operate effectively in diverse industrial settings, particularly in food processing and pharmaceutical manufacturing where the quality and purity of maltose are critical. Key characteristics of its working scenes include:
1. Hygienic and Clean Environment: The system is constructed from materials that meet stringent food-grade standards, ensuring that the maltose remains uncontaminated during transport. The design minimizes dead zones and easy-to-clean surfaces, which is essential for maintaining compliance with regulatory standards in the food industry.
2. Low Maintenance and Longevity: By eliminating moving parts in the conveying line, the system reduces the risk of mechanical failure and the need for frequent maintenance. This results in lower operational costs and extended service life, making it a cost-effective solution for long-term use.
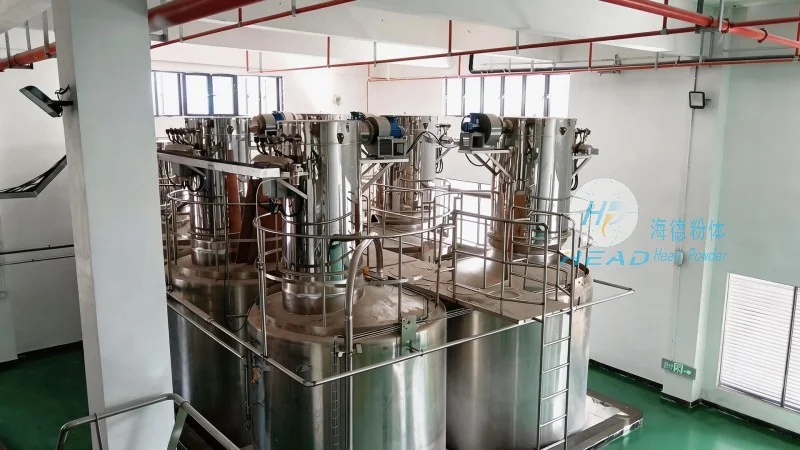
3. Flexible and Scalable Configuration: The system can be customized to accommodate different production volumes and layout requirements. It can be integrated with existing production lines or designed as a standalone unit, allowing for flexibility in plant expansion or reconfiguration.
4. Energy Efficiency: Advanced control systems optimize air pressure and flow rates, minimizing energy consumption while maintaining efficient material transport. This contributes to lower operational expenses and a reduced environmental footprint.
HeadPowder's Maltose Material Pneumatic Conveying System is particularly well-suited for applications where the consistent and hygienic handling of maltose is paramount. Typical working scenes include:
1. Food Processing Plants: In bakeries, confectioneries, and malt production facilities, the system efficiently transports maltose from storage silos to mixing and processing equipment. Its ability to handle bulk quantities without product degradation ensures smooth production workflows.
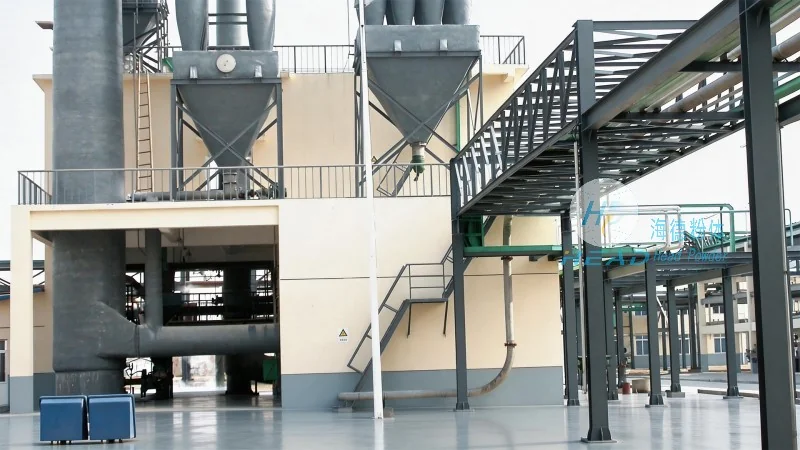
2. Pharmaceutical Manufacturing: For pharmaceutical companies producing maltose-based products, the system provides a sterile and controlled environment for material transport. The system's compliance with GMP (Good Manufacturing Practice) standards makes it an ideal choice for maintaining product integrity and regulatory compliance.
3. Industrial Bulk Handling: In industrial settings where maltose is used as an ingredient in various products, the system offers a reliable method for moving large volumes of material between different stages of production, such as from raw material storage to packaging lines.
Implementing the Maltose Material Pneumatic Conveying System from HeadPowder offers several advantages that enhance operational efficiency and product quality. These include:
1. Improved Product Quality: The system minimizes product degradation due to reduced friction and exposure to air, ensuring that the maltose maintains its quality and nutritional properties throughout the transport process.
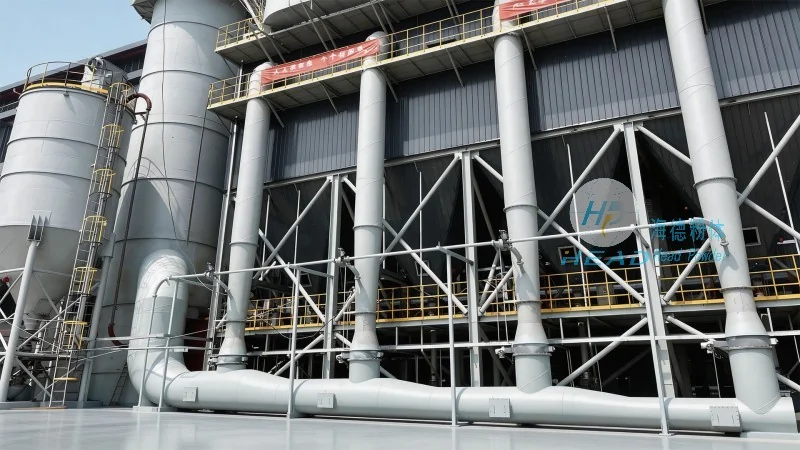
2. Enhanced Safety: By eliminating the need for manual handling of bulk materials, the system reduces the risk of workplace accidents and exposure to dust or other contaminants, creating a safer working environment.
3. Space Efficiency: The compact design of the pneumatic conveying system allows for installation in areas with limited space, making it suitable for retrofitting into existing production facilities.
4. Cost Savings: With lower maintenance requirements and energy-efficient operation, the system provides long-term cost savings compared to traditional mechanical conveying methods.
HeadPowder's Maltose Material Pneumatic Conveying System exemplifies advanced engineering solutions for the efficient and hygienic handling of maltose in industrial applications. By leveraging pneumatic conveying principles and adhering to stringent quality standards, the system addresses the unique challenges of maltose transport while delivering reliable performance and operational benefits. For companies in the food and pharmaceutical industries seeking to optimize their material handling processes, this system represents a robust and cost-effective choice.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top