With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Lightweight aggregate powder conveying systems are essential equipment in modern construction and material handling industries. These systems are designed to efficiently transport lightweight aggregate powders, which are widely used in applications such as concrete production, insulation materials, and other construction-related processes. The technology behind these systems combines advanced engineering principles with practical application, ensuring reliable and efficient material movement. In this article, we will explore the fundamental principles of lightweight aggregate powder conveying systems, as well as the key working scene characteristics that define their performance and suitability in various industrial settings.
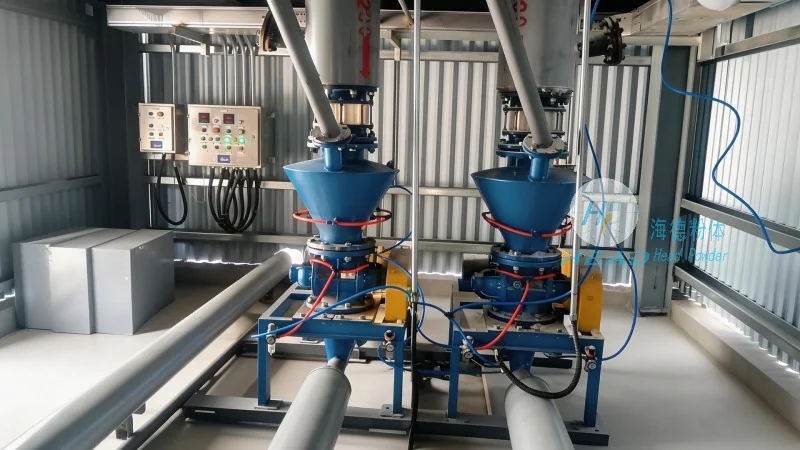
HeadPowder, the manufacturer of these advanced conveying systems, is a leading company based in Shandong, China. With a strong commitment to innovation and quality, HeadPowder specializes in the design, development, and production of high-performance powder handling equipment. The company's expertise lies in creating customized solutions tailored to the specific needs of clients across different industries. By leveraging years of experience and cutting-edge technology, HeadPowder ensures that its products meet the highest standards of efficiency, durability, and reliability. The company's headquarters is located in Shandong, China, where it maintains a state-of-the-art manufacturing facility and a dedicated team of engineers and technicians.
The operation of lightweight aggregate powder conveying systems is based on several key principles that ensure optimal performance. One of the primary principles is the use of specialized components such as conveyor belts, pneumatic systems, or mechanical conveyors, which are engineered to handle the unique properties of lightweight aggregates. These materials typically have low density and can be prone to dust generation, making it crucial to design the system with features that minimize particle loss and maintain consistent flow. The systems also incorporate advanced control mechanisms, including sensors and automation controls, to monitor and adjust the conveying process in real-time. This ensures that the material is transported smoothly and without interruption, even under varying load conditions. Additionally, the design of the system considers factors such as material compatibility, space constraints, and environmental regulations, ensuring that it meets the specific requirements of each application.
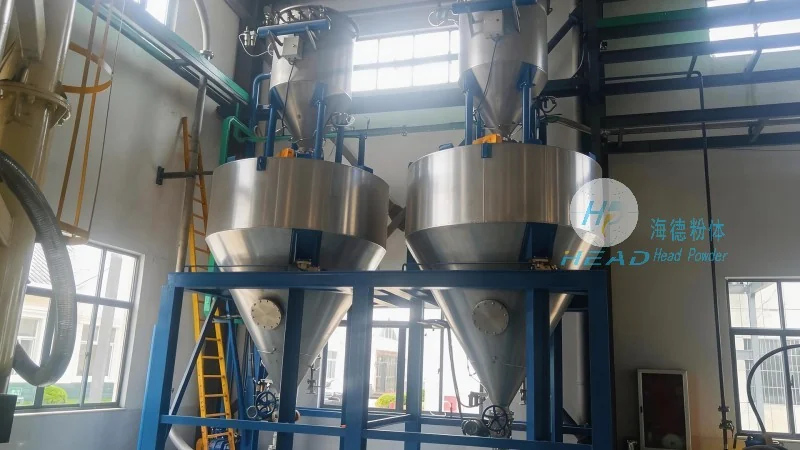
The working scene characteristics of lightweight aggregate powder conveying systems are tailored to meet the diverse needs of industrial environments. These systems are commonly used in concrete batching plants, where they facilitate the efficient transport of lightweight aggregates from storage silos to mixing stations. In insulation material production, the systems ensure that lightweight powders are delivered to processing lines without clogging or degradation. The systems are also utilized in construction sites for on-site material handling, allowing for quick and reliable supply of aggregates to concrete mixers. The working scene characteristics include high throughput capacity, low energy consumption, and minimal maintenance requirements, making them suitable for continuous operation in demanding industrial settings. Furthermore, the systems are designed to be adaptable, allowing for integration with existing infrastructure and processes, which enhances overall operational efficiency.

Lightweight aggregate powder conveying systems offer several advantages that make them a preferred choice for industrial applications. These systems provide high efficiency in material handling, with the ability to transport large volumes of lightweight aggregates at consistent speeds. The use of advanced materials and engineering reduces wear and tear, leading to lower maintenance costs and longer equipment lifespan. The systems also contribute to improved safety in the workplace by minimizing dust exposure and ensuring smooth material flow, which reduces the risk of accidents. Performance metrics such as conveying capacity, pressure drop, and energy consumption are carefully optimized to ensure that the systems operate within optimal parameters. These metrics are regularly monitored and adjusted to maintain peak performance, ensuring that the equipment meets the evolving needs of the industry.
Lightweight aggregate powder conveying systems, as developed by Shandong HeadPowder Engineering Co., Ltd., represent a significant advancement in material handling technology. By combining innovative design with practical application, these systems provide reliable and efficient solutions for transporting lightweight aggregates in various industrial settings. The company's commitment to quality and customer satisfaction ensures that its products are tailored to meet the specific requirements of clients, enhancing overall operational efficiency and productivity. As the construction and material handling industries continue to evolve, the demand for advanced powder conveying systems is expected to grow, and companies like HeadPowder are well-positioned to meet these needs with their expertise and dedication to excellence.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top