With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Straw ash powder conveying equipment serves as a specialized material handling device, designed to efficiently transport straw ash powders in various industrial and agricultural settings. This equipment addresses the unique challenges posed by straw ash, such as its fine particle size, light weight, and potential for dust generation. By leveraging advanced engineering principles, the system ensures safe, reliable, and efficient material movement while maintaining environmental standards. The following sections will explore the fundamental operational principles and the diverse working scenarios where this equipment excels.
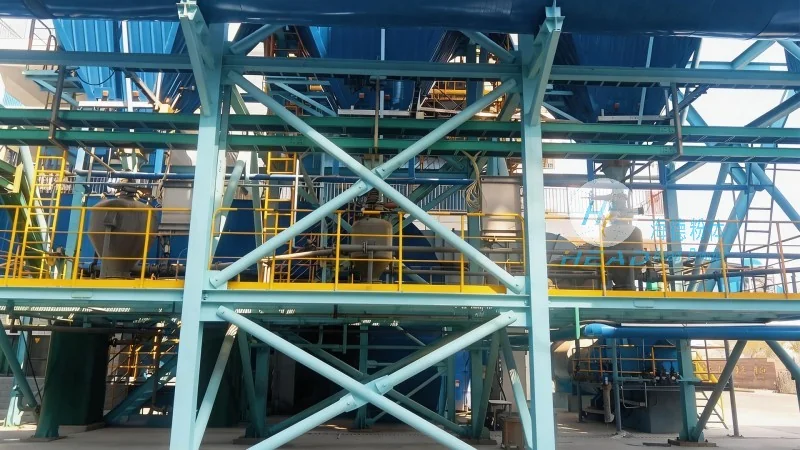
The core mechanism of straw ash powder conveyors centers on the utilization of air or mechanical forces to move powders through a sealed system. Typically, these systems employ either positive pressure (pneumatic) or negative pressure (suction) air flow to create a conveying medium that transports the material from the source to the destination. The design incorporates features like flexible hoses, rotary airlock valves, and dust collection units to maintain a consistent and clean operation. The equipment is engineered to handle the inherent properties of straw ash, including its tendency to clump or generate static charges, by integrating anti-static materials and robust sealing mechanisms. This ensures uninterrupted material flow and prevents issues like blockages or material buildup within the system.
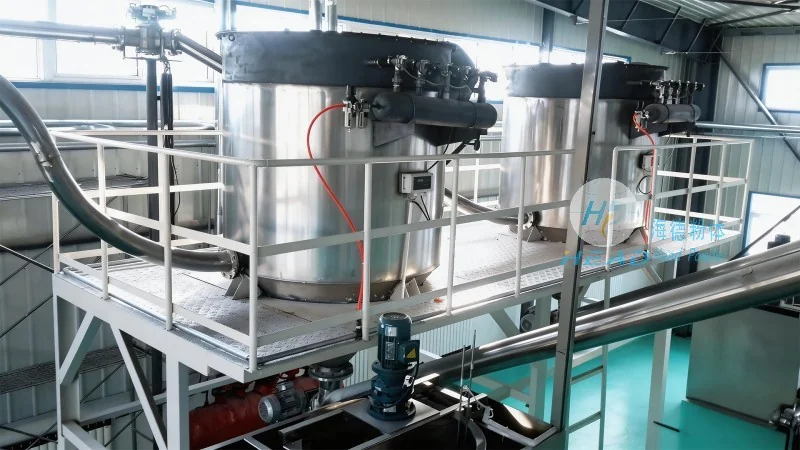
Several critical components work in concert to ensure the effective operation of straw ash powder conveyors. The feed hopper is responsible for receiving and feeding the straw ash material into the conveying system. It often includes vibration or agitation features to prevent material bridging and ensure a steady flow. The conveyor itself, which may be pneumatic or mechanical, uses either air pressure or mechanical motion to transport the powder. In pneumatic systems, a blower or compressor generates the necessary air flow, while mechanical systems rely on screws, belts, or buckets. The discharge unit then delivers the straw ash to the target location, such as a storage silo or processing unit. Additionally, integrated dust collection and filtration systems capture airborne particles, maintaining air quality and complying with environmental regulations. These components are carefully selected and configured to meet the specific demands of straw ash handling, ensuring optimal performance and longevity.
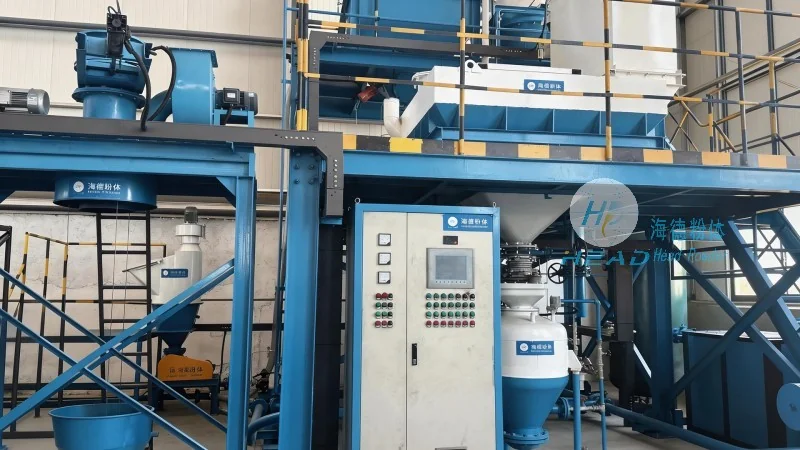
Straw ash powder conveyors are widely utilized in diverse applications where efficient handling of straw ash is essential. Common working scenarios include agricultural processing facilities, where straw ash is a byproduct of biomass combustion or processing, and industrial plants that use straw ash as a raw material for manufacturing or energy production. In these environments, the equipment must operate in conditions that may involve high temperatures or humidities, requiring construction from heat-resistant and corrosion-resistant materials. For instance, in a biomass power plant, the conveyor may transport straw ash from the combustion chamber to a storage silo, where it can be further processed or used as a fuel additive. Another application is in the production of straw ash-based building materials, where the conveyor ensures a consistent supply of raw material to mixing and molding processes. The versatility of straw ash powder conveyors makes them suitable for both small-scale agricultural operations and large-scale industrial facilities, adapting to various material flow rates and discharge locations.
Implementing straw ash powder conveying equipment offers significant advantages for businesses dealing with straw ash materials. One primary benefit is the substantial improvement in operational efficiency, as the equipment can handle large volumes of material with minimal labor input. The sealed system design reduces dust exposure, enhancing workplace safety and compliance with environmental regulations. Additionally, the equipment minimizes material loss and waste, as the conveying process is highly efficient and reduces the need for manual handling. The ability to handle fine powders without clogging or blockages is another key advantage, ensuring continuous material flow. Furthermore, the equipment can be customized to meet specific operational requirements, such as varying flow rates or different discharge points. This flexibility allows businesses to adapt the equipment to their unique processes, maximizing utility and return on investment. The long-term durability and low maintenance requirements of modern straw ash powder conveyors also contribute to cost savings over time, making them a practical choice for sustainable material handling solutions.
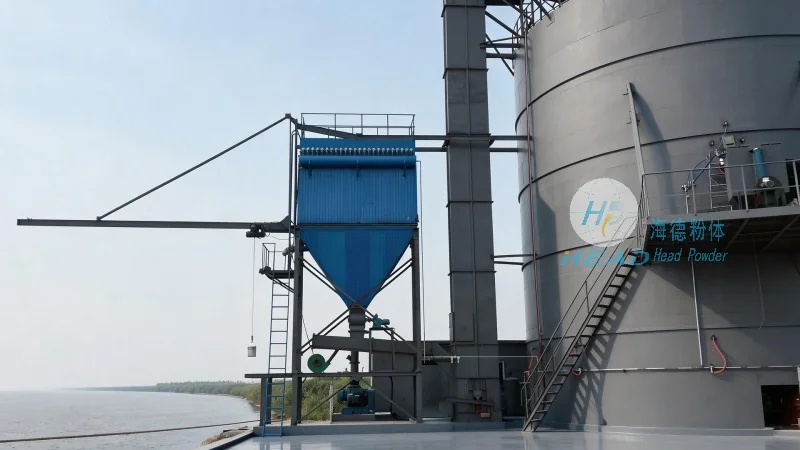
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of specialized material handling equipment, including straw ash powder conveyors. Headpowder is committed to innovation and quality, establishing itself as a trusted partner in the industry. The company’s products are designed and manufactured in China, leveraging advanced technology and rigorous quality control processes to ensure reliability and performance. Headpowder’s headquarters is located in Shandong, China, where it operates a state-of-the-art production facility and research and development center. The company focuses on providing tailored solutions by working closely with clients to understand their specific material handling challenges and develop customized equipment. Headpowder’s team of engineers and technicians, with extensive industry experience, ensures each product is engineered for optimal performance and longevity. By adhering to international standards and maintaining a customer-centric approach, headpowder has built a reputation for excellence in the material handling sector, serving clients both domestically and internationally.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top