With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
When it comes to the efficient and safe handling of fine chemicals in industrial processes, specialized material handling systems play a crucial role. These systems are designed to manage the transport of chemicals with high precision, ensuring minimal contamination and optimal performance. The equipment used in such systems is engineered to meet the stringent requirements of the fine chemical industry, offering reliable solutions for various material handling challenges.
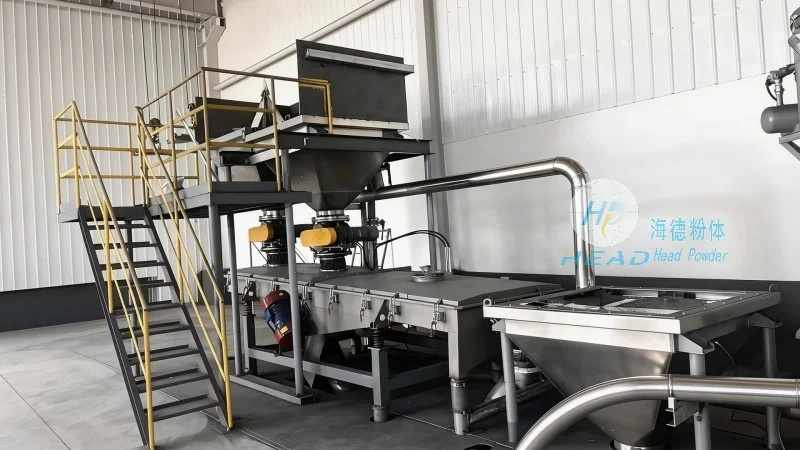
Fine chemical material handling systems are sophisticated setups that integrate multiple components to facilitate the movement of chemicals from storage to processing units. These systems are typically composed of pumps, valves, pipelines, and control units, all working in harmony to maintain the integrity of the chemical products. The design of these systems takes into account factors such as chemical compatibility, temperature control, and pressure management, ensuring that the materials are handled without degradation or loss of quality.
The working principles of fine chemical material handling equipment revolve around the efficient transfer of liquids or powders through a closed system. For liquid chemicals, positive displacement pumps or centrifugal pumps are commonly used, depending on the viscosity and flow rate requirements. These pumps generate the necessary pressure to move the material through the pipelines, while maintaining a consistent flow rate. In the case of powder handling, pneumatic conveying systems or screw conveyors are employed, utilizing air pressure or mechanical force to transport the solid materials. The control systems, often equipped with sensors and automation technology, monitor the flow rate, pressure, and temperature in real-time, adjusting the operation as needed to prevent any deviations from the desired parameters.
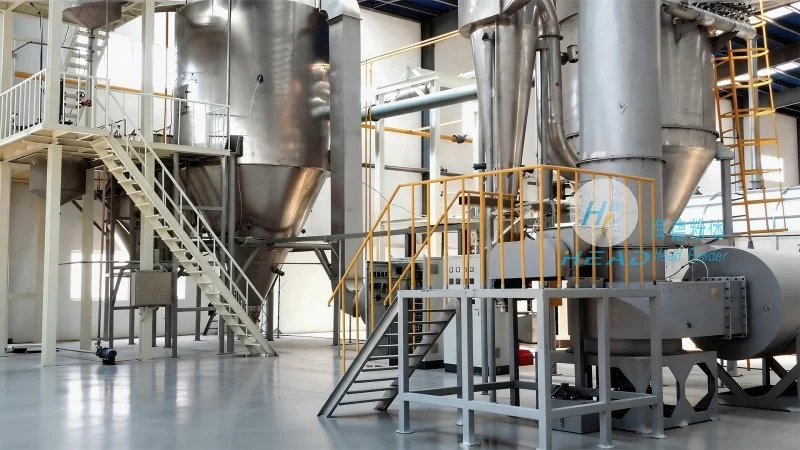
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, offers a range of equipment that embodies several key features essential for fine chemical applications. One of the primary features is the high level of precision and accuracy in material measurement and transfer. The equipment is designed with calibrated components that ensure minimal error in the quantity of chemicals being handled, which is critical for maintaining product consistency and meeting regulatory standards. Another significant feature is the corrosion resistance of the materials used in the construction of the system components. Fine chemicals often have aggressive properties that can damage standard equipment, so the use of corrosion-resistant materials like stainless steel or specialized polymers is essential to prolong the equipment's lifespan and maintain product purity.
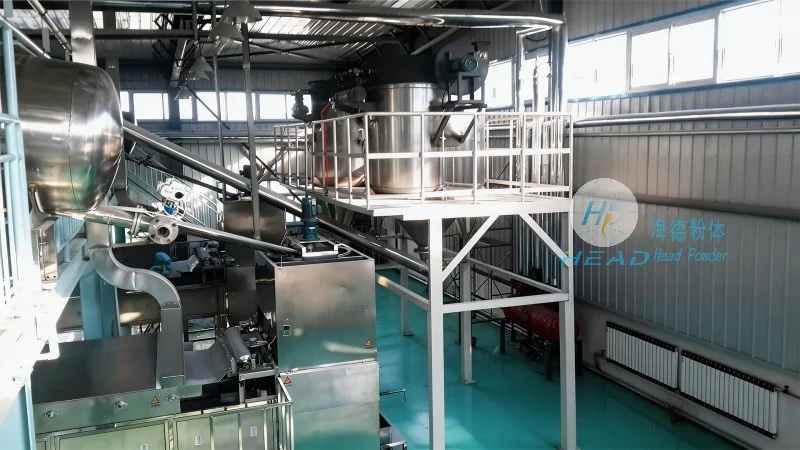
Automation and integration are also prominent features in modern fine chemical material handling systems. The systems are equipped with advanced control panels and software that allow for remote monitoring and operation, enhancing operational efficiency and reducing the risk of human error. Additionally, the modular design of the equipment enables easy maintenance and scalability, allowing companies to adapt the system as their production needs evolve. The integration of safety features, such as pressure relief valves and emergency shut-off mechanisms, further ensures the safety of personnel and the integrity of the process.
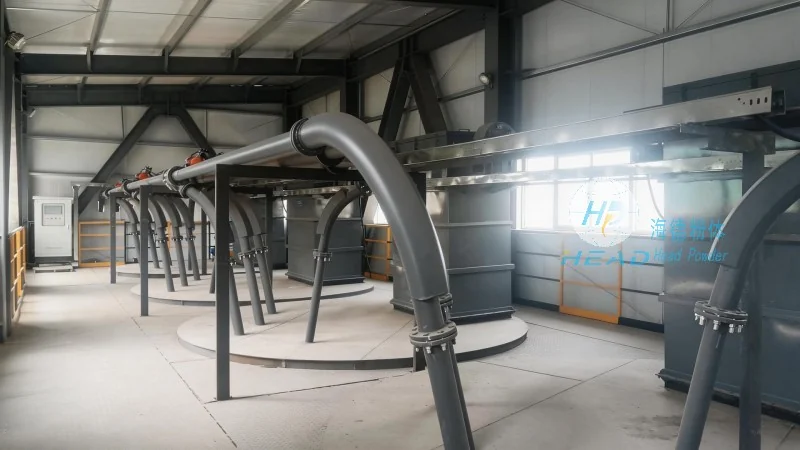
The effectiveness of fine chemical material handling systems is evident in various industrial applications. For instance, in pharmaceutical manufacturing, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients with utmost care, ensuring that the final drug products meet the stringent quality standards. In the chemical manufacturing sector, the systems are crucial for handling specialty chemicals, such as dyes, pigments, and solvents, where even a small amount of contamination can affect the final product's properties. The consistent performance of these systems contributes to higher productivity, reduced waste, and improved overall operational efficiency in the fine chemical industry.
As the demand for high-quality fine chemicals continues to grow, the importance of reliable material handling systems cannot be overstated. Shandong HeadPowder Engineering Co., Ltd. stands out as a trusted provider of advanced equipment designed to meet the unique challenges of the fine chemical industry. With a focus on precision, durability, and automation, their material handling systems offer solutions that enhance productivity while ensuring the safety and quality of the products. Based in Shandong, China, the company leverages its expertise and local resources to deliver tailored solutions that cater to the specific needs of their clients, supporting the growth and success of the fine chemical sector.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top