With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
This article provides an in-depth look at the working principle and key features of metering bin pump powder conveying systems, which are widely used in industrial applications for efficient and reliable powder transport. The system, often associated with the brand "headpowder" from Shandong HeadPowder Engineering Co., Ltd., based in China, represents a sophisticated solution for handling bulk powders in various industries.
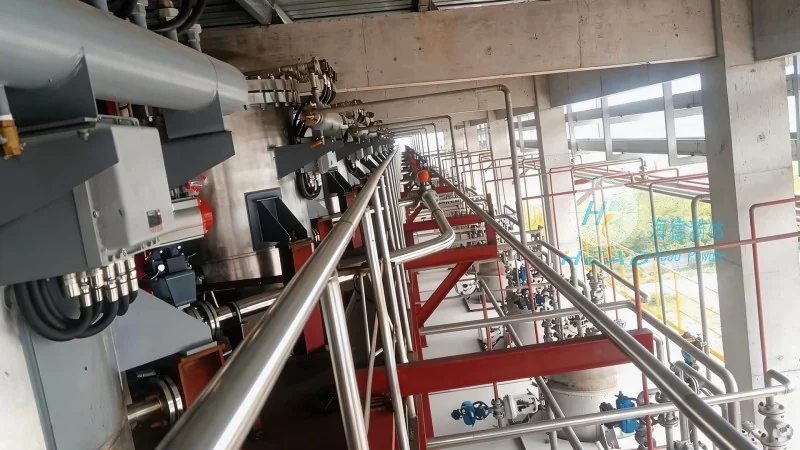
The metering bin pump operates on a principle that combines the functions of a bin and a pump, enabling precise control over the flow of powders. At its core, the system consists of a hopper or bin where the powder is stored, a pump mechanism that draws the material from the bin, and a discharge system that delivers the powder to the target location. The process typically involves the following steps: first, the powder is fed into the bin, where it accumulates under gravity. Then, the pump, often a diaphragm or piston type, creates a vacuum or pressure to draw the powder from the bin into the pump chamber. As the pump cycles, it discharges the powder through a pipeline to the destination. The metering function is achieved through adjustable parameters such as pump speed, pressure, and the level of the powder in the bin, allowing for accurate control of the flow rate. This precision is crucial for applications where consistent dosing or flow rates are required, such as in chemical processing, food production, or pharmaceutical manufacturing.
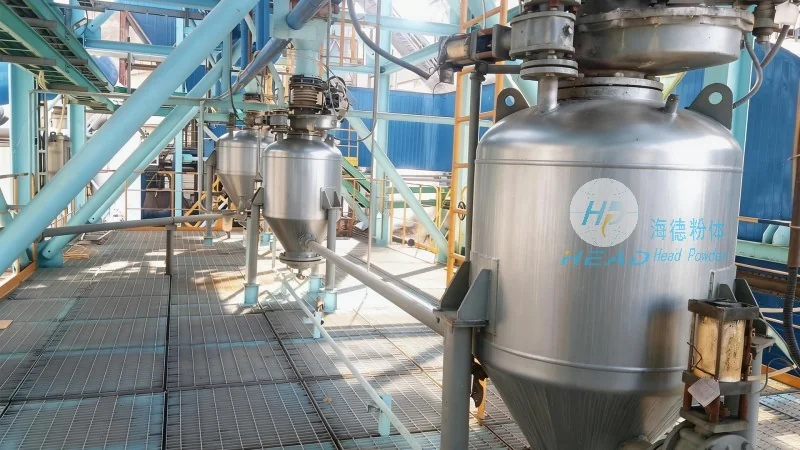
HeadPowder's metering bin pump systems are designed with several standout features that enhance their performance and versatility. One of the primary features is the ability to handle a wide range of powder types, from fine powders to bulkier granules, without clogging or degradation. The system's robust construction, typically made from corrosion-resistant materials like stainless steel, ensures durability and longevity, even in harsh industrial environments. Another important feature is the integrated metering capability, which allows for precise control of the powder flow rate. This is achieved through advanced control systems that can adjust the pump's operation based on real-time feedback from sensors monitoring the bin level or flow rate. The system also offers flexibility in terms of discharge options, with options for direct pipeline discharge or connection to downstream equipment like mixers or reactors. Additionally, the metering bin pump is known for its low maintenance requirements, as the pump mechanism is designed to minimize wear and tear, reducing downtime and operational costs. The system's energy efficiency is another notable feature, with optimized pump designs that use less power while maintaining high flow rates. These features collectively make the metering bin pump an ideal choice for industries that demand reliability, precision, and efficiency in powder handling.
The metering bin pump powder conveying system from Shandong HeadPowder Engineering Co., Ltd. finds applications across various industries where bulk powder transport is essential. In the chemical industry, it is used for transporting raw materials and finished products, ensuring consistent quality and preventing contamination. In the food and beverage sector, the system is employed for handling ingredients like flour, sugar, or spices, maintaining hygiene standards and preventing cross-contamination. The pharmaceutical industry benefits from the system's ability to handle sensitive powders, such as active pharmaceutical ingredients (APIs), with precision and minimal risk of product degradation. Other applications include the cement and construction industries, where the system efficiently transports raw materials like limestone or sand, and the agricultural sector, where it handles fertilizers or seeds. The benefits of using this system include improved process control, reduced material waste, and enhanced safety due to the enclosed design that minimizes dust exposure. Furthermore, the system's ability to handle different powder types without modification makes it a versatile solution for diverse industrial needs.
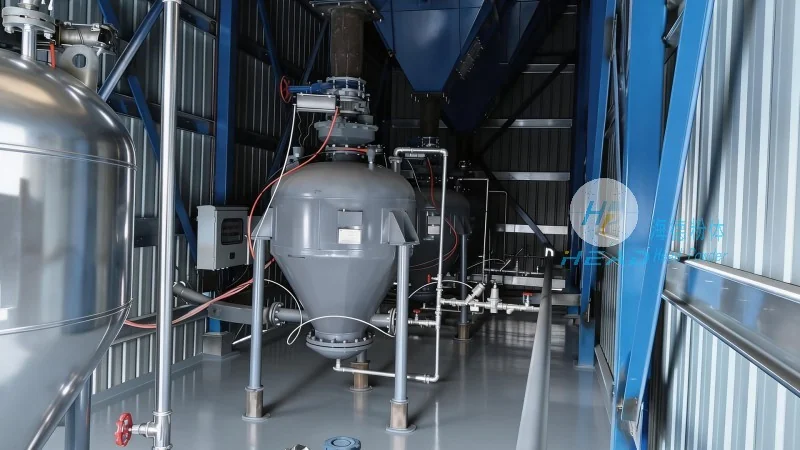
In conclusion, the metering bin pump powder conveying system is a highly effective and reliable solution for bulk powder transport, offering precise control and efficient operation. Developed by Shandong HeadPowder Engineering Co., Ltd., a company based in China, this system combines advanced engineering with practical design to meet the demands of modern industrial applications. The working principle, which integrates a bin and pump mechanism, allows for accurate metering and consistent flow rates, while key features such as durability, flexibility, and low maintenance make it a preferred choice for industries worldwide. As a leader in powder handling technology, HeadPowder continues to innovate and provide solutions that enhance productivity and safety in industrial processes. The system's ability to handle a wide range of powders and its integration with control systems ensures that it remains a valuable asset for any facility requiring efficient powder transport.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top