

What is a dust-free automatic powder pneumatic conveying machine? What are its design principles?
When it comes to efficient and clean powder handling in industrial settings, the dust-free automatic powder pneumatic conveying machine has emerged as a critical solution. This equipment is designed to transport powders and granules with minimal contamination and maximum efficiency, making it indispensable in sectors such as pharmaceuticals, food processing, and chemical manufacturing. Understanding its functionality and design principles is essential for businesses seeking to optimize their material handling processes.
Introduction to the Dust-Free Automatic Powder Pneumatic Conveying Machine
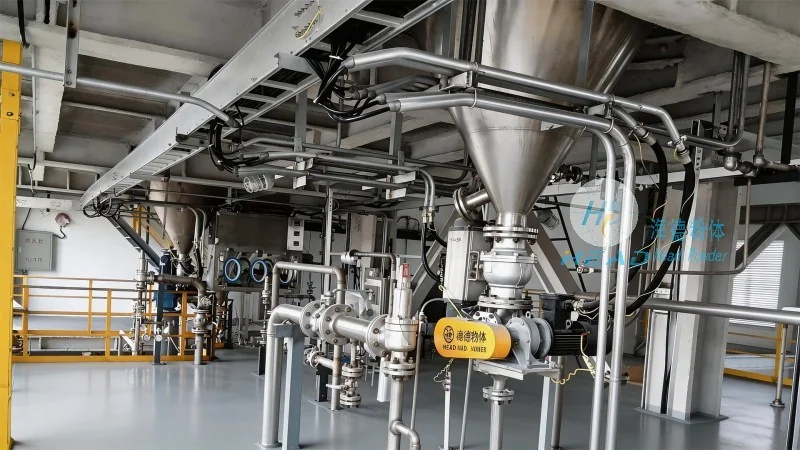
The dust-free automatic powder pneumatic conveying machine, also known as a pneumatic conveyor, is a system that uses compressed air or gas to move bulk materials through a pipeline. Unlike traditional mechanical conveyors, this system eliminates the need for physical contact between the material and the conveyor components, thereby reducing the risk of contamination and cross-contamination. The machine operates by creating a pressure differential within the pipeline, which draws the powder from the source and transports it to the destination. This method is particularly advantageous for handling sensitive materials that require strict cleanliness standards.
Key Design Principles of the Dust-Free Automatic Powder Pneumatic Conveying Machine
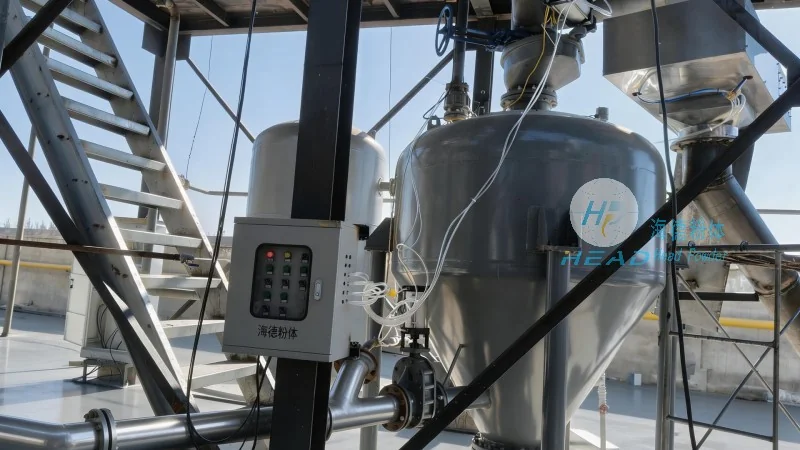
The design of a dust-free automatic powder pneumatic conveying machine is centered around several core principles to ensure optimal performance and compliance with industry standards. First, the system incorporates airtight and sealed components to prevent dust leakage and maintain a clean environment. This is achieved through the use of high-quality materials, such as stainless steel, and advanced sealing technologies that minimize the risk of particle escape. Second, the machine is equipped with an automated control system that regulates the flow of air and material, ensuring consistent and reliable operation. This control system typically includes sensors and valves that monitor pressure, flow rate, and material level, allowing for real-time adjustments to maintain optimal performance. Third, the design emphasizes energy efficiency by optimizing the air pressure and flow rates required for material transport. By reducing unnecessary energy consumption, the machine not only lowers operational costs but also contributes to environmental sustainability.
How the Dust-Free Automatic Powder Pneumatic Conveying Machine Works
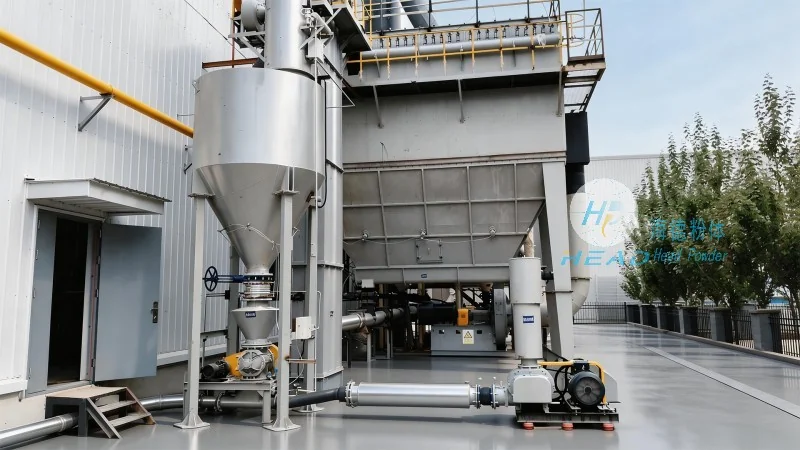
At its core, the dust-free automatic powder pneumatic conveying machine operates through a combination of air pressure and material properties. The process begins with the material being fed into the inlet of the machine, where it is then mixed with compressed air. The air, which is typically introduced at a specific pressure, creates a flow that propels the powder through the pipeline. The machine uses a series of components, including a hopper, a venturi, and a receiver, to control the flow and ensure efficient transport. The venturi, in particular, plays a crucial role by creating a low-pressure zone that draws the powder into the air stream, enhancing the conveying efficiency. The receiver at the end of the pipeline collects the material and separates it from the air, which is then filtered and recycled back into the system. This closed-loop system minimizes waste and ensures that the material remains within the controlled environment throughout the entire process.
Advantages of Using a Dust-Free Automatic Powder Pneumatic Conveying Machine
Implementing a dust-free automatic powder pneumatic conveying machine offers numerous advantages for industrial applications. Firstly, it provides a highly efficient method of transporting powders over long distances without the need for multiple transfer points or manual handling. This reduces labor costs and improves operational efficiency. Secondly, the machine’s design minimizes the risk of dust contamination, which is critical in industries where product purity is paramount, such as pharmaceuticals and food processing. By maintaining a clean environment, the machine helps to prevent product recalls and ensures compliance with regulatory standards. Thirdly, the automated control system allows for precise control over the material flow, enabling businesses to adjust the conveying rate according to production needs. This flexibility is particularly valuable in dynamic manufacturing environments where production demands fluctuate. Additionally, the machine’s energy-efficient design contributes to lower operational costs and reduced environmental impact, making it a sustainable choice for modern industries.
Applications of the Dust-Free Automatic Powder Pneumatic Conveying Machine
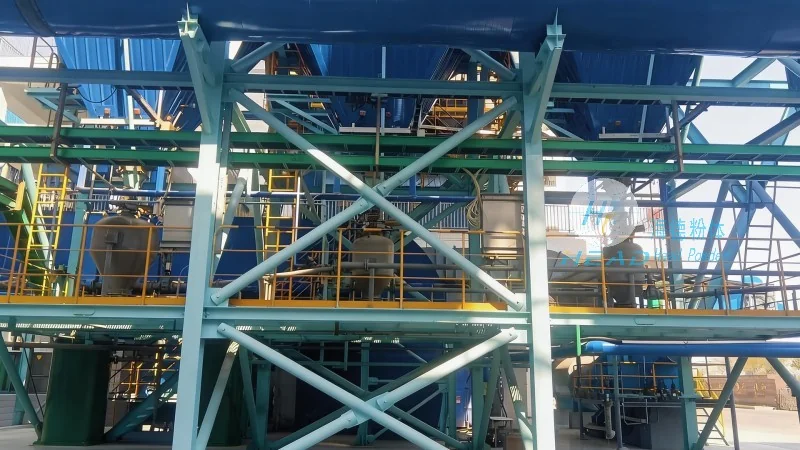
The dust-free automatic powder pneumatic conveying machine is widely used in various industries due to its versatility and effectiveness. In the pharmaceutical industry, it is employed to transport active pharmaceutical ingredients (APIs) and excipients with strict cleanliness requirements, ensuring that the final product remains free from contaminants. In the food processing sector, the machine is used to handle powders such as flour, sugar, and spices, maintaining the quality and safety of the food products. The chemical industry also benefits from this equipment, as it can transport sensitive chemicals and powders without compromising their integrity. Furthermore, the machine is utilized in the cosmetics industry to handle ingredients like pigments and powders, where color consistency and purity are essential. The adaptability of the dust-free automatic powder pneumatic conveying machine makes it a valuable asset across multiple sectors, providing a reliable solution for powder handling needs.
Conclusion and Company Information
In conclusion, the dust-free automatic powder pneumatic conveying machine is a sophisticated piece of equipment designed to address the challenges of efficient and clean powder transport in industrial settings. Its design principles, which emphasize airtightness, automation, and energy efficiency, make it a superior choice compared to traditional mechanical conveyors. By understanding how this machine operates and its advantages, businesses can make informed decisions about integrating it into their material handling processes. For those seeking a reliable and effective solution for powder conveying, Shandong HeadPowder Engineering Co., Ltd. offers high-quality dust-free automatic powder pneumatic conveying machines that meet the stringent requirements of modern industries. With a commitment to innovation and quality, HeadPowder provides equipment that enhances operational efficiency while maintaining the highest standards of cleanliness and safety.