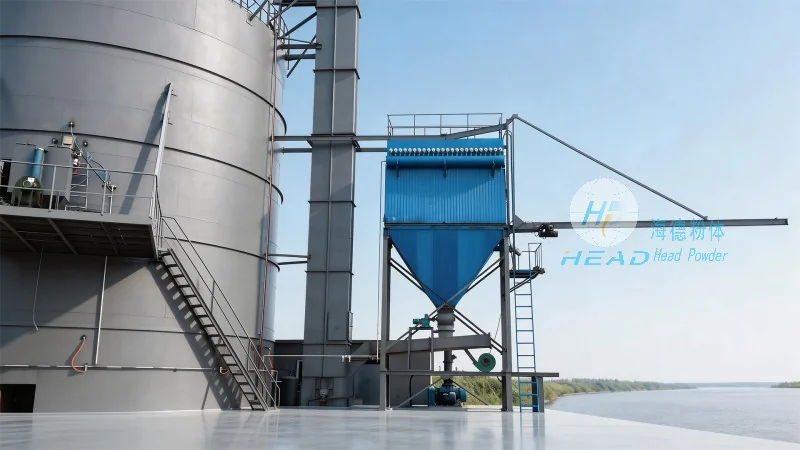
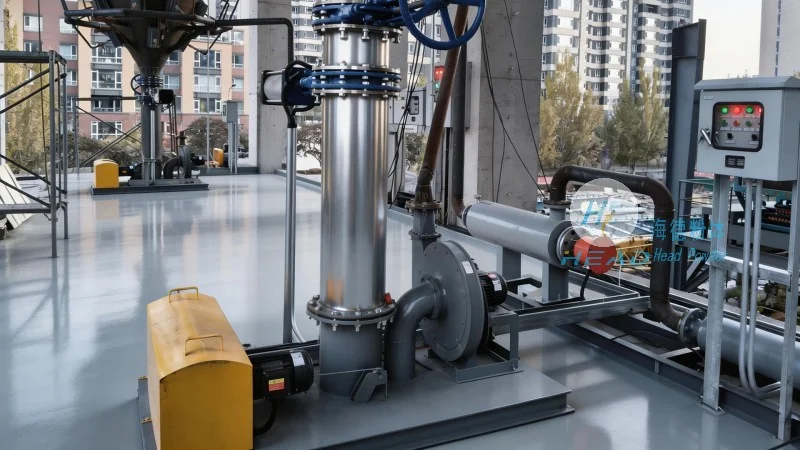
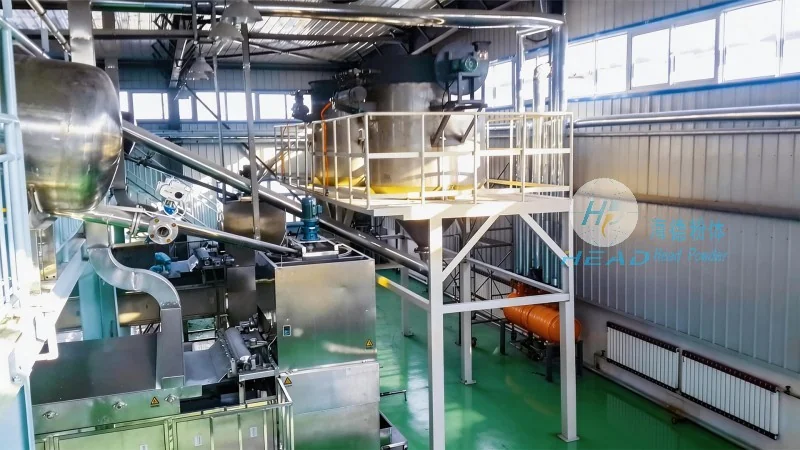
With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
In the realm of industrial material handling, the demand for efficient, clean, and reliable methods to transport powders and granular materials is paramount. Traditional mechanical conveying methods, such as screw conveyors or belt conveyors, often suffer from issues like dust leakage, high wear and tear, and maintenance complexities. To address these challenges, advanced technologies have emerged, with **pneumatic conveying systems** taking center stage. Among these, the **sealed batching pump** technology and **dilute phase positive pressure conveying** represent the pinnacle of modern engineering. These systems utilize air pressure to transport materials through pipelines, ensuring a sealed environment that protects both the product and the operator. Shandong Headpowder Engineering Co., Ltd. stands at the forefront of this technology, providing superior solutions for industries ranging from cement and power plants to chemical processing and food production.
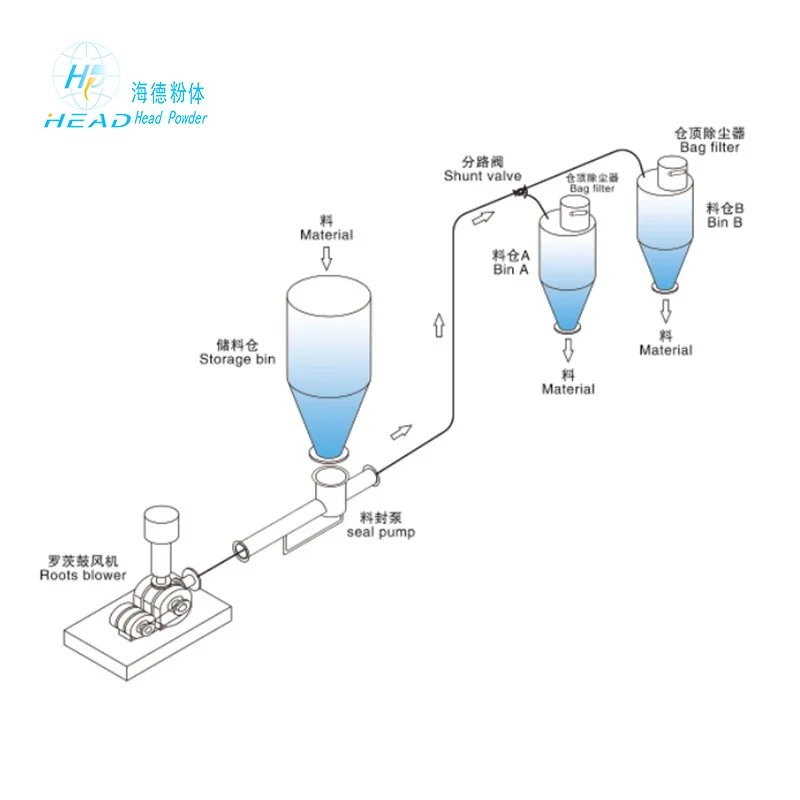
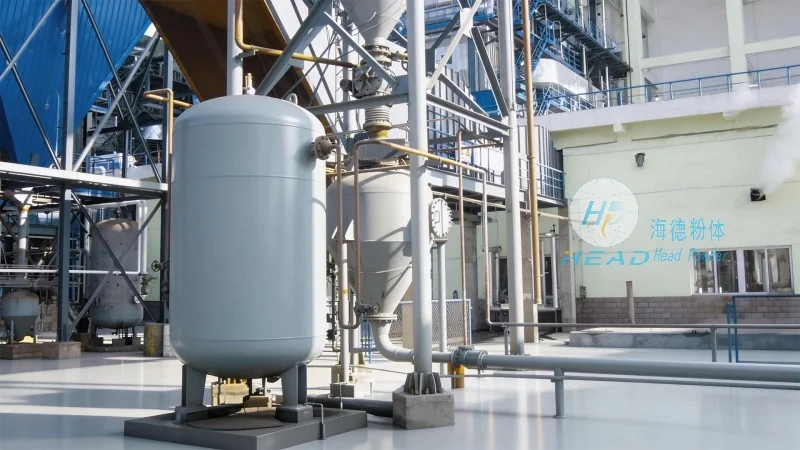
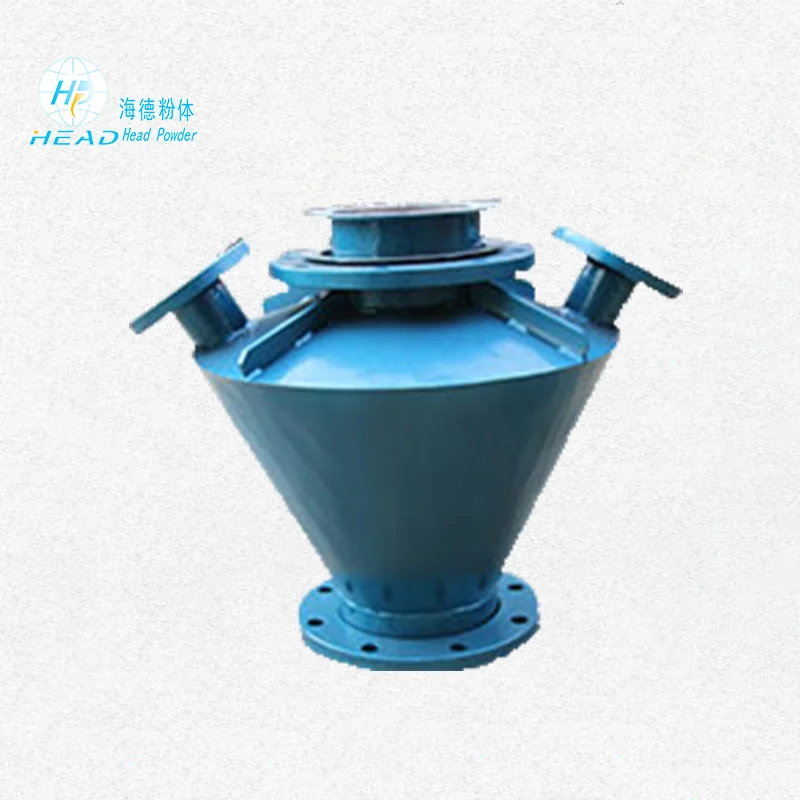
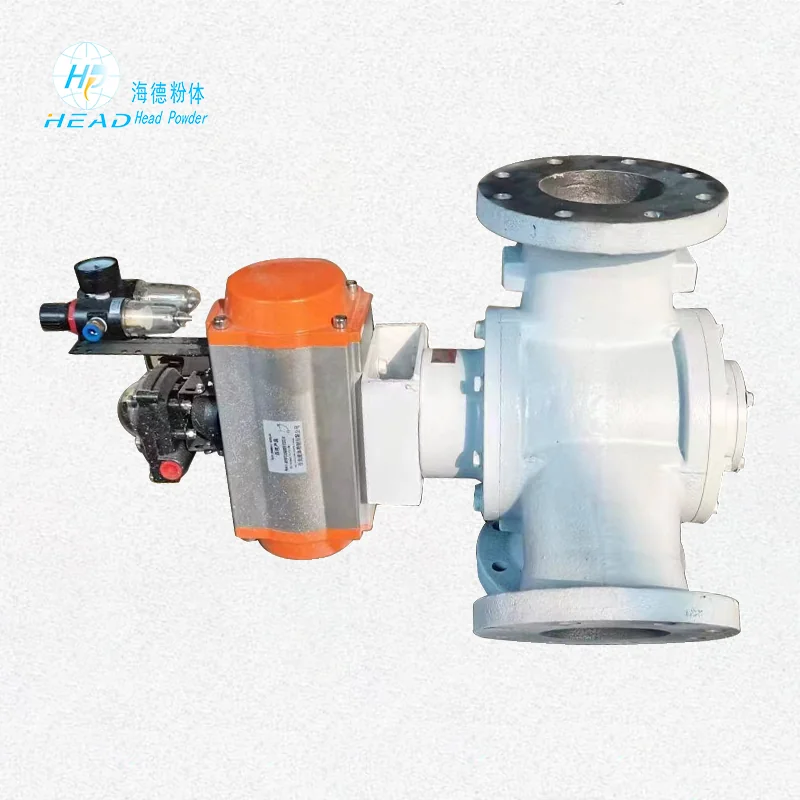
The core component of this advanced system is the **sealed batching pump**. Unlike traditional pumps that rely on complex mechanical seals and moving parts, a sealed batching pump operates on a simple yet effective principle. It functions by utilizing the weight of the material itself to maintain a stable flow. The pump creates a sealed chamber where compressed air is introduced to push the material out of the hopper and into the conveying pipeline. This design eliminates the need for traditional mechanical seals, which are prone to failure and leakage. Consequently, the maintenance requirements are significantly reduced, and the risk of dust pollution is virtually eliminated. The pump is designed to handle a wide range of materials, including fine powders and granular substances, ensuring versatility across different industrial applications.
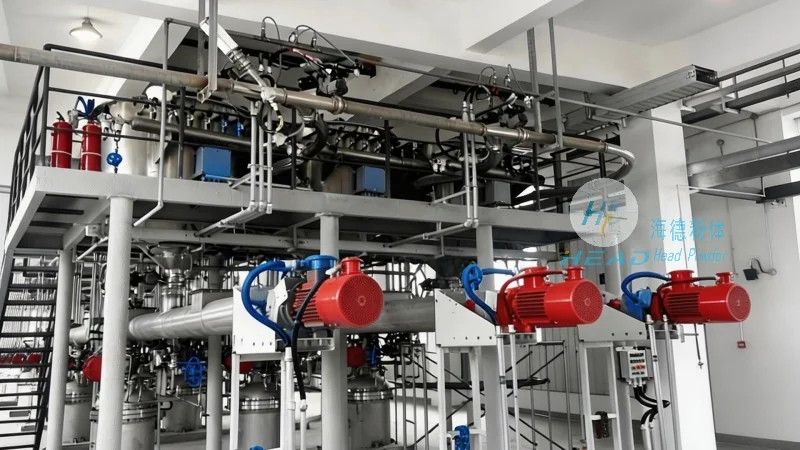
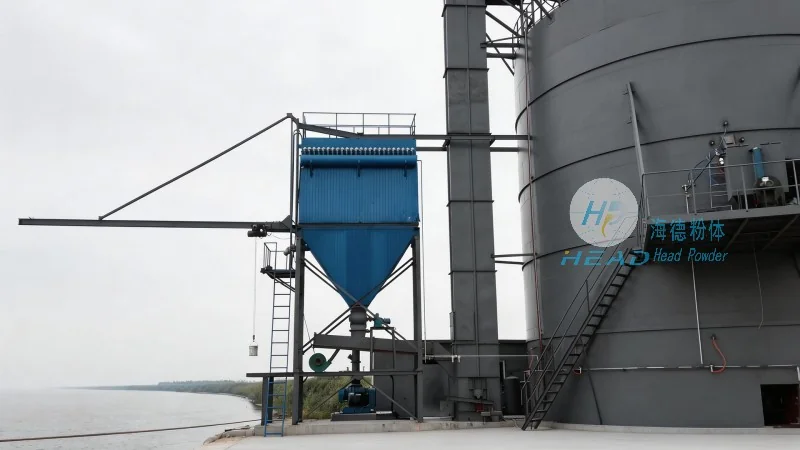
The **dilute phase positive pressure conveying** method is the operational standard for these systems. In a dilute phase system, the material and air mixture moves at a high velocity, creating a low-density flow. The "positive pressure" aspect indicates that the pressure within the pipeline is higher than atmospheric pressure. This pressure differential is what propels the material from the source (the pump) to the destination (the receiving hopper or silo). This method is particularly effective for long-distance transportation and complex pipeline layouts. Because the material is suspended in the air stream, the risk of material degradation is minimized, and the system can achieve high throughput rates. The efficiency of this method lies in its ability to maintain a consistent flow rate while minimizing energy consumption, making it an economically viable choice for large-scale operations.
One of the significant advantages of utilizing **pneumatic conveying systems** designed by expert manufacturers is the compatibility with diverse materials. Whether the requirement is to transport cement, fly ash, limestone, clay, or even food-grade powders, these systems can be customized to meet specific material properties. The **sealed batching pump** is engineered to handle materials with varying degrees of abrasiveness and moisture content. By adjusting the air pressure and flow rate, operators can optimize the system for specific materials, ensuring that the product remains in its intended state and quality is preserved throughout the transportation process. This versatility makes the system an indispensable asset in bulk material handling facilities.
As a leading **pneumatic conveying manufacturer**, Shandong Headpowder Engineering Co., Ltd. has dedicated itself to the research, development, and production of high-quality air handling equipment. Located in Shandong, China, the company leverages local manufacturing expertise combined with international engineering standards to deliver robust and efficient solutions. The company’s product portfolio is centered around the **sealed batching pump** and the **dilute phase positive pressure conveying** system, designed to meet the rigorous demands of modern industry. Their commitment to quality ensures that every unit is manufactured with precision, providing clients with reliable machinery that stands the test of time.
Operational efficiency is a critical metric for any industrial plant, and the design of the Shandong Headpowder system prioritizes this. The **sealed batching pump** features a streamlined design that reduces the number of moving parts, thereby minimizing wear and extending the equipment's lifespan. Routine maintenance is simplified to basic checks and cleaning, which reduces downtime and operational costs. Furthermore, the **dilute phase positive pressure conveying** system is designed for energy efficiency. By optimizing the air-to-material ratio, the system reduces the energy consumption required to move materials over long distances. This not only lowers utility bills but also reduces the carbon footprint of the facility, aligning with global sustainability goals.
For industries seeking a reliable solution for bulk material handling, the integration of a **sealed batching pump** and **dilute phase positive pressure conveying** system offers a superior alternative to traditional methods. These systems provide a clean, efficient, and cost-effective means of transporting powders and granules. Shandong Headpowder Engineering Co., Ltd. is proud to be the provider of these advanced solutions, combining technical expertise with customer-centric service. To discuss your specific material handling needs or to request a consultation, please contact Zhang Manager. You can reach Zhang Manager via WeChat at 15662777102 for professional support and detailed product information. Choosing the right partner for your pneumatic conveying needs is essential for long-term operational success, and Shandong Headpowder is dedicated to being that trusted partner.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top