

What is a Coal Ash Powder Pneumatic Conveying Equipment? And What Are Its Design Principles?
Coal ash, a byproduct of coal combustion in power plants, poses significant challenges in handling and transportation due to its fine particle size and potential for dust generation. To address these challenges, specialized equipment known as coal ash powder pneumatic conveying systems has been developed. These systems utilize air or gas to transport coal ash from one location to another, offering an efficient and safe solution for material handling in industrial settings.
Understanding Coal Ash Powder Pneumatic Conveying Equipment
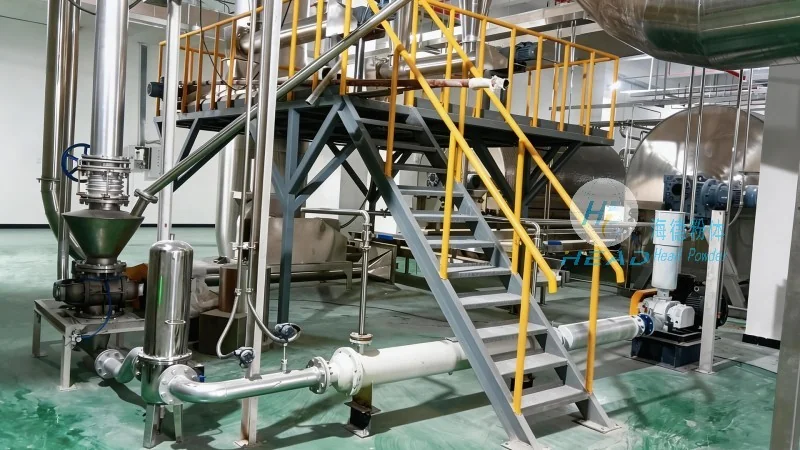
Coal ash powder pneumatic conveying equipment is a type of industrial machinery designed to transport coal ash, a fine particulate material, through a pipeline using compressed air or other gas as the conveying medium. This technology is particularly valuable in power generation facilities, where large volumes of coal ash need to be moved from the boiler to disposal sites or recycling facilities. The equipment is engineered to handle the unique properties of coal ash, including its low bulk density, high moisture content in some cases, and potential for dust explosion risks, ensuring safe and efficient operation.
Key Components of the Pneumatic Conveying System
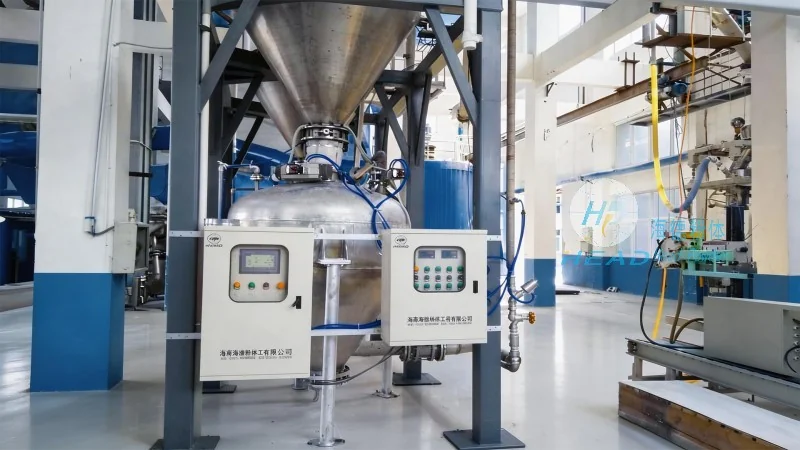
The coal ash powder pneumatic conveying system typically consists of several critical components that work in tandem to achieve effective material transport. These components include a dust collector or feeder to introduce the coal ash into the system, a conveying pipeline that transports the material, a blower or compressor to generate the necessary air pressure, and a receiver or discharge unit where the coal ash is deposited. Each component plays a vital role in maintaining the system's efficiency and safety. For instance, the feeder ensures a consistent flow of coal ash into the pipeline, while the blower provides the pressure differential required to move the material. The pipeline design, often using flexible or rigid tubing depending on the application, must be able to withstand the pressure and temperature conditions of the conveying process.
Design Principles for Efficient Coal Ash Transport
The design of coal ash powder pneumatic conveying equipment is guided by several key principles aimed at optimizing performance, safety, and cost-effectiveness. One of the primary design considerations is the selection of the appropriate conveying method—either dilute phase or dense phase—based on the characteristics of the coal ash and the distance it needs to be transported. Dilute phase systems use low air-to-material ratios and are suitable for short to medium distances, while dense phase systems employ higher air-to-material ratios and are ideal for longer distances or when handling more abrasive materials. The system's design also incorporates features to minimize dust emissions and prevent material degradation. This includes the use of sealed feeders and discharge units, as well as filtration systems to capture any airborne particles. Additionally, the equipment is designed to handle variations in coal ash properties, such as changes in moisture content or particle size, ensuring consistent performance over time.
Operational Considerations and Maintenance
Proper operation and regular maintenance are essential for the reliable performance of coal ash powder pneumatic conveying equipment. Operators must follow established procedures for starting and stopping the system, including pre-start checks to ensure all components are functioning correctly and that the pipeline is free of blockages. Regular maintenance tasks include cleaning the dust collector and feeder, inspecting the blower and compressor for wear, and checking the pipeline for signs of wear or damage. These maintenance activities help to prevent system failures and extend the lifespan of the equipment. Furthermore, the system is designed with safety features such as pressure relief valves and dust explosion suppression systems to mitigate risks associated with the handling of coal ash. These features are critical in ensuring the safety of personnel and the integrity of the equipment during operation.
Applications and Benefits of Coal Ash Powder Pneumatic Conveying
Coal ash powder pneumatic conveying equipment is widely used in various industrial applications, particularly in the power generation sector. Its primary benefits include the ability to transport coal ash over long distances without the need for traditional trucks or conveyor belts, which can be more cost-effective and environmentally friendly. The equipment also reduces the risk of dust exposure for workers and minimizes the environmental impact of coal ash disposal by ensuring that the material is contained and transported safely. Additionally, the system can be integrated with other processes, such as coal ash recycling or utilization, to enhance overall plant efficiency. By leveraging the principles of pneumatic conveying, facilities can achieve more efficient and sustainable handling of coal ash, contributing to both operational and environmental goals.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of industrial powder handling equipment, including coal ash powder pneumatic conveying systems. With years of experience in the industry, HeadPowder specializes in designing and manufacturing equipment tailored to the unique needs of power plants and other industrial facilities. The company's products are known for their reliability, efficiency, and adherence to safety standards. HeadPowder's commitment to quality and customer satisfaction has made it a trusted partner for facilities seeking to improve their coal ash handling processes. The company's headquarters is located in Shandong, China, where it continues to innovate and develop new solutions for the evolving needs of the industrial sector.