With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Glucose material handling conveyors are specialized industrial systems designed to transport glucose, a critical sweetener and energy source, efficiently and safely within processing facilities. These conveyors play a vital role in the food and beverage industry, pharmaceutical manufacturing, and other sectors where glucose is processed or used as an ingredient. Understanding the components, operational mechanisms, and design principles of such conveyors is essential for optimizing production workflows and ensuring product quality.
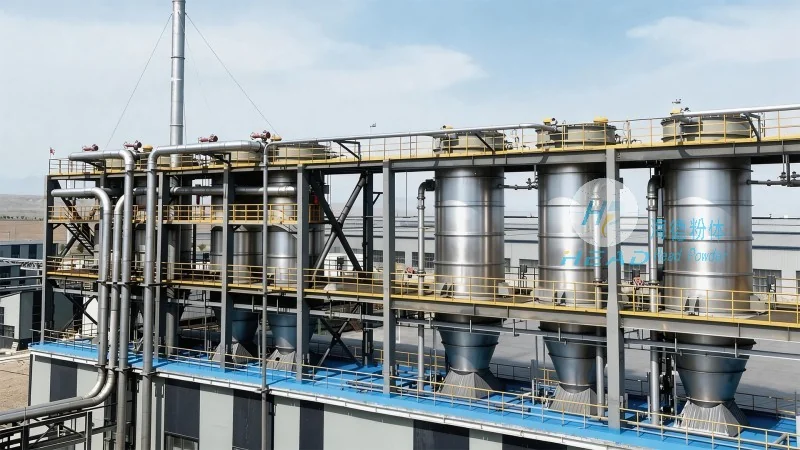
The core components of a glucose material handling conveyor typically include feeding mechanisms, conveyor belts or rollers, control systems, and material handling accessories. The feeding mechanism, often a hopper or feeder, ensures a consistent flow of glucose into the conveyor system. Conveyor belts, commonly made from food-grade materials like stainless steel or polyurethane, are designed to handle the granular or powdered nature of glucose without contamination. Control systems, including sensors and variable frequency drives (VFDs), regulate the speed and direction of the conveyor, allowing for precise material movement. Additionally, accessories such as dividers, elevators, and discharge chutes may be integrated to manage the flow and orientation of the glucose during transport.
The design of glucose material handling conveyors adheres to several key principles to ensure optimal performance. Firstly, hygienic design is paramount, as glucose is used in food and pharmaceutical applications where contamination must be minimized. Materials used in construction, such as stainless steel and food-grade plastics, are non-porous and easy to clean, reducing the risk of bacterial growth. Secondly, the conveyor system is engineered for gentle handling of the material to prevent degradation or clumping. This is achieved through smooth surfaces and minimal impact points, ensuring the glucose remains in its desired form. Thirdly, the system is designed for scalability and adaptability, allowing it to accommodate varying production volumes and processing requirements. This flexibility is crucial for meeting the dynamic needs of modern manufacturing environments.
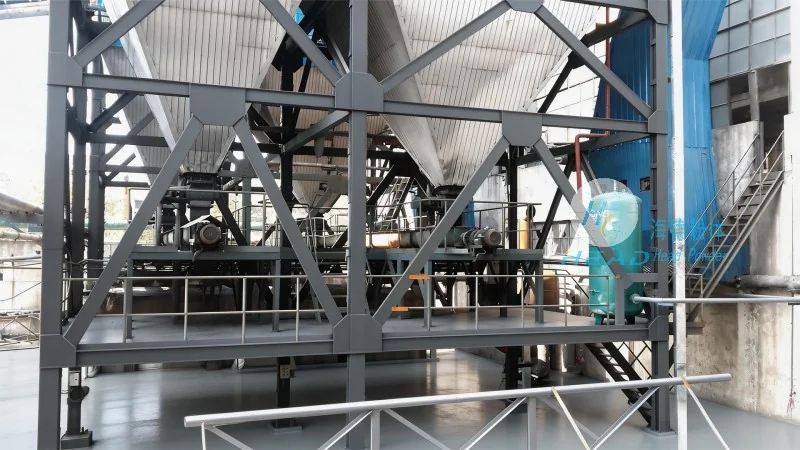
Operational efficiency and longevity of glucose material handling conveyors depend on proper maintenance and adherence to operational guidelines. Regular cleaning and sanitation are critical to maintain hygiene standards, as glucose can attract moisture and microbial growth. The conveyor components, particularly the belts and rollers, require periodic inspection to detect wear and tear, which can affect performance and product quality. Additionally, the control systems should be calibrated regularly to ensure precise control over the conveyor speed and flow. Proper training for operators on the safe and efficient use of the conveyor system is also essential to prevent accidents and downtime.
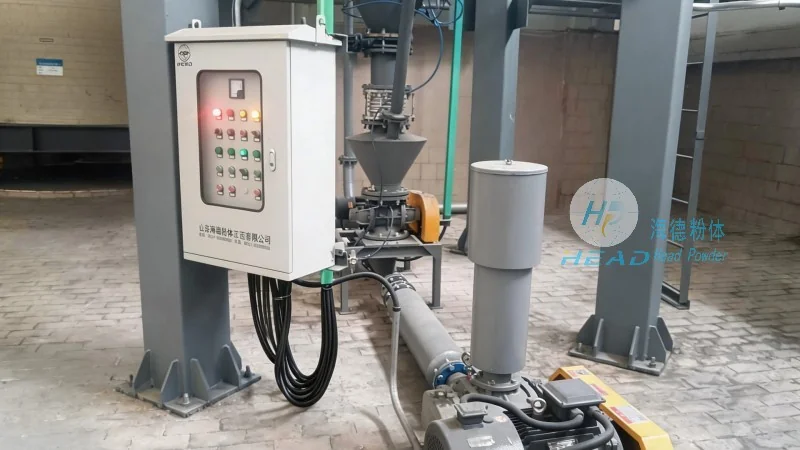
Glucose material handling conveyors are widely used in various stages of glucose processing, from raw material intake to finished product packaging. In the initial stages, conveyors transport raw glucose from storage silos or bulk containers to processing equipment. During the processing phase, conveyors may be used to move glucose through mixing, drying, or crystallization units. In the final stages, conveyors transport the finished glucose product to packaging lines or storage areas. The versatility of these systems allows them to integrate seamlessly with other processing equipment, enhancing overall production efficiency.
Glucose material handling conveyors are indispensable components in the glucose processing industry, providing efficient, hygienic, and reliable transport of glucose. By adhering to design principles that prioritize material integrity, hygiene, and scalability, these systems ensure optimal performance and product quality. For businesses operating in the glucose sector, investing in high-quality material handling conveyors is a strategic decision that enhances operational efficiency and supports long-term success. Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in designing and manufacturing such conveyors, offering tailored solutions to meet the specific needs of their clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top