With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced air-flow conveying systems for salt handling applications. The principle of salt air-flow conveying equipment is centered on the efficient transport of granular materials like salt through a pipeline using compressed air. This method offers significant advantages over traditional mechanical conveying systems, including reduced maintenance costs, lower energy consumption, and enhanced safety in handling potentially hazardous materials.
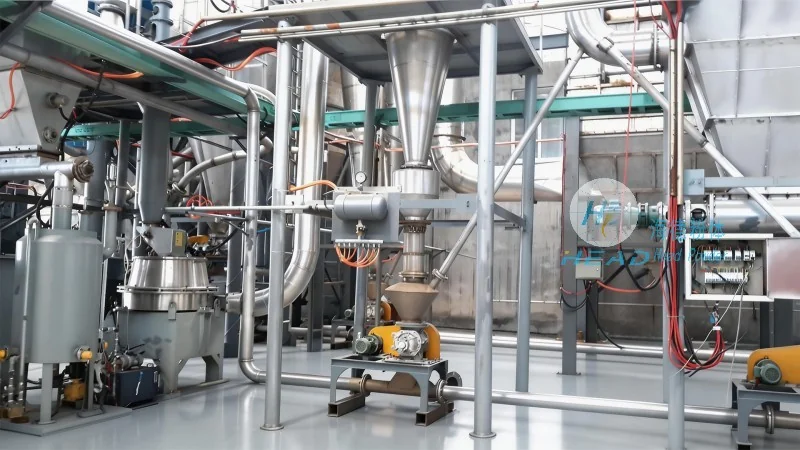
The air-flow conveying system for salt typically consists of several key components: a hopper for material storage, a rotary valve or feeder to control the flow of salt into the pipeline, a venturi or air nozzle to create the necessary air flow, and a receiver or silo for the discharged material. The working principle involves feeding salt into the hopper, where it is then metered by the feeder and mixed with high-pressure air. The air-salt mixture travels through the pipeline under pressure, and upon reaching the receiver, the air is separated from the salt, allowing the material to be deposited in the desired location. This process is highly efficient for transporting large volumes of salt over moderate distances, making it ideal for industrial and commercial salt processing facilities.
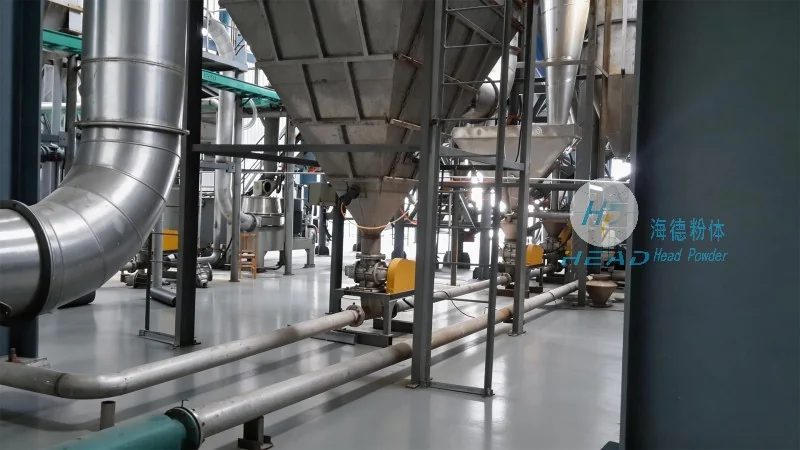
Compared to traditional methods such as belt conveyors or bucket elevators, air-flow conveying offers several key benefits for salt handling. Firstly, it eliminates the need for moving parts in contact with the material, reducing wear and tear and minimizing the risk of contamination. Secondly, the system is highly flexible, allowing for changes in conveying direction or distance without significant modifications. Thirdly, it can handle a wide range of salt types, including fine powders and coarse granules, with consistent performance. Additionally, the air-flow system is more energy-efficient, as it requires less power to transport the same volume of material compared to mechanical systems. These advantages make air-flow conveying a preferred choice for many salt processing operations.
HeadPowder's salt air-flow conveying equipment is widely used in various applications within the salt industry. In salt production facilities, the system is used to transport raw salt from storage silos to processing units, such as crushers or classifiers. In salt processing plants, it can convey processed salt to packaging lines or storage areas. Additionally, the equipment is suitable for transporting salt in salt mines or quarries, where it is extracted from the ground and transported to processing facilities. The versatility of the air-flow system allows it to be adapted to different production scales, from small-scale operations to large industrial plants. By optimizing the conveying process, HeadPowder's equipment helps clients improve operational efficiency and reduce overall costs in their salt handling operations.
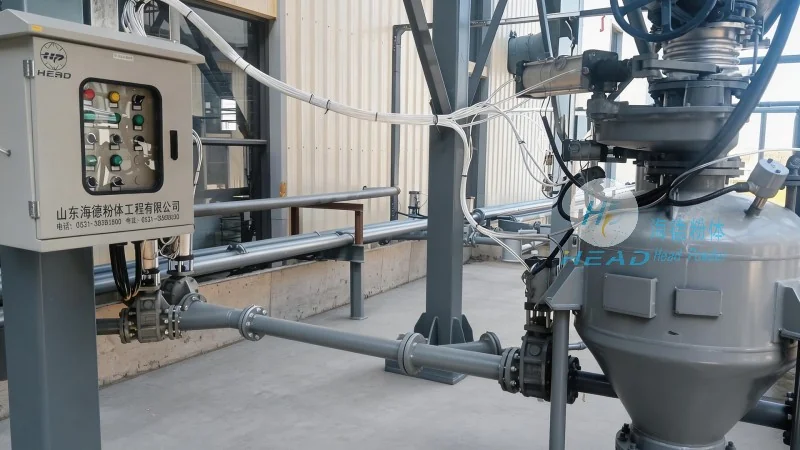
HeadPowder understands that each salt handling application has unique requirements. Therefore, the company offers customized air-flow conveying solutions tailored to specific client needs. Whether it's adjusting the conveying capacity, modifying the pipeline layout, or integrating with existing equipment, HeadPowder's engineering team works closely with clients to develop the most suitable solution. The company also provides comprehensive technical support, including installation guidance, maintenance training, and troubleshooting assistance. This ensures that clients can maximize the performance and lifespan of their salt air-flow conveying equipment. With a focus on quality and customer satisfaction, HeadPowder aims to deliver reliable and efficient conveying solutions for the salt industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top