With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industries dealing with dye powders and other fine or granular materials, efficient material handling is crucial for maintaining production efficiency and product quality. Pneumatic conveying systems offer a solution that leverages air flow to transport these materials with precision and control. This article explores the principles and applications of dye pneumatic conveying, highlighting how companies like Shandong HeadPowder Engineering Co., Ltd. utilize advanced technology to optimize material transport processes.
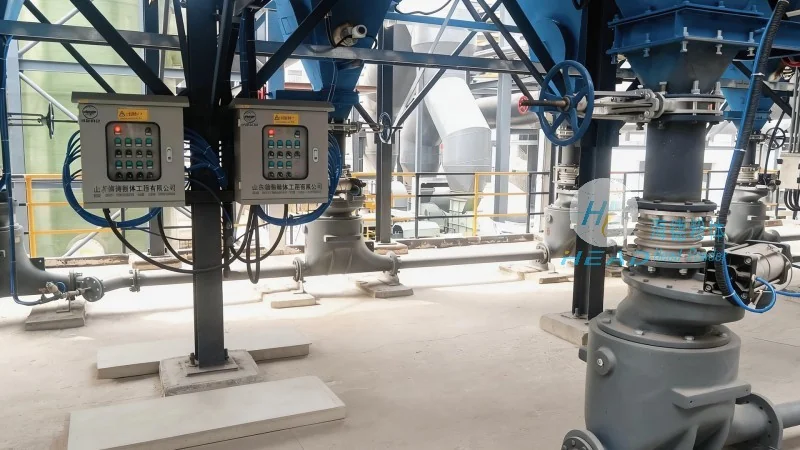
Pneumatic conveying, also known as air conveying, is a method that uses compressed air or other gases to move bulk materials through a pipeline system. In the context of dye handling, this technology is particularly valuable due to the sensitivity of dye powders to moisture, contamination, and degradation. The system typically consists of a hopper for material storage, a conveying line, and a receiver for the material's final destination. The air flow can be either positive pressure (where air pushes the material) or negative pressure (where air pulls the material), each with its own advantages depending on the application and material characteristics.
Several critical components work together to ensure the smooth operation of a pneumatic conveying system for dyes. These include: the material hopper, which holds the dye powder and provides a controlled feed; the air compressor or blower, which generates the necessary air pressure; the conveying line, which transports the material; and the filter and separator, which remove dust and particles from the air before it is released back into the environment. Each component must be carefully selected and maintained to ensure the system operates efficiently and safely. For example, the hopper may be equipped with a rotary valve or feeder to regulate the flow of dye powder, preventing clogging and ensuring a consistent feed rate. The air compressor must be capable of delivering the required pressure and volume to move the material through the pipeline without excessive energy consumption.
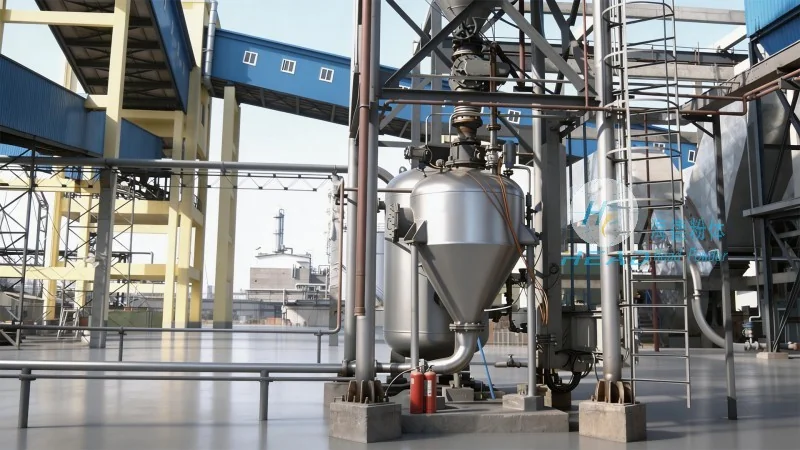
Compared to traditional methods like belt conveyors or manual handling, pneumatic conveying offers several advantages for dye processing. First, it provides a closed system that protects the dye from moisture, dust, and contamination, which is essential for maintaining the color quality and stability of the product. Second, it allows for precise control over the material flow rate and pressure, enabling manufacturers to adjust the system according to production needs. Third, it reduces labor costs and operational risks by automating the material transport process. Additionally, pneumatic conveying can handle a wide range of material sizes and densities, making it suitable for various dye formulations. The system also minimizes product degradation due to reduced exposure to air and mechanical stress, which is critical for high-value dyes used in textiles and other industries.
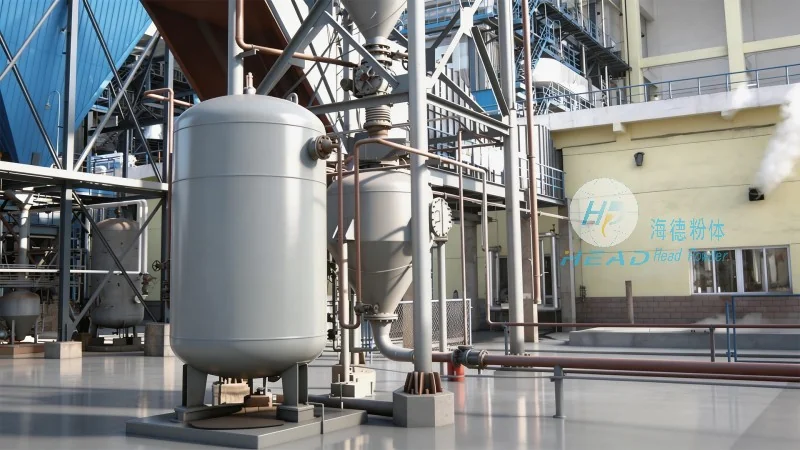
The applications of pneumatic conveying in the dye industry are diverse and widespread. In textile manufacturing, for example, dye powders are often transported from storage silos to mixing and dyeing machines. Pneumatic systems allow for the rapid and accurate delivery of the required dye quantities, ensuring consistent color results across batches. In chemical manufacturing, dyes are transported from production lines to storage facilities or to other processing units. The closed system prevents cross-contamination and maintains the purity of the materials. Additionally, in research and development labs, small-scale pneumatic conveyors are used to handle experimental dye samples, providing flexibility and precision in material handling.
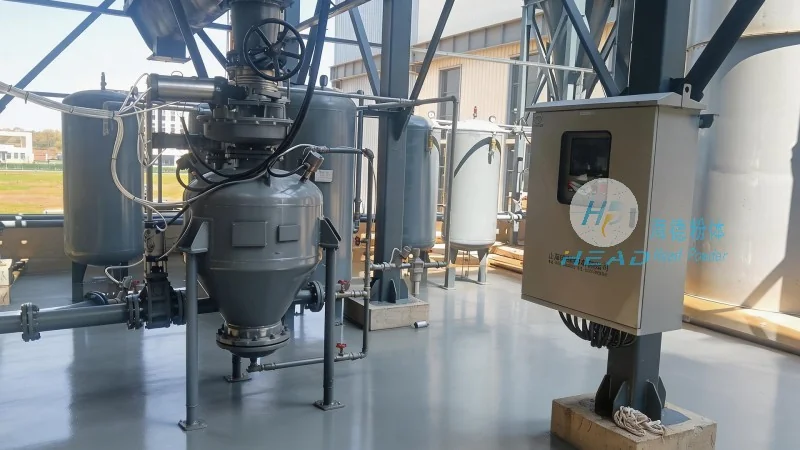
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing pneumatic conveying systems tailored to the needs of the dye industry. The company, commonly referred to as HeadPowder, has extensive experience in working with various dye formulations and production environments. Their systems are engineered to meet the specific requirements of each client, ensuring optimal performance and reliability. For instance, a client in the textile industry might require a high-capacity positive pressure system to transport large quantities of dye powders quickly and efficiently. HeadPowder's engineers would assess the material characteristics, such as particle size and moisture content, and design a system with the appropriate air pressure and line diameter to achieve the desired throughput. The company also provides maintenance and support services to ensure the longevity and efficiency of the installed systems, helping clients maintain consistent production and product quality.
Pneumatic conveying remains a vital technology for efficiently handling dye powders and other fine materials in the modern industrial landscape. As the demand for high-quality dyes continues to grow, the need for reliable and efficient material transport systems becomes increasingly important. Companies like Shandong HeadPowder Engineering Co., Ltd. play a crucial role in advancing this technology by developing innovative solutions that meet the evolving needs of the industry. By leveraging the principles of pneumatic conveying, manufacturers can enhance their production processes, reduce costs, and improve product quality, ultimately contributing to the success of their operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top