With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for the efficient handling of potassium carbonate fertilizer. This article provides a comprehensive overview of such systems, highlighting their operational principles, key components, and practical applications in the fertilizer industry.
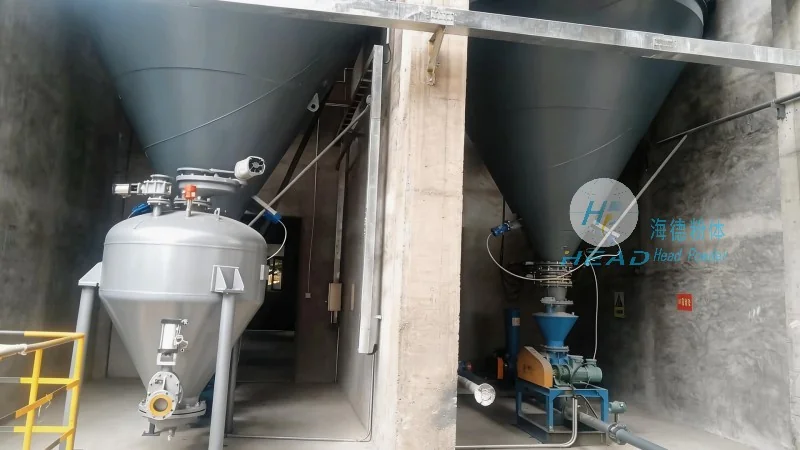
Pneumatic conveying systems are essential for the safe and efficient transport of bulk materials like potassium carbonate fertilizer from storage silos to processing or packaging units. These systems utilize air or gas as the conveying medium, enabling the material to be moved through pipelines without the need for mechanical components like belts or buckets. The primary advantage of pneumatic conveying is its ability to handle fine or dusty materials, such as potassium carbonate, while minimizing product degradation and contamination.
The effectiveness of a pneumatic conveying system for potassium carbonate fertilizer relies on several critical components working in harmony. These include:
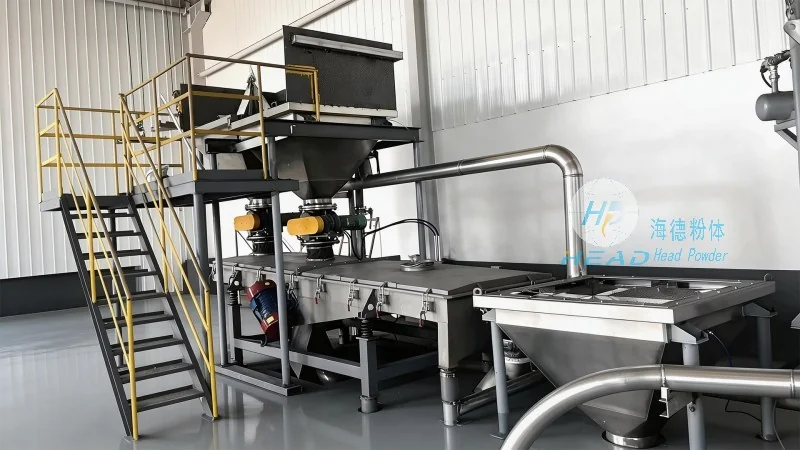
The operation of a pneumatic conveying system for potassium carbonate fertilizer involves several stages. Initially, the fertilizer is discharged from the feed hopper into the pipeline via the rotary valve. Simultaneously, the compressor supplies compressed air, which mixes with the fertilizer particles, creating a slurry-like mixture. This mixture is then propelled through the pipeline to the receiving hopper at the destination. The air and fertilizer are separated at the receiving end, with the air being recirculated back to the compressor or released safely.
Efficiency in these systems is measured by factors such as conveying capacity, energy consumption, and material handling speed. Advanced systems often incorporate features like variable speed drives for the blower, which adjust air pressure based on the material flow, optimizing energy use. Additionally, the use of high-efficiency cyclones and filters minimizes air loss and ensures that the fertilizer is collected with minimal dust, improving overall system performance and product quality.
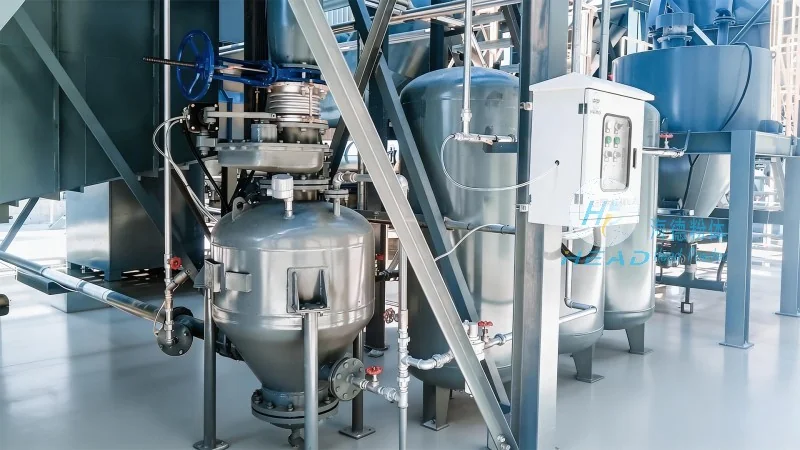
Potassium carbonate fertilizer pneumatic conveying systems are widely used in fertilizer production and distribution facilities. They are particularly beneficial in processes where the fertilizer needs to be transferred between multiple stages, such as from raw material storage to blending, or from blending to packaging. The systems offer several advantages over traditional mechanical conveying methods:
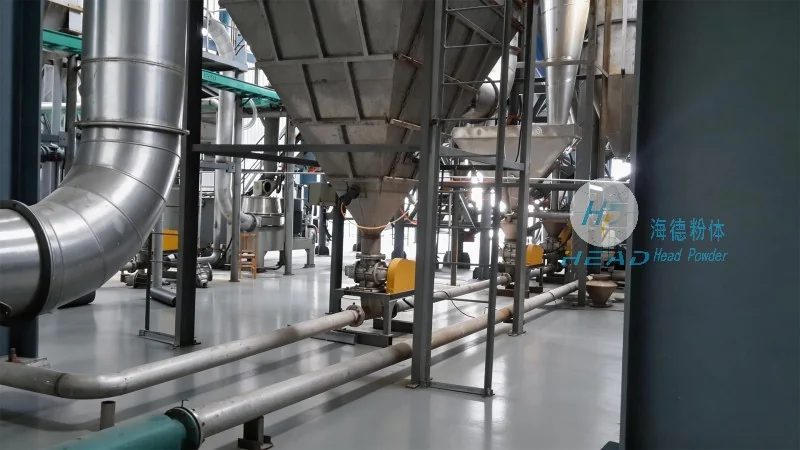
HeadPowder, with its expertise in engineering, offers customized pneumatic conveying solutions tailored to the specific needs of fertilizer plants. The company's team of engineers works closely with clients to assess their current infrastructure, material characteristics, and operational requirements to design a system that maximizes efficiency and minimizes costs. Customization may include adjustments to pipeline length, diameter, or the type of compressor, as well as integration with existing control systems or silos.
For facilities in Shandong, China, HeadPowder leverages its local presence and understanding of regional regulations and market demands to provide solutions that align with both operational and compliance needs. The company's commitment to quality and customer satisfaction ensures that the installed systems meet or exceed industry standards, providing reliable and long-lasting performance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top