With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading manufacturer based in Shandong, China, specializes in advanced pneumatic conveying solutions. The intelligent centralized pneumatic conveying system is a sophisticated piece of equipment designed to efficiently transport bulk materials over long distances with minimal human intervention. This system integrates cutting-edge technology to ensure reliable and efficient material handling, making it ideal for various industrial applications.
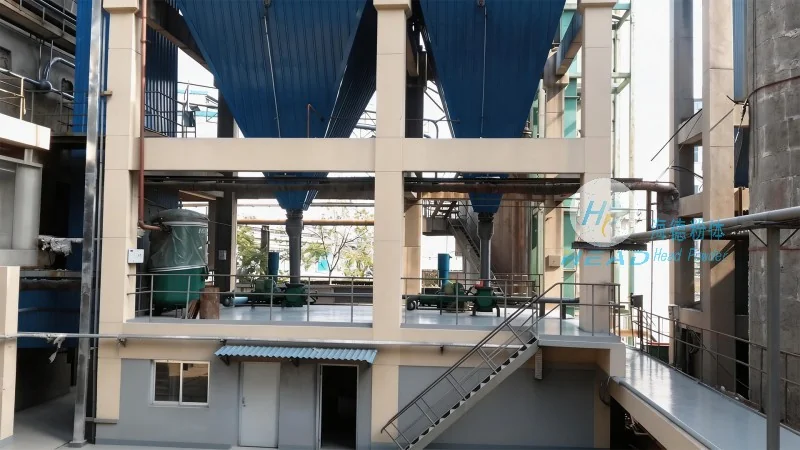
HeadPowder Engineering Co., Ltd. is a professional enterprise dedicated to the research, development, and production of pneumatic conveying systems. With a strong focus on innovation and quality, the company has established itself as a trusted provider in the industry. HeadPowder's commitment to excellence is reflected in its state-of-the-art manufacturing facilities and rigorous quality control processes, ensuring that each product meets the highest standards of performance and durability.
The intelligent centralized pneumatic conveying system is a versatile and efficient solution for transporting dry bulk materials such as powders, granules, and fine particles. Unlike traditional conveying methods, this system utilizes compressed air to move materials through a network of pipes, eliminating the need for mechanical components like belts or buckets. The centralization aspect allows for a unified control system, enabling seamless coordination between multiple feeding and discharge points.
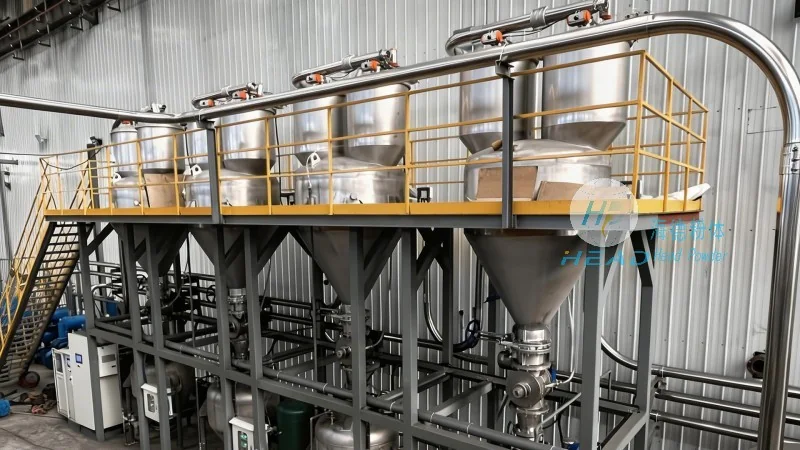
The intelligent centralized pneumatic conveying system comprises several critical components, each playing a vital role in the overall operation. These include the air compressor, which generates the necessary pressure to move materials; the material feeders, which introduce the bulk material into the system; the conveying pipes, which transport the material from the source to the destination; and the control unit, which manages the entire process. Additionally, the system may feature sensors and monitoring devices to provide real-time data on pressure, flow rate, and material level, enhancing operational efficiency and safety.
The operation of the intelligent centralized pneumatic conveying system follows a systematic sequence to ensure smooth material transport. Initially, the air compressor is activated, generating compressed air that fills the conveying pipes. Simultaneously, the material feeder is engaged, feeding the bulk material into the system. As the compressed air flows through the pipes, it creates a pressure differential that propels the material forward. The material is then transported to the designated discharge point, where it is released under controlled conditions. The control unit continuously monitors the system parameters, adjusting the air pressure and flow rate as needed to maintain optimal performance. This automated process minimizes human intervention, reducing operational costs and improving overall efficiency.
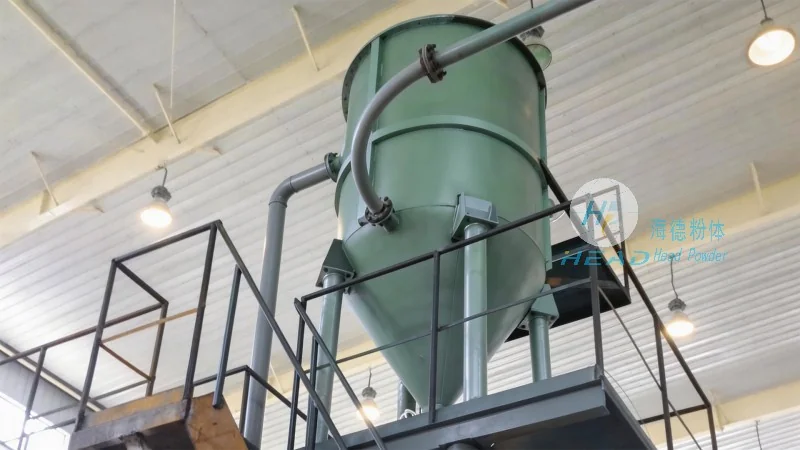
The working principle of the intelligent centralized pneumatic conveying system is based on the fundamental concept of pneumatic transport. Compressed air is used to create a flow of air and material within the conveying pipes. The air acts as a carrier, carrying the bulk material particles along the pipe network. The system operates under either positive or negative pressure, depending on the specific application requirements. Positive pressure systems use compressed air to push the material forward, while negative pressure systems use vacuum to draw the material into the system. The intelligent control system optimizes the pressure and flow rates to ensure that the material is transported efficiently without causing blockages or excessive wear on the equipment. This principle allows for the reliable and consistent transport of materials over long distances, making it suitable for various industrial settings.
The intelligent centralized pneumatic conveying system offers numerous advantages over traditional conveying methods. One of the primary benefits is its ability to transport materials over long distances with minimal energy consumption. The system also eliminates the need for mechanical components, reducing maintenance requirements and operational downtime. Additionally, the centralized control system provides real-time monitoring and data analysis, enabling proactive maintenance and troubleshooting. The system is also highly flexible, allowing for easy integration with existing industrial processes and expansion as needed. Furthermore, the use of compressed air ensures that the material is handled gently, preserving its quality and preventing contamination. These advantages make the intelligent centralized pneumatic conveying system an ideal choice for industries requiring efficient, reliable, and cost-effective material transport solutions.
The intelligent centralized pneumatic conveying system is widely used in various industries due to its versatility and efficiency. It is commonly employed in the chemical, pharmaceutical, food, and cement industries, where the transport of dry bulk materials is essential. In the chemical industry, the system is used to transport powders and granules for processing and packaging. In the pharmaceutical industry, the system ensures the safe and hygienic transport of raw materials and finished products. The food industry utilizes the system for transporting ingredients and products, maintaining strict sanitary standards. The cement industry benefits from the system's ability to transport large quantities of raw materials over long distances, improving production efficiency. These applications highlight the system's adaptability and reliability in diverse industrial environments.
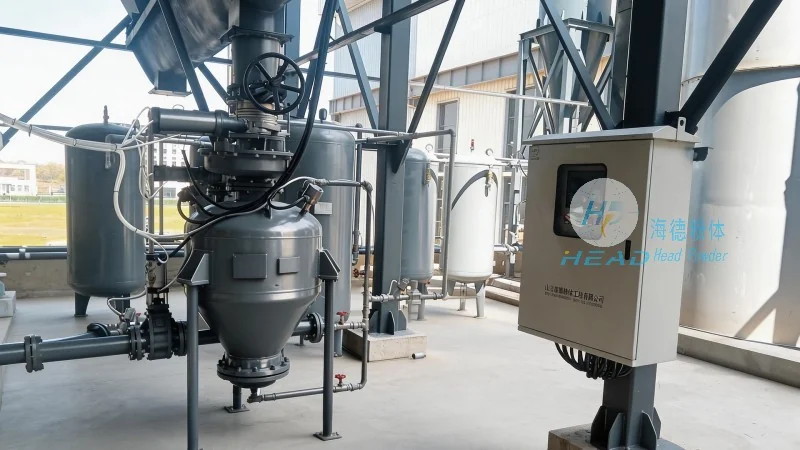
Maintaining the intelligent centralized pneumatic conveying system is crucial to ensure its long-term performance and reliability. Regular maintenance procedures include checking the air compressor for proper operation, inspecting the conveying pipes for blockages or leaks, and cleaning the material feeders and discharge points. The control unit should be monitored regularly to ensure that all sensors and monitoring devices are functioning correctly. If issues arise, such as material blockages or pressure fluctuations, the system's troubleshooting guide should be consulted. The guide provides step-by-step instructions for identifying and resolving common problems, minimizing downtime and ensuring the system operates at optimal levels. Proper maintenance and timely troubleshooting are essential to maximize the system's lifespan and performance.
The intelligent centralized pneumatic conveying system is a sophisticated and efficient solution for transporting bulk materials in various industrial applications. With its advanced technology and centralized control system, the system offers numerous benefits, including reduced energy consumption, minimal maintenance, and improved operational efficiency. HeadPowder Engineering Co., Ltd. continues to innovate and refine its pneumatic conveying systems, ensuring that clients receive high-quality, reliable equipment that meets their specific needs. As the demand for efficient material transport solutions grows, the intelligent centralized pneumatic conveying system remains a top choice for industries seeking to optimize their production processes and enhance overall productivity.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top