

Principle and Working Scene Characteristics of Manganese Carbonate Pneumatic Conveying System Equipm
HeadPowder, a professional engineering company based in Shandong, China, specializes in the design and manufacturing of advanced pneumatic conveying systems tailored for the handling of manganese carbonate. The company's facilities are located in Shandong, China, and it operates under the brand name headpowder, offering comprehensive solutions for material transport in industrial settings.
Principle of Manganese Carbonate Pneumatic Conveying Systems
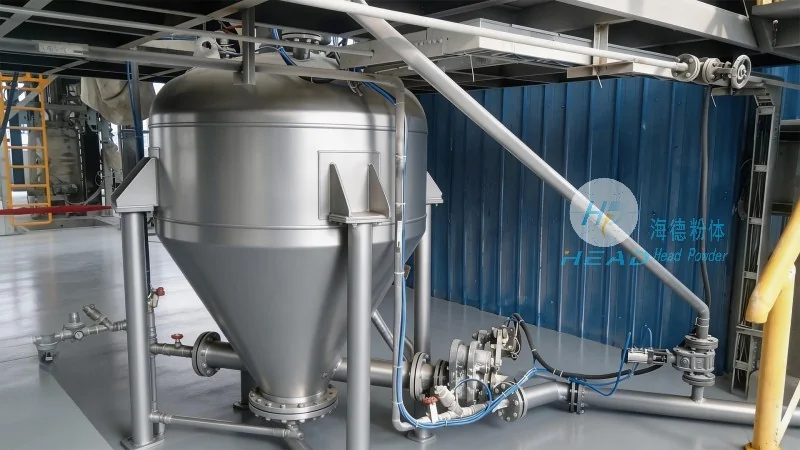
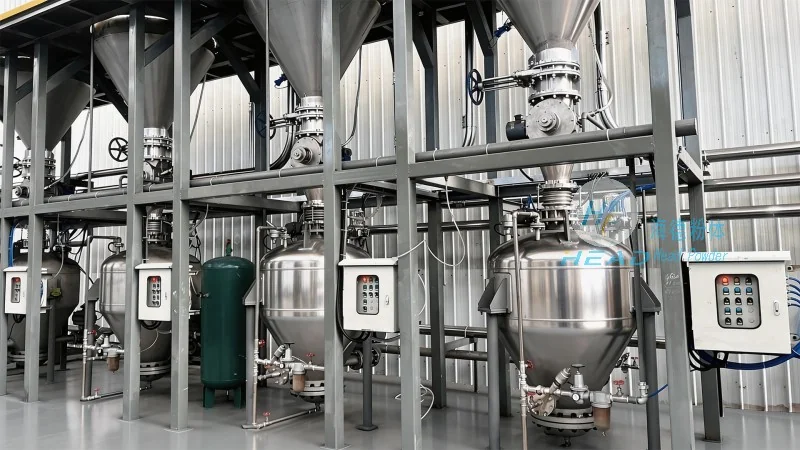
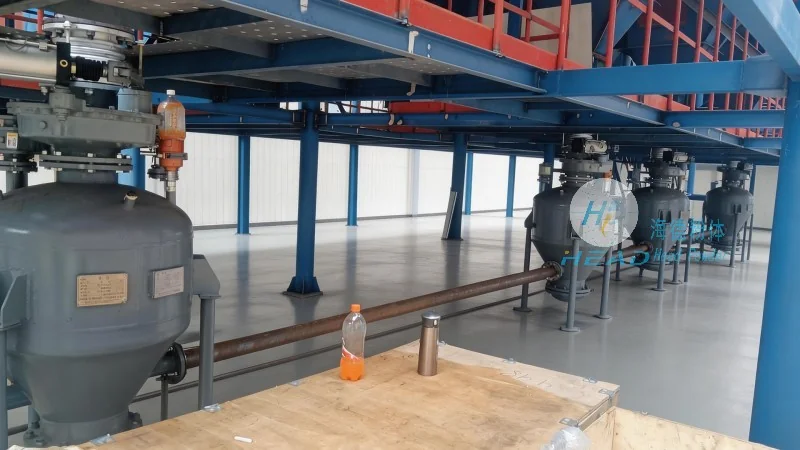
Manganese carbonate pneumatic conveying systems operate on the fundamental principle of transporting solid particles through a pipeline using a stream of air or other gas. This method, known as pneumatic conveying, eliminates the need for mechanical components like belts or buckets, reducing friction and wear while enabling efficient material movement. The system typically consists of several key components: a feeder to introduce the manganese carbonate into the air stream, a conveying line to transport the material, a separator to separate the material from the air, and a receiver to collect the final product. The air velocity and pressure within the system are carefully controlled to ensure the material is carried efficiently without causing excessive pressure drops or material degradation. For manganese carbonate, which is a fine powder with specific bulk properties, the system design must account for factors such as particle size, density, and moisture content to maintain stable and reliable operation.
Working Scene Characteristics and Applications
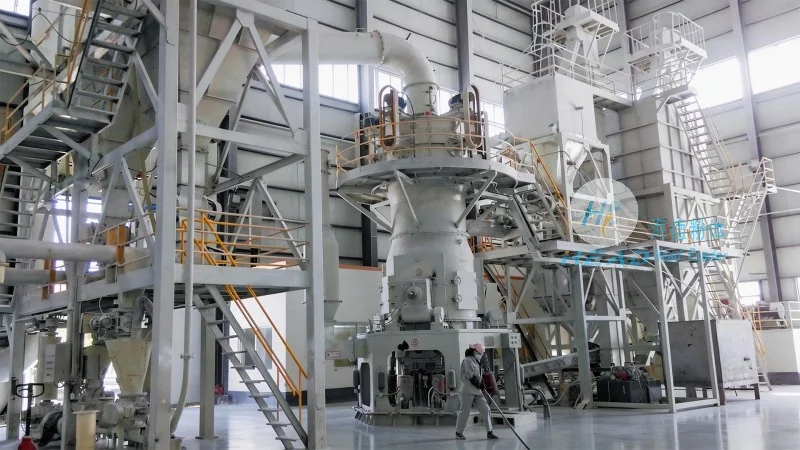
The working scene characteristics of manganese carbonate pneumatic conveying systems are tailored to meet the demands of industrial production environments. These systems are commonly used in mining, chemical processing, and battery manufacturing industries where manganese carbonate is a critical raw material. The key characteristics include high efficiency in material transport, minimal product contamination due to the enclosed system, and the ability to handle large volumes of material over long distances. In industrial settings, the system's flexibility allows it to integrate with existing production lines, providing a seamless flow of materials from storage to processing units. The working environment is designed to be robust and durable, capable of withstanding the abrasive nature of manganese carbonate particles and the operational pressures required for efficient conveying. Additionally, the system's energy efficiency is a significant advantage, as it minimizes operational costs while maintaining high throughput rates. The working scene also emphasizes safety, with features such as explosion-proof designs and air filtration systems to ensure compliance with industrial safety standards. These characteristics make the pneumatic conveying system an ideal solution for handling manganese carbonate in various industrial applications, ensuring consistent performance and reliability.