With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Rare earth powder material conveying lines are specialized industrial systems engineered to handle the transportation of rare earth powders, a critical component in modern manufacturing processes. These lines are essential for industries that rely on rare earth elements, such as electronics, automotive, and renewable energy sectors, where efficient and safe material handling is paramount. The design of such lines must address the unique challenges posed by rare earth powders, including their fine particle size, potential for static electricity, and the need for contamination-free operation.

At Shandong HeadPowder Engineering Co., Ltd., we specialize in the design and manufacturing of advanced material conveying systems tailored for rare earth powder applications. Our expertise lies in creating solutions that not only meet the stringent requirements of the rare earth processing industry but also enhance operational efficiency and safety. The rare earth powder material conveying line is a comprehensive system that integrates various components to ensure reliable and continuous material transport from the source to the processing or storage point.
The design of a rare earth powder material conveying line is based on several fundamental principles aimed at optimizing performance, safety, and reliability. The system typically comprises a series of interconnected components, each playing a crucial role in the overall operation. These components include material feeders, conveying equipment (such as pneumatic or mechanical conveyors), control units, and safety devices. The selection of each component is critical and depends on factors like the powder characteristics, required conveying capacity, and the specific application environment.
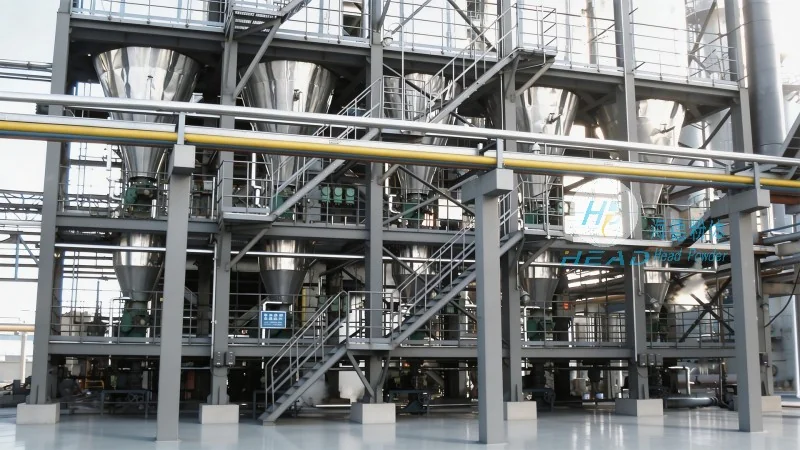
For instance, the material feeder is responsible for uniformly feeding the rare earth powder into the conveying system, preventing blockages and ensuring consistent flow. This is often achieved through devices like rotary valves or screw feeders, which are designed to handle fine powders without causing segregation or agglomeration. The conveying equipment, whether pneumatic (using air pressure to move the powder) or mechanical (using belts or chains), must be capable of handling the low density and high dust potential of rare earth powders. Pneumatic conveying systems are particularly favored for their ability to transport powders over long distances with minimal particle degradation, while mechanical systems offer advantages in terms of energy efficiency and suitability for high-temperature or corrosive environments.
Modern rare earth powder material conveying lines are equipped with advanced control and monitoring systems to ensure optimal performance and safety. These systems typically include sensors, controllers, and software that allow for real-time monitoring of key parameters such as flow rate, pressure, and temperature. The control unit, often integrated with a programmable logic controller (PLC), manages the operation of the conveying equipment, feeders, and safety devices. It can adjust the conveying speed, pressure, or feed rate based on real-time data, ensuring that the system operates within safe and efficient parameters. Additionally, the monitoring system provides alerts for any deviations or faults, enabling timely maintenance and preventing system downtime.
Given the nature of rare earth powders, which can be hazardous if not handled properly, safety is a top priority in the design of material conveying lines. The systems are equipped with various safety features, including explosion-proof components, dust suppression systems, and overpressure relief valves. These measures are designed to prevent the accumulation of static electricity, which can lead to sparks and explosions, and to minimize the risk of dust explosions. Environmental considerations are also addressed through the use of sealed conveying systems and filtration units that capture and contain any released particles, ensuring compliance with environmental regulations and protecting the surrounding environment.
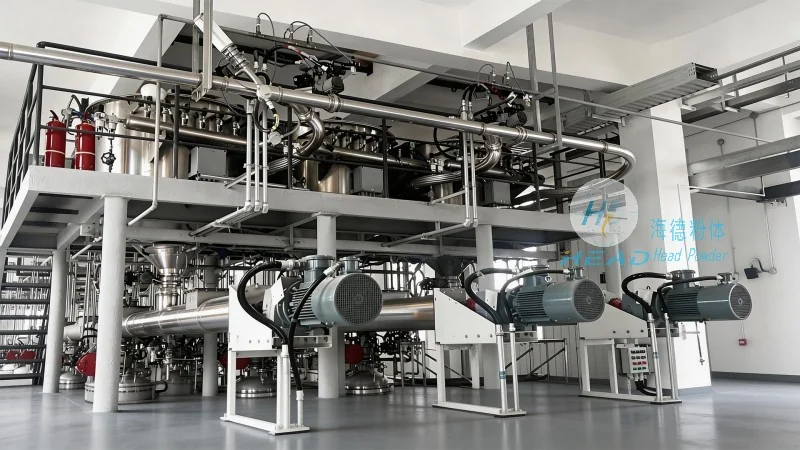
The rare earth powder material conveying line plays a vital role in the processing of rare earth elements, from raw material handling to final product packaging. In the rare earth mining and processing industry, these lines are used to transport raw ores and intermediate products to processing facilities. In the manufacturing sector, they are employed to move finished rare earth powders to assembly lines or storage areas. The efficiency of these conveying systems directly impacts the overall productivity and cost-effectiveness of rare earth processing operations. By reducing material handling time and improving safety, the conveying line contributes to higher quality output and lower operational costs for companies in the rare earth industry.
Shandong HeadPowder Engineering Co., Ltd. is committed to providing high-quality rare earth powder material conveying lines that meet the demanding requirements of the industry. Our design principles focus on reliability, efficiency, and safety, ensuring that our systems deliver optimal performance in handling rare earth powders. With a deep understanding of the unique challenges associated with rare earth materials, we continue to innovate and improve our conveying solutions to support the growth and success of our clients in the rare earth processing sector. The rare earth powder material conveying line is not just a component of the manufacturing process but a critical enabler of efficient and safe operations in the rare earth industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top