With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Bulk bag material handling systems are critical components in modern industrial operations, designed to efficiently manage the storage, transfer, and distribution of bulk materials. These systems are particularly valuable in industries such as chemicals, food processing, pharmaceuticals, and construction, where large quantities of raw materials or finished products need to be handled safely and effectively. The core of these systems lies in the seamless integration of bulk bag handling equipment, including discharge mechanisms, conveyor systems, and material transfer technologies. Understanding the working principle and key features of such systems is essential for optimizing operational efficiency and ensuring compliance with safety standards.
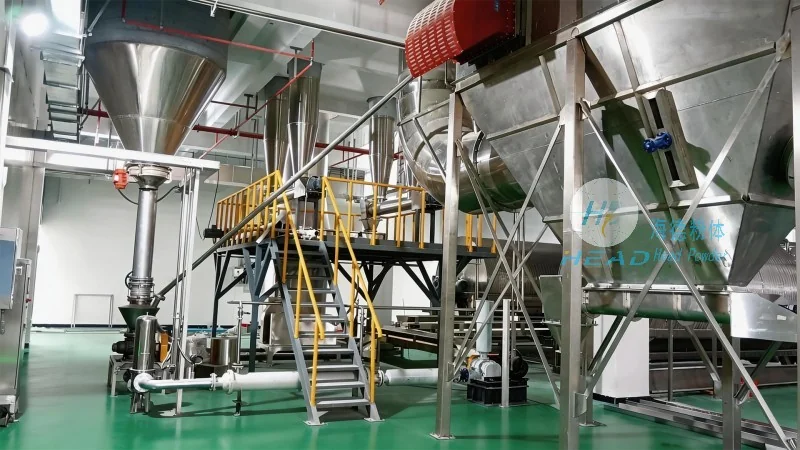
The working principle of a bulk bag material handling system typically involves several sequential steps that ensure the smooth and controlled transfer of materials from the bulk bag to the downstream processing or storage equipment. The process begins with the placement of a bulk bag, which is a flexible container made of woven fabric, typically filled with bulk materials like powders, granules, or liquids. The system then uses specialized discharge equipment to open the bag and allow the material to flow out. Common discharge methods include bottom discharge, top discharge, or side discharge, depending on the bag design and material characteristics. Once the bag is opened, a conveyor system, such as a belt conveyor or screw conveyor, is activated to transport the material from the bag to the target location. The system may also incorporate features like vibration or agitation to facilitate the flow of material, especially for cohesive or low-flowing substances. The entire process is often automated, with sensors and controls ensuring that the discharge and transfer occur at a consistent rate, minimizing waste and preventing material buildup or blockages.
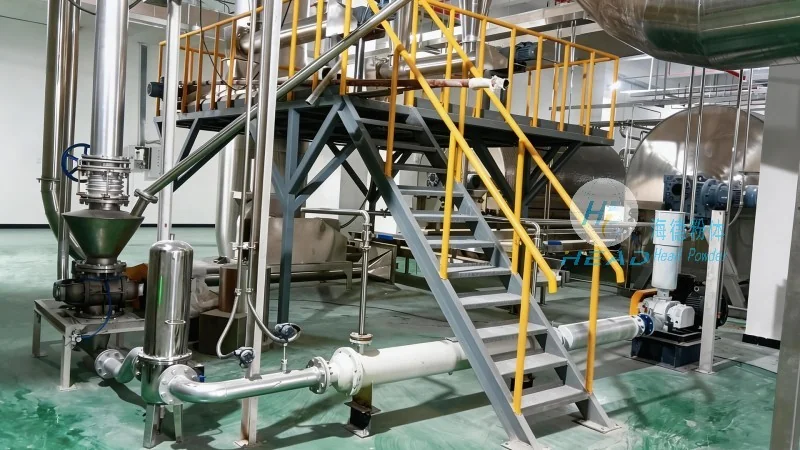
Bulk bag material handling systems are characterized by several key features that enhance their performance, reliability, and adaptability. One of the primary features is the ability to handle a wide range of material types, from free-flowing powders to highly cohesive granules, without the need for pre-processing or additional handling steps. This versatility makes the systems suitable for diverse industrial applications. Another important feature is the integration of safety mechanisms, such as overload protection, material flow monitoring, and emergency stop functions, which help prevent accidents and ensure operator safety. The systems also offer high efficiency and throughput, with automated operations reducing labor costs and increasing production speed. Additionally, the design of bulk bag handling equipment allows for easy maintenance and cleaning, which is crucial for industries with strict hygiene requirements, such as food and pharmaceuticals. The use of durable materials in the construction of the system components, such as stainless steel for conveyor parts and corrosion-resistant fabrics for bulk bags, further enhances the longevity and reliability of the equipment. Moreover, modern bulk bag material handling systems often incorporate advanced control technologies, including programmable logic controllers (PLCs) and user-friendly interfaces, enabling precise control over the discharge and transfer processes. These features collectively contribute to the effectiveness and sustainability of bulk bag material handling systems in various industrial settings.
Bulk bag material handling systems find extensive applications across multiple industries, offering significant benefits in terms of operational efficiency and cost reduction. In the chemical industry, these systems are used to handle raw materials like chemicals and reagents, ensuring safe and controlled transfer to processing equipment. The food and beverage industry benefits from the hygienic design of bulk bag handling systems, which minimizes contamination risks and maintains product quality. In the pharmaceutical sector, the systems are crucial for handling active pharmaceutical ingredients (APIs) and other sensitive materials, where precision and cleanliness are paramount. The construction industry also utilizes bulk bag material handling systems for transporting bulk materials like cement, sand, and gravel, improving material management and reducing handling time. The primary benefits of these systems include increased productivity, reduced labor costs, improved safety, and enhanced material handling accuracy. By automating the material transfer process, the systems minimize human error and ensure consistent material flow, leading to higher overall operational efficiency. Additionally, the use of bulk bag handling reduces the risk of material spillage and contamination, which is critical in industries with strict environmental and regulatory standards. The adaptability of these systems to different material types and processing requirements further enhances their value, making them a versatile solution for modern industrial operations.
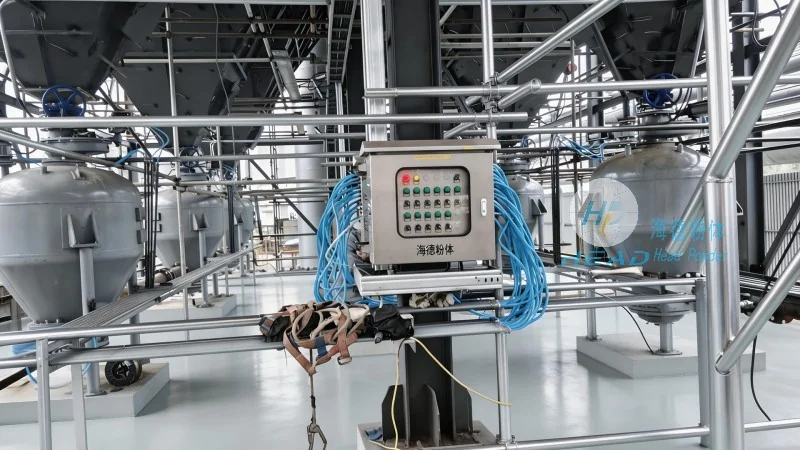
Bulk bag material handling systems represent a sophisticated and efficient solution for managing bulk materials in industrial environments. Their working principle, which combines specialized discharge mechanisms with automated conveyor systems, ensures the safe and controlled transfer of materials from bulk bags to downstream processes. The key features of these systems, including versatility, safety, efficiency, and adaptability, make them indispensable in various industries. The benefits of implementing such systems include increased productivity, reduced costs, improved safety, and enhanced material handling accuracy. As industrial operations continue to evolve, the demand for reliable and efficient bulk bag material handling systems remains high. Shandong HeadPowder Engineering Co., Ltd., a leading provider in this field, specializes in designing and manufacturing high-quality bulk bag material handling systems tailored to the specific needs of different industries. With a focus on innovation and customer satisfaction, the company ensures that its systems meet the highest standards of performance and safety. Based in Shandong, China, HeadPowder Engineering leverages advanced technology and expertise to deliver solutions that optimize material handling processes and support the growth of industrial operations worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top