With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of advanced material handling systems tailored for industrial applications, including those involving biomass ash. Based in Shandong, China, the company leverages decades of engineering expertise to deliver efficient and reliable solutions for transporting and processing biomass ash, a byproduct commonly generated in biomass energy production facilities.
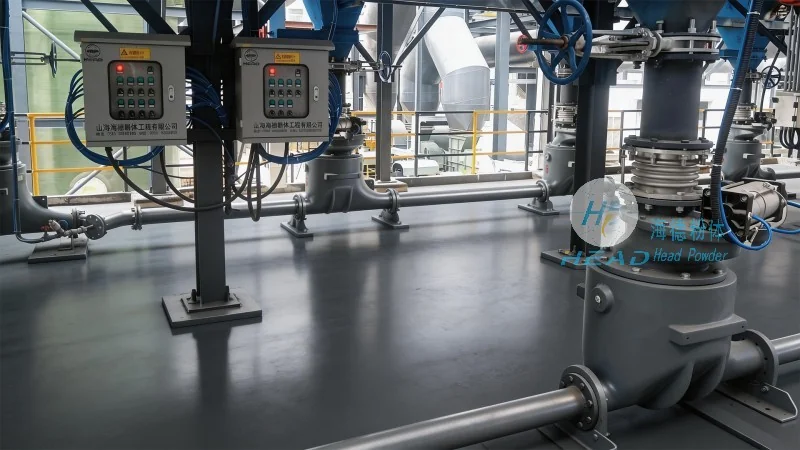
The biomass ash material handling system is a comprehensive solution designed to manage the entire lifecycle of biomass ash from collection to final disposal or reuse. It integrates multiple components, including storage silos, conveyor belts, dust collection systems, and control panels, to ensure seamless operation and minimal environmental impact. The system is engineered to handle varying ash compositions and particle sizes, making it adaptable to different biomass feedstocks and processing requirements.
At the core of the system are several critical components that work in tandem to achieve efficient material transport. The storage silo serves as the initial collection point, where ash is deposited from biomass combustion or gasification processes. This silo is typically equipped with a hopper and a discharge valve that regulate the flow of ash into the conveyor system. The conveyor belt, often a belt conveyor or screw conveyor depending on the application, transports the ash from the silo to the processing or disposal area. Dust collection systems are integrated to capture and filter airborne particles, ensuring compliance with environmental regulations and maintaining a safe working environment. Control panels provide operators with real-time monitoring and adjustment capabilities, allowing for precise control over the system's operation.
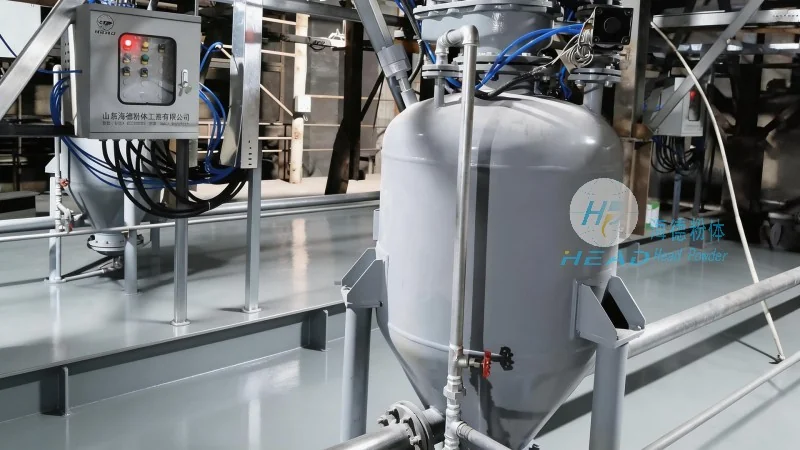
The operation of the biomass ash material handling system follows a systematic workflow that ensures consistent and reliable performance. The process begins with ash accumulation in the storage silo. Once the silo reaches a predetermined level, the discharge valve opens, allowing ash to flow into the conveyor system. The conveyor belt then transports the ash to the next stage of processing, such as a screening or crushing unit, or directly to a disposal site. Throughout this process, the dust collection system continuously operates to capture any airborne particles, preventing dust emissions and maintaining air quality. Operators monitor the system via the control panel, adjusting conveyor speeds or silo discharge rates as needed to optimize throughput and prevent system overload. The workflow is designed to minimize downtime and maximize efficiency, ensuring that the system operates continuously and reliably.
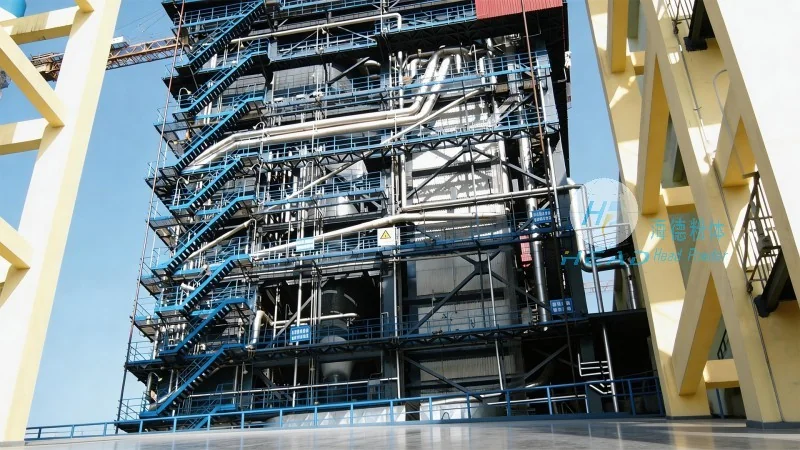
The working principle of the biomass ash material handling system combines mechanical components with advanced control technology to achieve precise material handling. The mechanical components, including the silo, conveyor, and dust collection equipment, are designed to handle the physical properties of biomass ash, such as its density, moisture content, and particle size distribution. The control system, typically based on programmable logic controllers (PLCs), monitors and controls the operation of these components. It receives input from sensors (e.g., level sensors in the silo, speed sensors on the conveyor) and processes this data to adjust the system's operation. For example, if the silo level is low, the control system may trigger the discharge valve to open and increase conveyor speed. Conversely, if the silo is full or the conveyor is overloaded, the system will automatically reduce speed or stop to prevent damage. This integration of mechanical and control systems ensures that the system operates safely, efficiently, and in compliance with operational parameters.
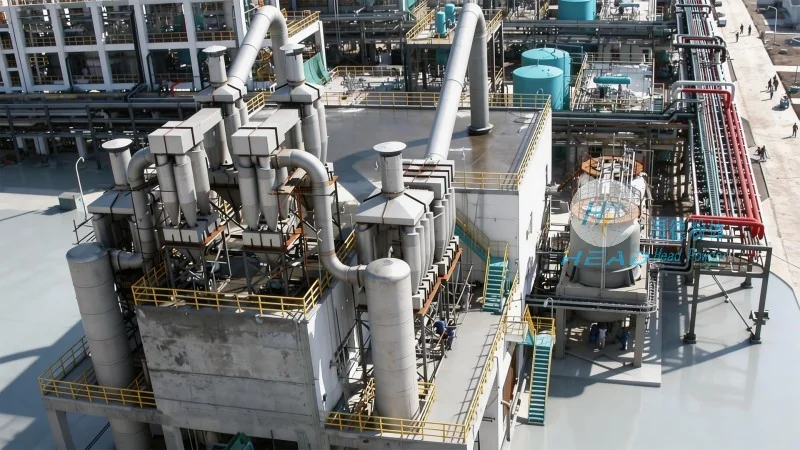
The biomass ash material handling system offers several advantages that make it suitable for a wide range of industrial applications. Its modular design allows for customization to meet specific project requirements, whether for small-scale biomass facilities or large-scale power plants. The system's efficiency in transporting biomass ash reduces labor costs and minimizes the risk of manual handling, which can be hazardous due to the ash's potential to cause respiratory issues or skin irritation. Additionally, the integrated dust collection system ensures that the system operates in compliance with environmental regulations, reducing the risk of fines or operational disruptions. The system is particularly well-suited for biomass energy production facilities, where biomass ash is a byproduct of combustion processes. It can also be applied in other industries, such as agricultural or waste management, where ash from biomass or organic materials needs to be transported and processed.
Shandong HeadPowder Engineering Co., Ltd. provides a robust and reliable biomass ash material handling system that combines advanced engineering with efficient operation. The system's comprehensive design, including storage, conveyor, and dust collection components, ensures that biomass ash is handled safely and effectively. By leveraging the company's expertise in material handling technology, clients can achieve improved operational efficiency, reduced environmental impact, and enhanced safety in their biomass ash management processes. The system is a testament to the company's commitment to delivering high-quality, customized solutions that meet the evolving needs of the industrial sector.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top