

Working Principle and Features of Powder Explosive Pneumatic Conveying Systems
For industries dealing with powder explosives, efficient and safe material handling is paramount. The powder explosive pneumatic conveying system offers a reliable solution that ensures the safe and effective transport of such materials. This article delves into the working principle and key features of such systems, providing insights into their operational mechanics and advantages.
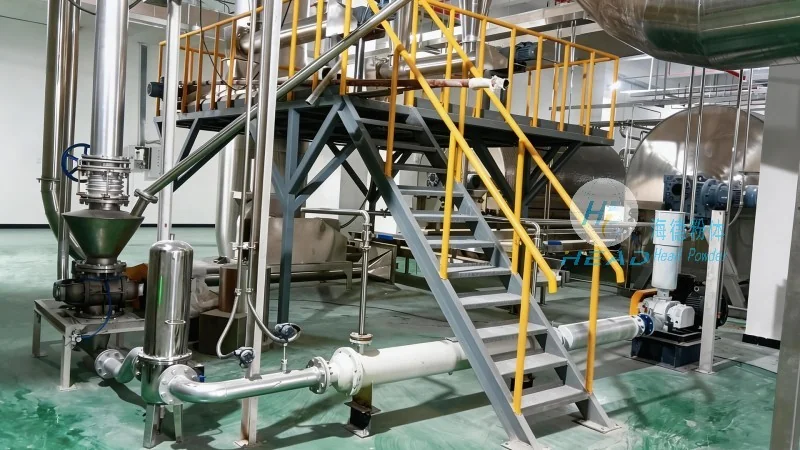
Overview of Powder Explosive Pneumatic Conveying Systems
Powder explosive pneumatic conveying systems are specialized equipment designed to transport granular or powdery explosive materials through a pipeline using air or gas as the conveying medium. Unlike traditional mechanical conveyors, these systems rely on the force of compressed air to move the material, minimizing the risk of mechanical contact that could potentially cause sparks or friction-related hazards. The system typically consists of a hopper for material storage, a conveying line, a control unit, and a discharge point. The design is tailored to meet the stringent safety standards required for handling explosive powders, ensuring compliance with industry regulations and preventing accidental ignition or explosion.
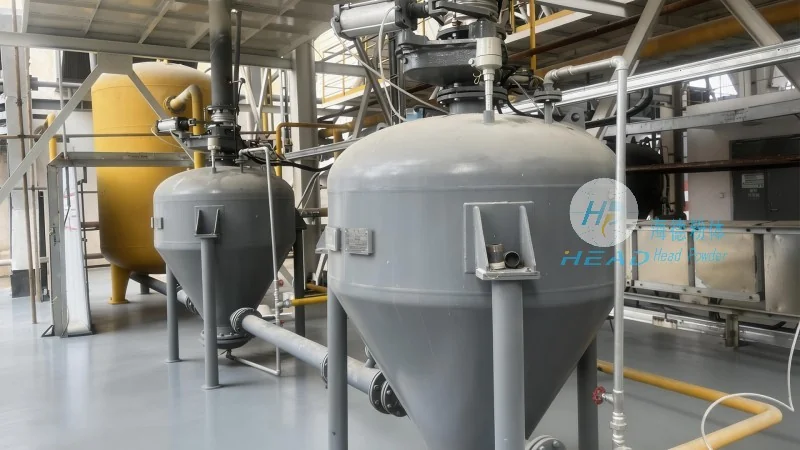
Working Principle of the Powder Explosive Pneumatic Conveying System
The operation of a powder explosive pneumatic conveying system is based on the principle of air flow and pressure differentials. The process begins with the material being fed from the hopper into the conveying line. A high-pressure air compressor generates compressed air, which is then introduced into the pipeline. As the air flows through the line, it creates a low-pressure zone that draws the powder particles into the stream. The combination of air velocity and particle size allows the material to be suspended and transported efficiently. The system may use either positive pressure (where air is pushed through the line) or negative pressure (where air is drawn out, creating a vacuum), depending on the specific application and material characteristics. The control unit monitors the air pressure, flow rate, and material feed rate to maintain optimal conveying conditions, ensuring consistent and safe operation.
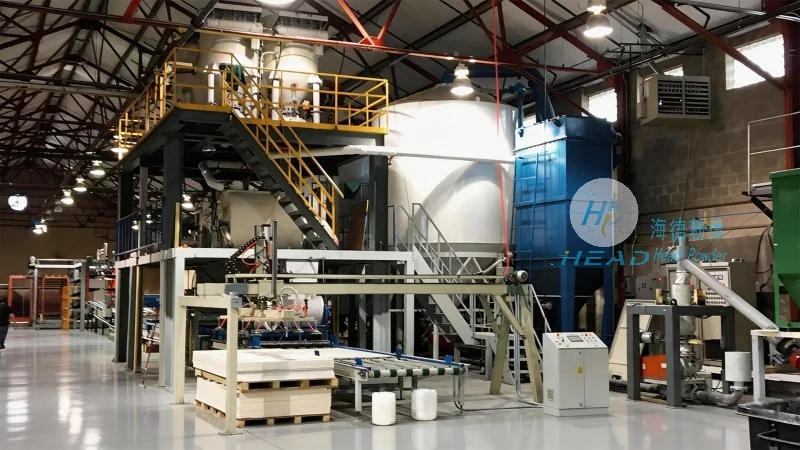
Key Features and Advantages of the System
Several distinct features make powder explosive pneumatic conveying systems highly effective for handling sensitive materials. Firstly, the system provides a fully enclosed environment, which prevents dust contamination and minimizes the risk of accidental exposure to personnel. This enclosed design also reduces the likelihood of external factors, such as moisture or contaminants, affecting the material quality. Secondly, the system operates with minimal mechanical components, reducing the risk of friction or impact that could generate sparks. The use of air as the conveying medium eliminates the need for moving parts in direct contact with the powder, enhancing safety. Additionally, the system offers flexibility in terms of layout and material handling, as the conveying line can be easily adjusted to accommodate different plant configurations. The control system allows for precise regulation of air pressure and flow, ensuring consistent material transport and preventing overloading or underloading of the pipeline. This precision control is crucial for maintaining the stability and safety of the conveying process.
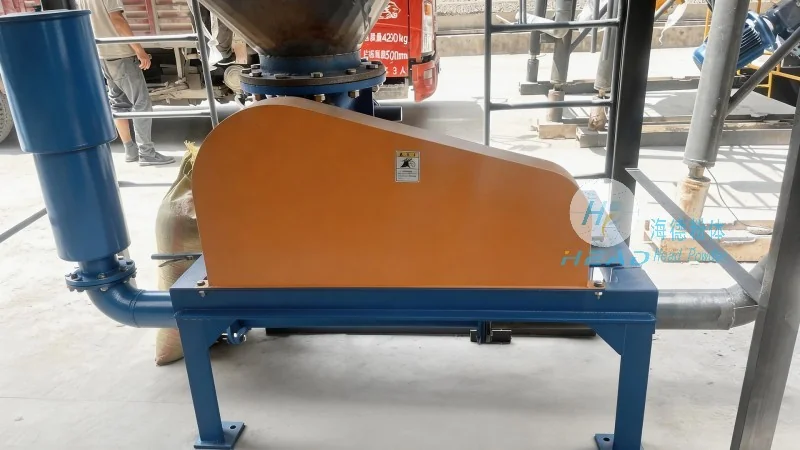
Company Information: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of specialized equipment for the handling of powder explosives. With a strong commitment to safety and innovation, the company has developed advanced pneumatic conveying systems that meet the highest industry standards. HeadPowder's systems are designed to provide reliable, efficient, and safe solutions for various applications, including the transport of gunpowder, blasting agents, and other explosive powders. The company's headquarters is located in Shandong, China, where it maintains a state-of-the-art manufacturing facility and research center. HeadPowder's team of engineers and technicians is dedicated to providing customized solutions that address the unique challenges of each client's operation, ensuring optimal performance and compliance with regulatory requirements.