With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Slurry pneumatic conveying systems represent a sophisticated and efficient method for transporting particulate materials suspended in a liquid medium. This technology, widely utilized across various industrial sectors, offers a reliable solution for handling challenging materials that traditional conveyors may struggle with. The system combines the principles of pneumatic transport with the ability to manage slurries, making it an essential tool for industries such as mining, chemical processing, and food production.
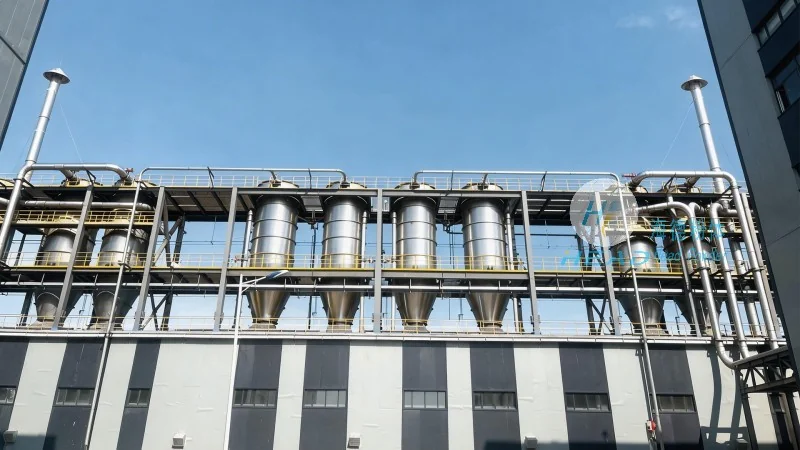
A slurry pneumatic conveying system is designed to transport slurries—mixtures of solid particles and liquid—through a pipeline using compressed air or other gases. Unlike dry bulk pneumatic systems, which handle only dry powders, slurry systems are engineered to accommodate the additional complexity of liquid content, ensuring stable and efficient transport. The core components of such a system typically include a slurry pump, a conveying line, a separator, and a control system. These components work in tandem to ensure the material is transported from the source to the destination without clogging or degradation.
The operation of a slurry pneumatic conveying system relies on the creation of a low-pressure zone within the conveying line. This is achieved by introducing compressed air into the system, which creates a vacuum that pulls the slurry mixture through the pipeline. The slurry pump, often a positive displacement type, ensures a consistent flow rate, while the air injection point is strategically placed to maintain the proper air-to-solids ratio. This ratio is critical for preventing material settling or blockages in the pipeline. The system also incorporates a separator at the end of the line, which separates the air from the slurry, allowing the liquid to be collected and the solid particles to be discharged at the destination. This separation process is vital for maintaining the integrity of the material and preventing contamination.
Several key components are integral to the effective operation of a slurry pneumatic conveying system. The slurry pump is responsible for moving the mixture through the system, providing the necessary pressure to overcome pipeline resistance. The conveying line, usually made of corrosion-resistant materials like stainless steel or polyethylene, is designed to withstand the abrasive nature of the slurry. The air injection system, which can be either in-line or external, controls the flow of air and its interaction with the slurry. The separator, often a cyclone or a bag filter, efficiently separates the air and liquid, ensuring that the material is delivered in a clean and usable state. Additionally, a control system monitors parameters such as pressure, flow rate, and temperature, allowing for real-time adjustments to maintain optimal performance.
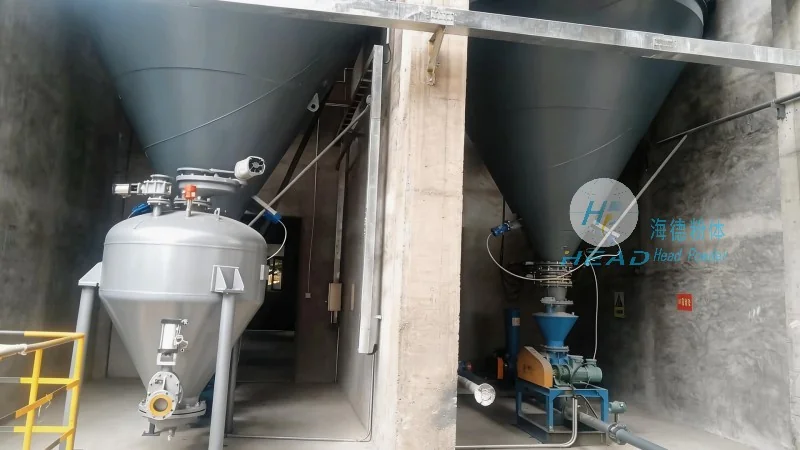
Slurry pneumatic conveying systems find extensive applications across multiple industries due to their versatility and efficiency. In the mining sector, they are used to transport tailings and ore slurries from processing plants to disposal sites or storage facilities. The chemical industry utilizes these systems for handling slurries of chemicals and catalysts, ensuring safe and controlled transport within manufacturing facilities. The food and beverage industry also benefits from slurry systems, particularly for transporting fruit purees, milk products, and other liquid-solid mixtures. Additionally, in the construction and waste management sectors, slurry systems are employed for transporting sludge and other waste materials, contributing to more sustainable waste processing.
Compared to traditional conveyor systems, slurry pneumatic conveying offers several advantages that make it a preferred choice for many applications. One of the primary benefits is the ability to transport materials over long distances without the need for multiple transfer points or elevators. This reduces installation costs and simplifies the overall system layout. The system also provides a closed-loop operation, minimizing dust emissions and environmental contamination, which is crucial for compliance with environmental regulations. Furthermore, slurry systems can handle a wide range of materials, including abrasive and corrosive substances, without significant wear or degradation. The flexibility in design allows for customization based on the specific requirements of the material being transported, ensuring optimal performance and efficiency.
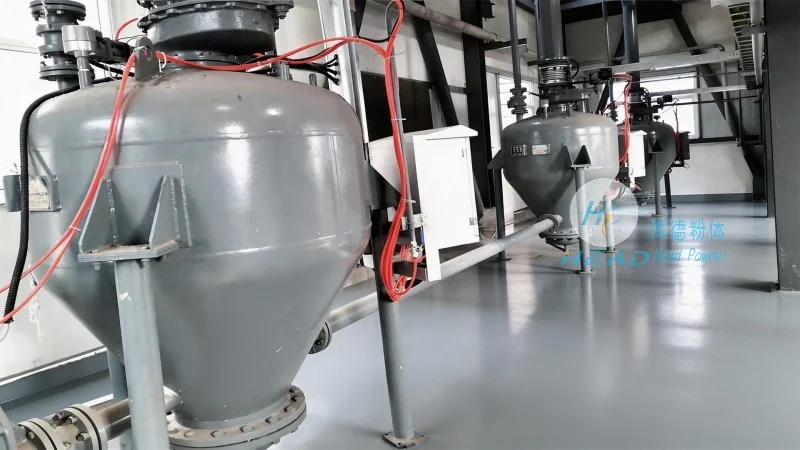
While slurry pneumatic conveying systems offer numerous benefits, they also present certain challenges that must be addressed to ensure reliable operation. One of the main challenges is the potential for clogging or blockages in the pipeline, which can be caused by the settling of solids or the formation of deposits. To mitigate this, systems often incorporate features such as air agitation and periodic flushing. Another challenge is the maintenance of the components, particularly the pump and separator, which are exposed to abrasive and corrosive conditions. Regular maintenance, including cleaning and replacement of worn parts, is essential to extend the system's lifespan and maintain performance. Additionally, the energy consumption of the system, primarily from the air compressor, can be significant. However, advancements in compressor technology and system design have helped reduce energy costs, making the system more economical over time.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of slurry pneumatic conveying solutions, specializes in designing and manufacturing customized systems tailored to the specific needs of their clients. The company, operating under the brand name headpowder, leverages years of experience and technical expertise to develop solutions that meet the unique requirements of various industries. Their systems are designed to integrate seamlessly with existing infrastructure, minimizing disruption during installation and operation. The company's approach to customization includes thorough site assessments, material analysis, and system simulations to ensure that the final design is optimized for performance, efficiency, and reliability. This personalized approach ensures that clients receive a system that not only meets their current needs but also adapts to future expansion or changes in operational requirements.
Slurry pneumatic conveying systems represent a highly effective and versatile solution for transporting slurries in various industrial applications. With their ability to handle challenging materials, provide efficient transport over long distances, and maintain a closed-loop operation, these systems offer significant advantages over traditional methods. As technology continues to advance, the design and efficiency of slurry systems are expected to improve, further enhancing their role in industrial operations. For industries seeking reliable and efficient slurry transport solutions, the expertise and products offered by companies like Shandong HeadPowder Engineering Co., Ltd. remain a key resource in achieving operational excellence and sustainability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top