

Preventing Dust Leakage in Pneumatic Conveying Systems for Industrial Alkali Transport
For industrial operations dealing with bulk materials like industrial alkali, the selection of an efficient and reliable material handling system is crucial. Pneumatic conveying systems have emerged as a preferred solution due to their ability to transport materials over long distances with minimal human intervention. However, when handling substances such as industrial alkali, which are often in powdered or granular form, the risk of dust leakage becomes a significant concern. This article explores effective strategies and solutions provided by Shandong HeadPowder Engineering Co., Ltd. to prevent dust leakage during the transport of industrial alkali, ensuring operational safety and compliance with environmental standards.
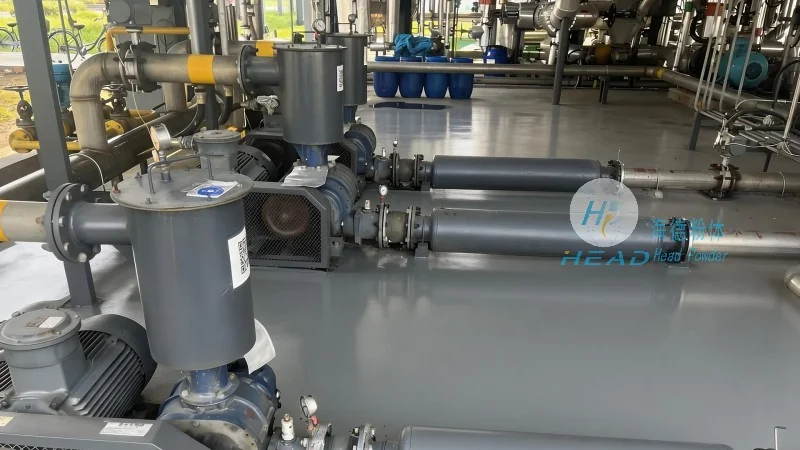
The Challenges of Dust Leakage in Alkali Transport
Industrial alkali, such as sodium hydroxide or calcium hydroxide, is commonly used in various chemical processes, including manufacturing, water treatment, and food production. When these materials are handled in bulk, the fine particles can easily become airborne, leading to dust leakage. Dust leakage not only poses health risks to workers through respiratory issues but also contributes to environmental pollution and can affect the quality of the final product. Traditional methods like bucket elevators or belt conveyors may struggle to contain dust effectively, making pneumatic conveying systems a more viable option. However, even advanced pneumatic systems require careful design and maintenance to prevent dust leakage.
Key Solutions by Shandong HeadPowder Engineering Co., Ltd. for Dust Control
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing pneumatic conveying systems tailored for industrial alkali transport. The company's approach focuses on integrating robust dust control mechanisms into the system design. Key solutions include the use of high-quality seals, airlocks, and filtration systems that minimize the escape of fine particles. For instance, the company employs advanced rotary valves and airlocks that are specifically engineered to handle the abrasive nature of industrial alkali, ensuring tight sealing and preventing dust leakage at critical points in the conveying process.
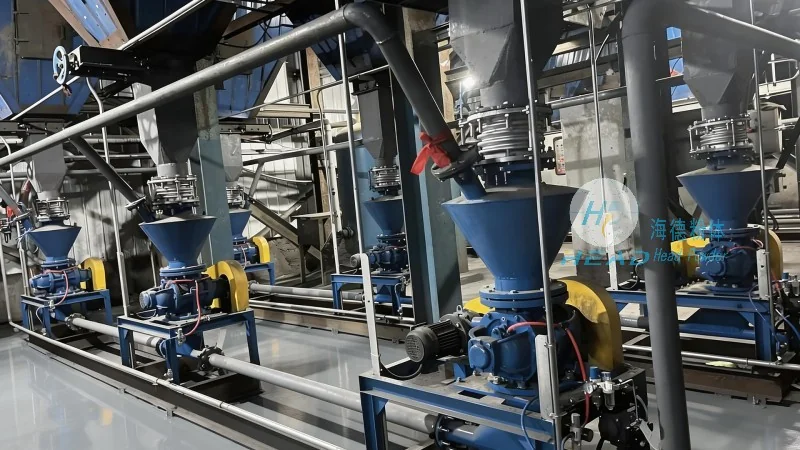
Advanced Equipment and Technologies for Efficient Alkali Handling
One of the core technologies used by HeadPowder is the positive pressure pneumatic conveying system, which is particularly effective for transporting industrial alkali. This system operates by blowing air under pressure into the conveying line, ensuring that all material is carried along with the air stream. The design includes features such as pulse-jet filters and cyclone separators that capture and recycle dust, reducing the amount of material lost to the environment. Additionally, the company utilizes flexible hoses and rigid pipes with smooth interiors to minimize friction and particle attrition, which can generate additional dust. By optimizing the air velocity and pressure, HeadPowder ensures that the conveying process is both efficient and dust-tight.
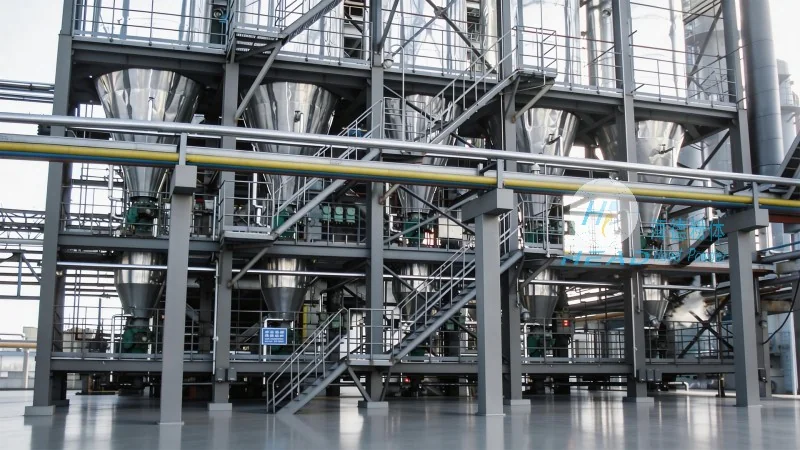
Ensuring Safety and Compliance in Industrial Alkali Conveying
Ensuring safety and compliance is a top priority for HeadPowder when designing pneumatic conveying systems for industrial alkali. The company adheres to international safety standards and environmental regulations, incorporating features like explosion-proof motors and dust collection systems that meet the requirements of industrial settings. The systems are also equipped with monitoring and control panels that allow operators to track pressure, flow rates, and dust levels in real-time. This enables proactive maintenance and quick response to any potential issues, further reducing the risk of dust leakage. Moreover, the company provides comprehensive training and support to clients, ensuring that operators are well-equipped to handle the systems safely and effectively.
Conclusion and Company Overview
In conclusion, preventing dust leakage in pneumatic conveying systems for industrial alkali transport requires a combination of advanced technology, careful system design, and rigorous maintenance. Shandong HeadPowder Engineering Co., Ltd. has established itself as a trusted partner in providing customized solutions that address the unique challenges of alkali handling. By leveraging their expertise in material handling and dust control, HeadPowder helps industrial clients maintain operational efficiency, ensure worker safety, and comply with environmental regulations. With a strong commitment to quality and innovation, the company continues to deliver reliable pneumatic conveying systems that meet the demands of modern industrial applications.