

Efficient Air-Pneumatic Conveying Systems for Solving Rare Earth Powder Transport Challenges
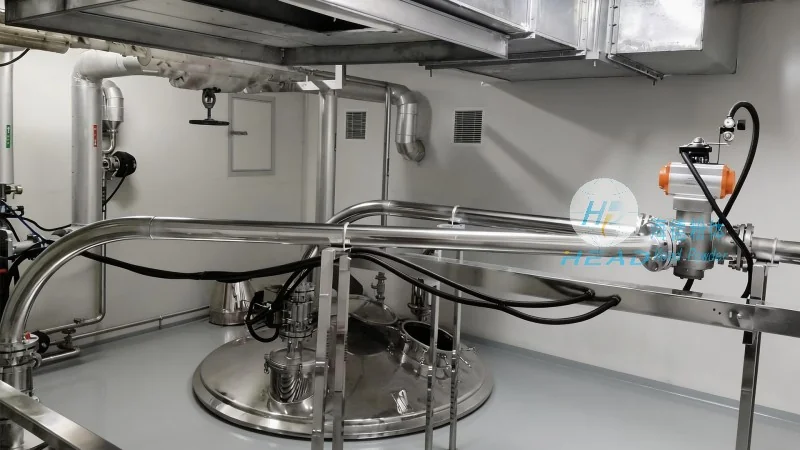
Efficient air-pneumatic conveying systems have emerged as a critical solution for the complex challenges associated with transporting rare earth powders. These specialized systems leverage compressed air to move fine powders like rare earth materials through a network of pipes, offering a reliable and efficient alternative to traditional bulk material handling methods. The unique properties of rare earth powders, such as their high density, fine particle size, and potential for static charge accumulation, make conventional methods like belt conveyors or bucket elevators less suitable. Air-pneumatic systems address these issues by providing gentle, low-friction transport that minimizes product degradation and ensures consistent flow rates.
Key Advantages of Air-Pneumatic Conveying for Rare Earth Powders
HeadPowder, a leading provider of engineering solutions, specializes in designing and implementing air-pneumatic conveying systems tailored to the demands of rare earth powder handling. The company's expertise lies in understanding the specific characteristics of rare earth materials and tailoring system configurations to optimize performance. Key advantages include:
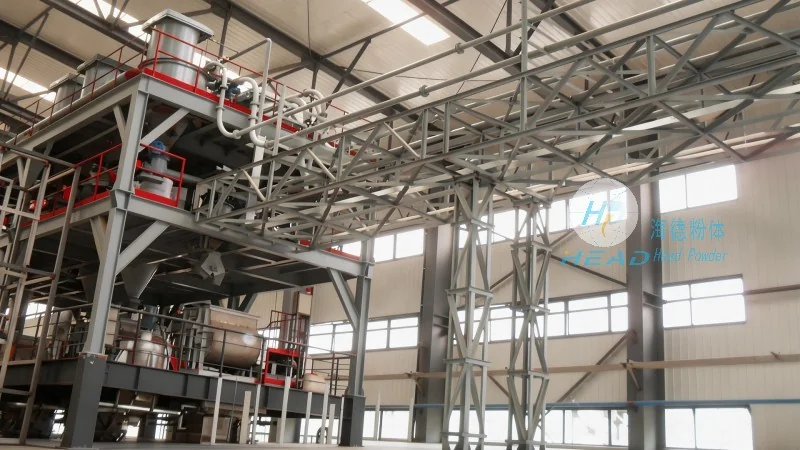
- Reduced product degradation and contamination due to gentle, low-impact transport.
- Enhanced safety through enclosed systems that prevent dust emissions and exposure.
- Improved process control with adjustable air pressure and flow rates for precise material delivery.
- Lower maintenance costs compared to mechanical conveyors, as there are fewer moving parts exposed to abrasive powders.
System Components and Design Considerations
Effective air-pneumatic conveying systems for rare earth powders involve several critical components, each designed to address the unique challenges of the material. These components include:
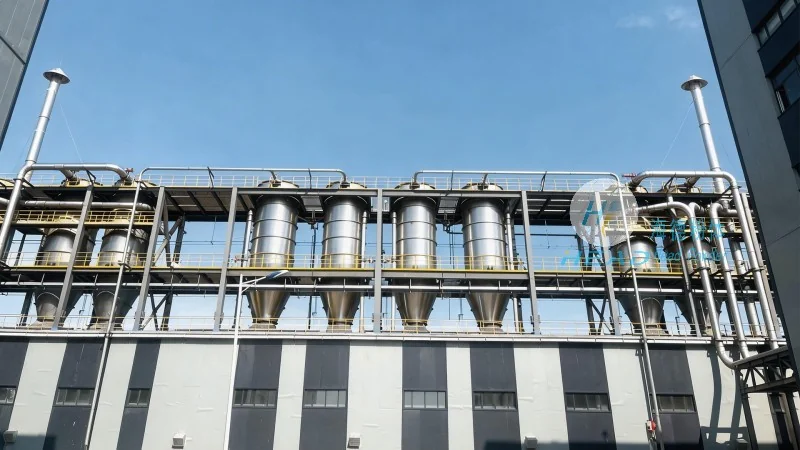
- Inlet Hoppers and Feeders: Precision feeders ensure consistent material flow into the system, preventing blockages and maintaining uniform particle distribution.
- Pneumatic Conveying Lines: High-quality, corrosion-resistant pipes are used to transport the powder, often with internal coatings or smooth surfaces to minimize friction and prevent material buildup.
- Control Valves and Regulators: These components manage air pressure and flow, allowing operators to adjust system performance based on material characteristics and process requirements.
- Collection Hoppers and Discharge Equipment: The system concludes with a collection hopper that safely stores the transported powder, with discharge mechanisms that prevent re-entrainment of dust.
Application in Rare Earth Processing
HeadPowder's air-pneumatic conveying solutions are widely applied in the rare earth processing industry, from raw material handling to finished product packaging. The systems are integral to processes such as:
- Transporting raw rare earth ores and concentrates from storage to processing facilities.
- Conveying intermediate products like pre-concentrated rare earth oxides between grinding and separation stages.
- Delivering final rare earth products to packaging lines or storage silos, ensuring minimal loss and contamination.
Case Study: Enhancing Efficiency in a Rare Earth Smelting Plant
A recent project by HeadPowder involved upgrading the material handling system at a major rare earth smelting plant in Shandong, China. The plant previously relied on traditional bucket elevators, which suffered from frequent downtime due to material buildup and product degradation. HeadPowder designed and installed a custom air-pneumatic conveying system that integrated with the existing infrastructure. The new system reduced material degradation by 40% and cut downtime by 60%, leading to a significant increase in overall plant efficiency. The project demonstrated the system's ability to handle the high-volume, fine-particle nature of rare earth powders while maintaining operational reliability.
Customization and Support from HeadPowder
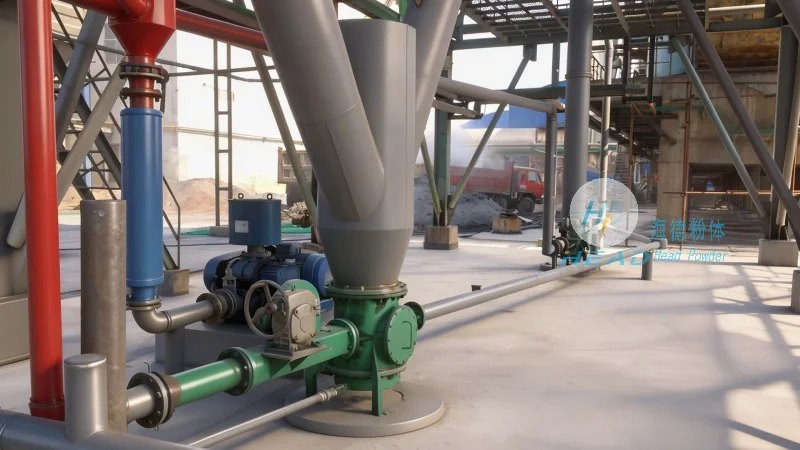
HeadPowder understands that each rare earth processing facility has unique requirements. The company offers comprehensive customization services, working closely with clients to design systems that meet specific material properties, flow rates, and operational constraints. This includes conducting thorough material analysis to determine the optimal air pressure, pipe diameter, and system layout. Additionally, HeadPowder provides ongoing technical support and maintenance services to ensure the longevity and efficiency of the conveying systems. The company's commitment to quality and customer satisfaction has made it a trusted partner in the rare earth industry.