With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Coal ash, a byproduct of coal combustion, poses unique challenges in handling and transportation due to its fine particle size and variable moisture content. Traditional methods such as belt conveyors or bucket elevators often struggle with dust generation, material segregation, and operational inefficiencies. Pneumatic conveying technology emerges as a robust solution, offering a dust-free, continuous, and flexible approach to coal ash transport. This article explores the application and optimization of pneumatic conveying systems specifically tailored for coal ash, highlighting key design considerations and operational benefits.
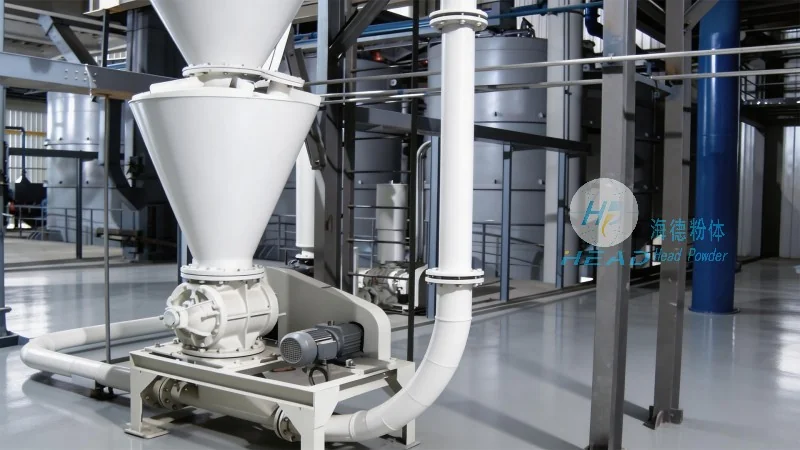
Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial conveying systems, specializes in developing customized pneumatic conveying solutions for diverse industrial applications. With a focus on innovation and reliability, HeadPowder has established itself as a trusted partner in the field of material handling. The company’s expertise lies in understanding the specific requirements of coal ash transport, ensuring that each system is engineered to meet stringent performance standards and operational demands.
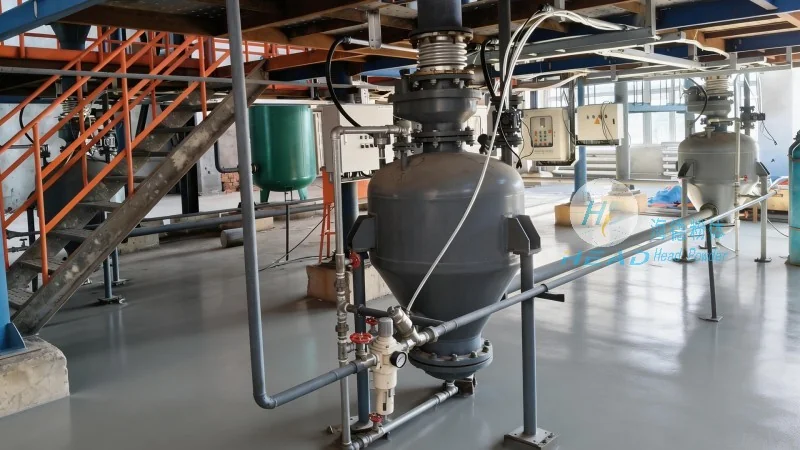
The successful implementation of pneumatic conveying for coal ash relies on careful consideration of several critical factors. First, the selection of the appropriate conveying type—whether dilute-phase or dense-phase—depends on the ash's properties, such as particle size distribution and moisture content. Dilute-phase systems, which use high air velocities to transport material in a dispersed state, are ideal for fine coal ash with low bulk density. Dense-phase systems, on the other hand, use lower air velocities and higher pressure to move material in a slurry-like state, reducing wear on equipment and minimizing pressure drops. Additionally, the design of the conveying line, including pipe diameter, bends, and valves, must be optimized to minimize friction losses and prevent material deposition. HeadPowder engineers employ advanced computational fluid dynamics (CFD) simulations to model the flow behavior of coal ash in the system, ensuring efficient and reliable operation.
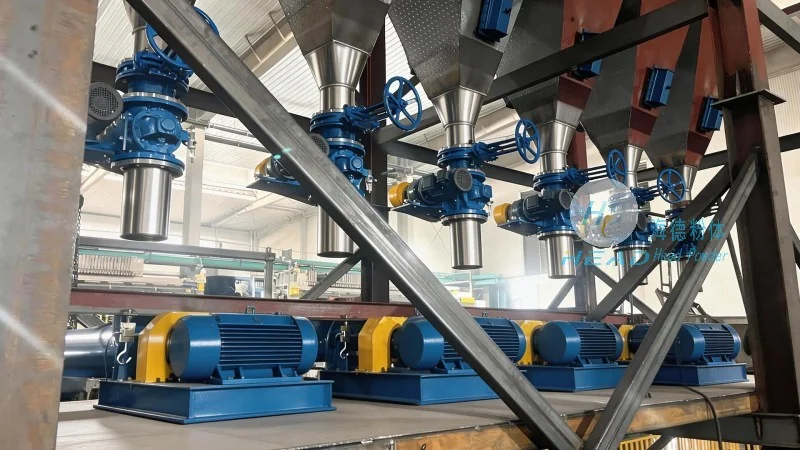
Optimization of pneumatic conveying systems for coal ash involves several strategies aimed at enhancing performance and reducing operational costs. One key approach is the integration of advanced control systems that monitor and adjust air flow, pressure, and material feed rates in real-time. This dynamic control helps maintain consistent conveying rates, preventing overloading or underloading of the system. Another optimization technique is the use of specialized equipment, such as cyclone separators and dust collectors, to improve material recovery and reduce environmental impact. These components ensure that the coal ash is efficiently separated from the conveying air, minimizing dust emissions and facilitating reuse or disposal. Furthermore, regular maintenance and inspection of the conveying system are crucial to prevent equipment failure and extend the system's lifespan. HeadPowder provides comprehensive maintenance services, including routine checks, component replacement, and performance testing, to ensure optimal operation of the system.
Implementing pneumatic conveying technology for coal ash transport offers numerous benefits that outweigh the initial investment. One of the most significant advantages is the elimination of dust and airborne particles, which improves workplace safety and reduces environmental pollution. Unlike traditional methods, pneumatic conveying operates in a closed system, preventing dust from escaping into the environment and minimizing the risk of respiratory issues for workers. Additionally, the continuous and flexible nature of the system allows for seamless integration with other industrial processes, such as ash utilization or disposal. This integration enhances overall operational efficiency and reduces downtime. Furthermore, pneumatic conveying systems are capable of handling a wide range of ash compositions, including high-moisture or abrasive materials, without causing excessive wear on equipment. The low maintenance requirements and long service life of these systems also contribute to cost savings over time.
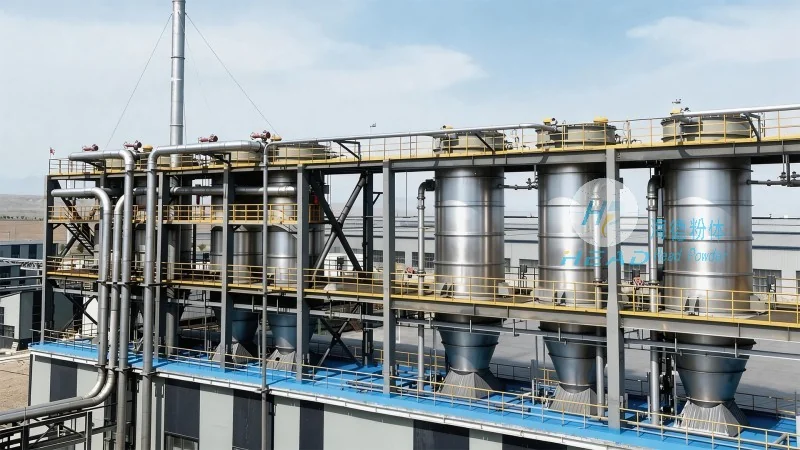
In conclusion, pneumatic conveying technology represents a highly effective and efficient solution for coal ash transport. By optimizing the design and operation of these systems, industries can improve safety, reduce environmental impact, and enhance overall operational performance. Shandong HeadPowder Engineering Co., Ltd. stands ready to provide tailored pneumatic conveying solutions that address the unique challenges of coal ash handling. With its expertise in engineering and commitment to quality, HeadPowder ensures that each system is optimized for maximum performance and reliability, helping clients achieve their material handling goals while meeting regulatory requirements.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top