With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
The global demand for high-quality flour has necessitated the modernization of processing facilities across the globe, with North Africa being a significant region for agricultural production and food processing. Located in the heart of the Kingdom of Morocco, the capital city of Rabat presents a unique set of logistical and environmental challenges for industrial operations. To address the critical need for efficient material handling, Shandong Headpowder Engineering Co., Ltd. successfully executed a sophisticated **air conveying case** designed specifically for a flour manufacturing facility in this strategic location. This project represents a landmark achievement in industrial automation, transforming the traditional dusty and labor-intensive methods of flour handling into a streamlined, high-tech operation. The implementation of this system was not merely an upgrade of equipment but a complete overhaul of the facility's logistics infrastructure, ensuring that the delicate flour products reached their destination with maximum integrity and minimal waste.

At the core of this engineering marvel is the specialized **pneumatic conveying of flour**, a process that leverages the power of air pressure to move granular materials through a closed pipeline system. Unlike traditional mechanical conveyors, such as screw conveyors or bucket elevators, which can cause significant material degradation and generate excessive dust, the air-based system employed in Rabat ensures a gentle yet efficient transfer of the product. This project highlights the growing trend of **air conveying in Africa**, where industrial facilities are increasingly adopting Western-level technology to improve operational standards and meet international food safety regulations. The facility in Rabat now operates with a level of precision that was previously unattainable, setting a new benchmark for flour processing plants in the region.
Before the implementation of the new system, the flour processing plant in Rabat faced a myriad of operational hurdles that threatened both product quality and worker safety. The primary concern was the generation of airborne flour dust, a byproduct of traditional bulk handling methods. In a flour mill, dust is not merely a nuisance; it is a significant safety hazard. Flour dust is highly combustible, and the accumulation of fine particulate matter in the air poses a severe explosion risk. Furthermore, the traditional mechanical systems were prone to wear and tear, requiring frequent maintenance and leading to unplanned downtime. The manual intervention required for these older systems also increased the risk of cross-contamination, as the open handling processes allowed for the introduction of foreign particles and bacteria.
Moreover, the specific climatic conditions of Morocco, characterized by high temperatures and varying humidity levels, added another layer of complexity to the material handling process. Flour is a hygroscopic material, meaning it absorbs moisture from the air, which can cause it to clump and clog conventional machinery. The facility needed a solution that could withstand these environmental stressors while maintaining consistent output. The existing infrastructure was unable to cope with the increasing volume of production, leading to bottlenecks in the packaging and storage stages. These challenges necessitated a comprehensive solution that would address not only the immediate logistical issues but also the long-term sustainability and safety of the plant's operations.
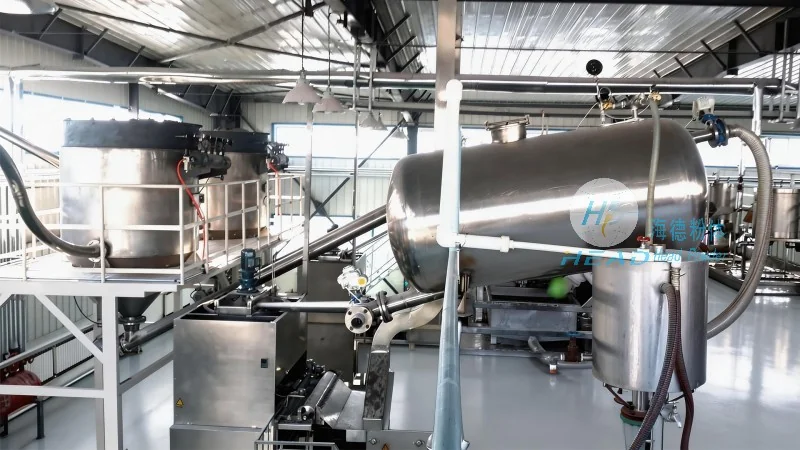
To overcome these challenges, Shandong Headpowder Engineering Co., Ltd. designed a bespoke pneumatic conveying system tailored to the specific needs of the Rabat facility. The core of this solution is the **dust-free automated air conveying** technology, which utilizes a closed-loop pipeline system to transport the flour from the storage silos to the packaging machines. This system is engineered to operate under precise pressure differentials, ensuring that the flour is moved through the pipes with a consistent and controlled velocity. By controlling the flow rate and air pressure, the system prevents the material from settling or bridging, which are common issues that plague older conveyor systems.
The engineering team focused heavily on the selection of components that would ensure reliability and efficiency. High-performance Roots blowers and vacuum pumps were selected to generate the necessary airflow, while specialized rotary valves were used to meter the flour into the conveying lines. The system is designed to handle the high volume of throughput required by a modern mill without compromising on energy efficiency. One of the standout features of this implementation is the integration of advanced filtration technology. The system is equipped with state-of-the-art cyclone separators and pulse-jet bag filters, which capture and remove any dust particles from the exhaust air before it is released back into the environment. This ensures that the surrounding area remains clean and that the air quality meets strict occupational health and safety standards.
The transition to a **dust-free automated air conveying** system offers profound benefits that extend far beyond simple cleanliness. From a quality assurance perspective, the closed system ensures that the flour remains uncontaminated throughout the entire transportation process. There is no risk of dust from other parts of the factory settling onto the product, nor is there a risk of the flour absorbing moisture or foreign odors from the open air. This level of protection is crucial for maintaining the premium quality of the flour, which is the primary product of the facility. Additionally, the automation aspect of the system drastically reduces the need for manual labor. Operators can monitor the entire process from a central control panel, adjusting parameters and troubleshooting issues remotely. This not only improves efficiency but also creates a safer working environment by minimizing the need for workers to be exposed to dust and moving machinery.
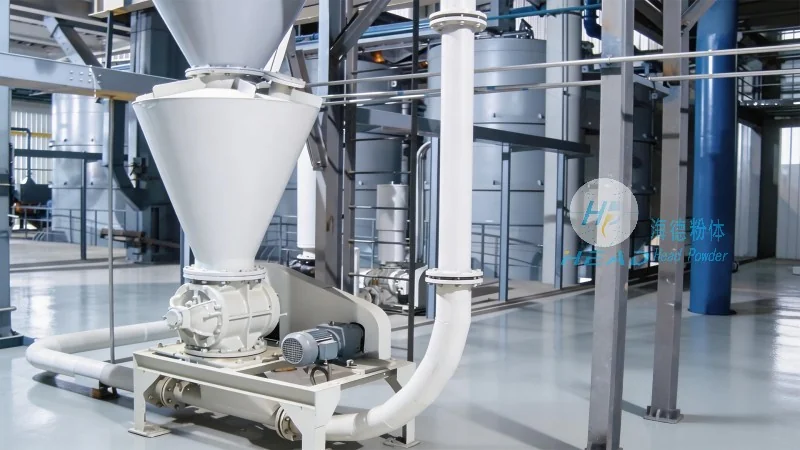
The economic impact of this project cannot be overstated. By eliminating the frequent maintenance requirements of mechanical conveyors and reducing the downtime associated with clogs and jams, the facility has seen a significant increase in overall productivity. The energy efficiency of the pneumatic system also contributes to lower operational costs over the long term. The **air conveying case** in Rabat serves as a testament to the economic viability of investing in advanced material handling technology. It demonstrates that while the initial capital investment may be higher than traditional methods, the long-term savings in maintenance, labor, and product waste make it a sound financial decision.
The engineering design of the Rabat project was a collaborative effort between the technical team at Shandong Headpowder Engineering Co., Ltd. and the facility's management. The goal was to create a seamless integration of the new pneumatic system with the existing infrastructure. The process flow begins at the receiving hoppers, where the raw flour is fed into the system via rotary airlock valves. These valves ensure that the system remains sealed, preventing air from escaping while allowing material to enter. The flour is then transported through a network of stainless steel pipes to the destination points, such as filling machines or intermediate storage silos.
A key component of the design is the use of variable frequency drives (VFDs) on the blowers and motors. This allows for precise control over the airflow, adjusting it in real-time to match the specific demands of the conveying process. For instance, during peak production hours, the system can ramp up the speed to handle larger volumes, while during off-peak times, it can throttle back to save energy. The system is also equipped with smart sensors that monitor pressure and flow rates. If any deviation from the normal operating parameters is detected, the system can automatically adjust or alert the operators, ensuring that potential issues are addressed before they escalate into major problems. This level of sophistication is what defines a modern **air conveying in Africa** project, setting it apart from older, less intelligent systems.
Shandong Headpowder Engineering Co., Ltd. has established itself as a leader in the field of industrial material handling, and the Rabat project is a shining example of their technical prowess. With a strong foundation in engineering and a deep understanding of the unique challenges faced by the food industry, the company provides end-to-end solutions that cover everything from system design and manufacturing to installation and after-sales service. The team's expertise in **pneumatic conveying of flour** is particularly noteworthy, as they understand the delicate nature of the product and the rigorous standards required to process it safely.
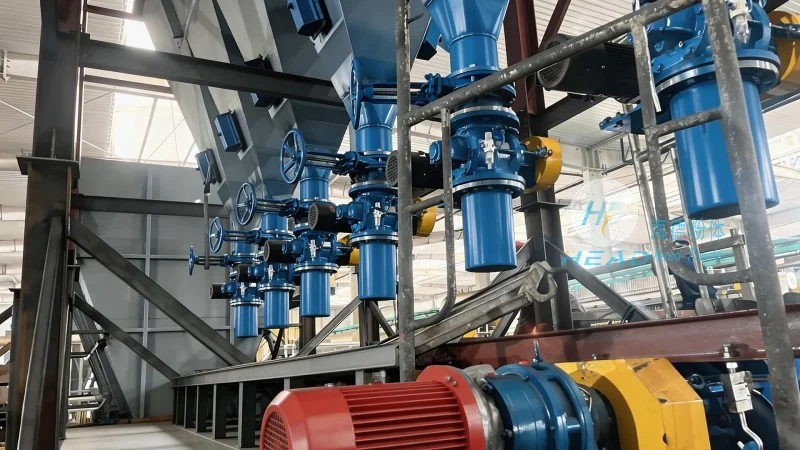
Located in Shandong, China, the company benefits from a robust industrial base and a wealth of technical talent. They have successfully delivered numerous projects across the globe, and their experience in the African market is extensive. They understand the local regulations, the environmental conditions, and the operational needs of the facilities in the region. This local knowledge, combined with their global engineering standards, ensures that every project they undertake is a success. The company’s commitment to innovation is evident in their continuous investment in research and development, ensuring that their systems remain at the cutting edge of technology.
The successful completion of the flour handling project in Rabat, Morocco, stands as a testament to the effectiveness of modern pneumatic conveying technology. By implementing a **dust-free automated air conveying** system, the facility has achieved a new level of operational excellence, safety, and product quality. This project not only solved the immediate logistical challenges but also positioned the plant for future growth and scalability. For companies in the food processing industry looking to upgrade their material handling capabilities, this case study serves as a compelling example of what is possible with the right engineering partner.
Shandong Headpowder Engineering Co., Ltd. is dedicated to providing superior solutions for the global market. If you are interested in learning more about how a pneumatic conveying system can transform your operations, or if you require a customized solution for your specific needs, we invite you to reach out. Our team of experts is ready to assist you in designing a system that meets your exact requirements. Please contact Zhang Manager for further information and consultation. You can reach us via WeChat at 15662777102 to discuss your project details and explore how we can help you achieve your operational goals.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top