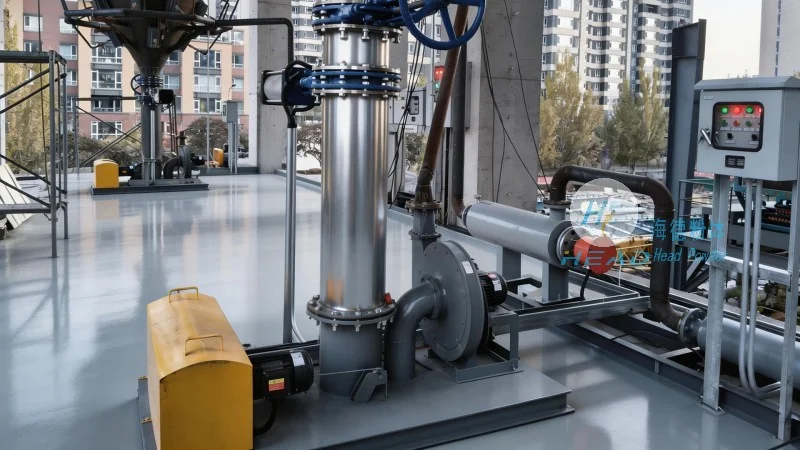
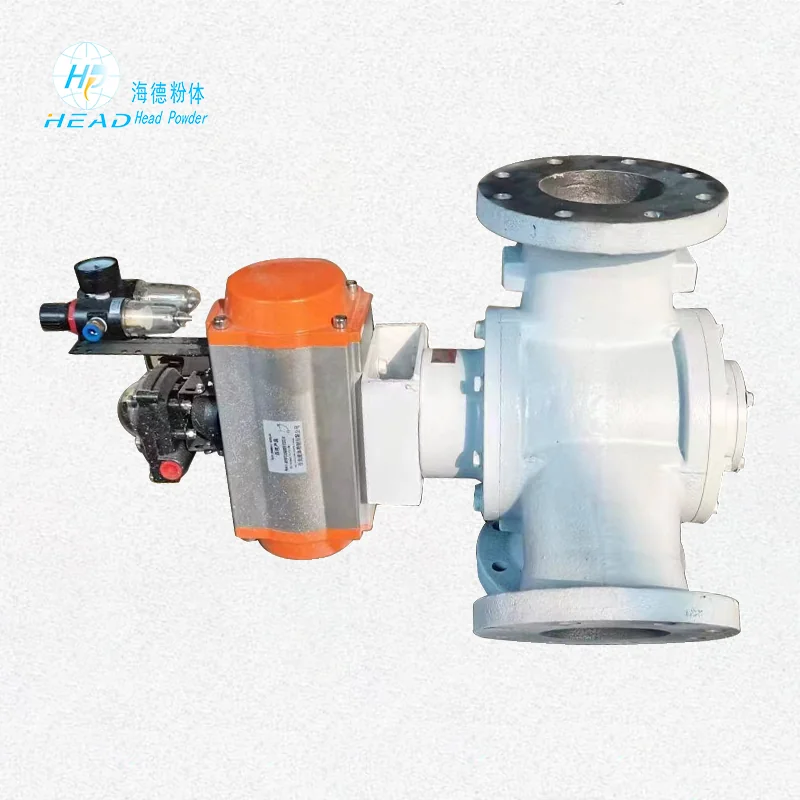
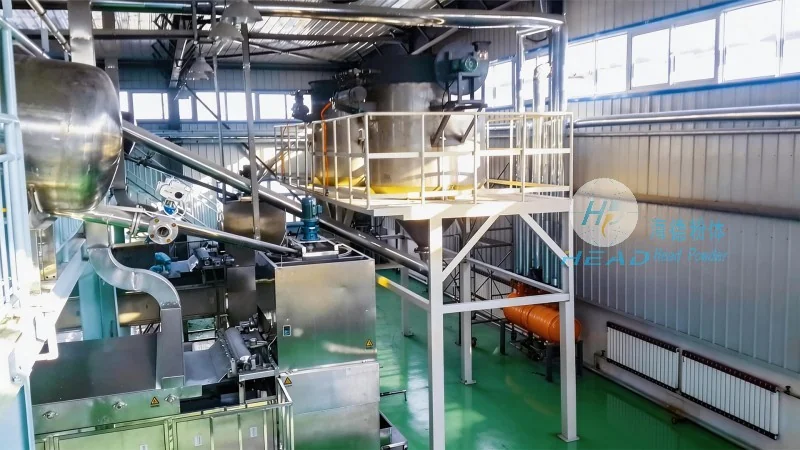
With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Pneumatic conveying systems represent a cornerstone technology in modern material handling, offering a reliable and efficient method for transporting bulk solids from one location to another. Among the various methodologies employed in this field, the suction pneumatic conveying system stands out due to its unique operational characteristics and broad applicability. This system utilizes air pressure differentials to move materials through pipelines, ensuring a controlled and consistent flow. Unlike pressure systems that push material, suction systems pull material through the system, which offers distinct advantages in terms of safety, flexibility, and environmental control.
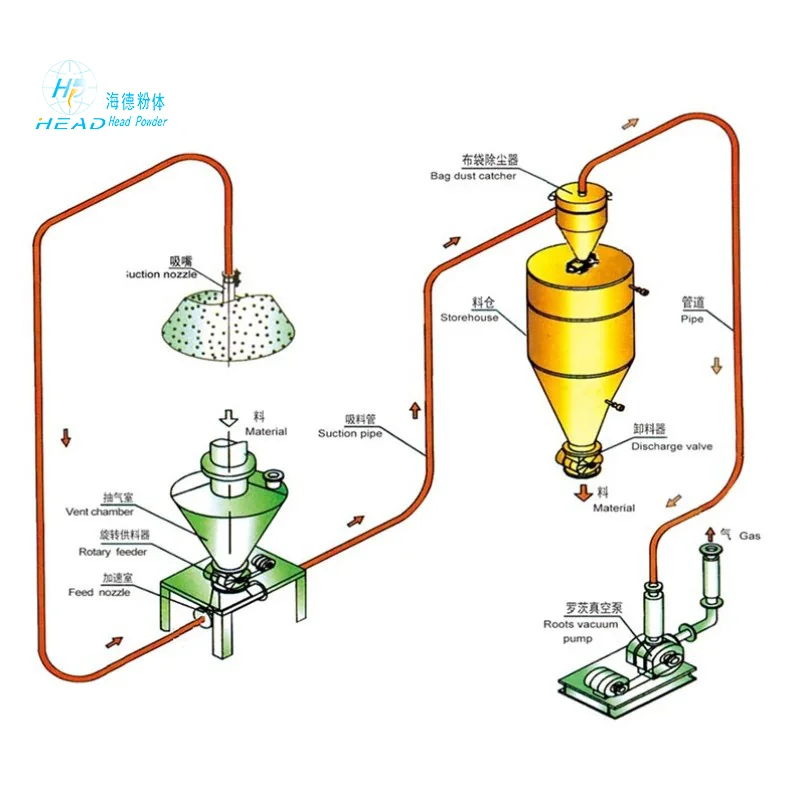
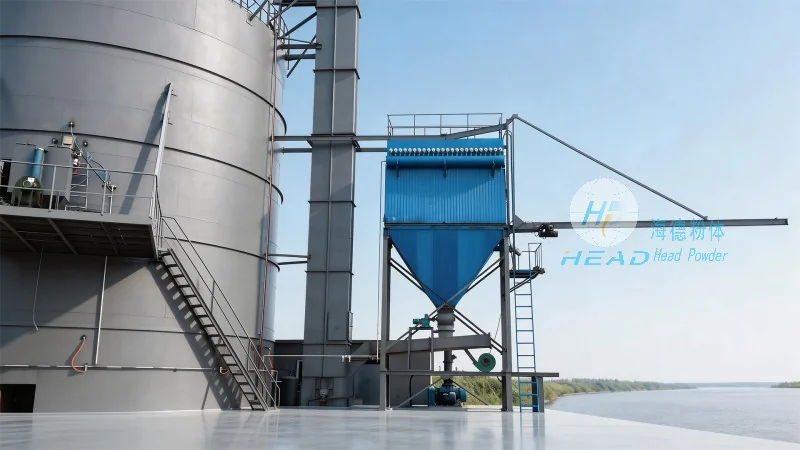
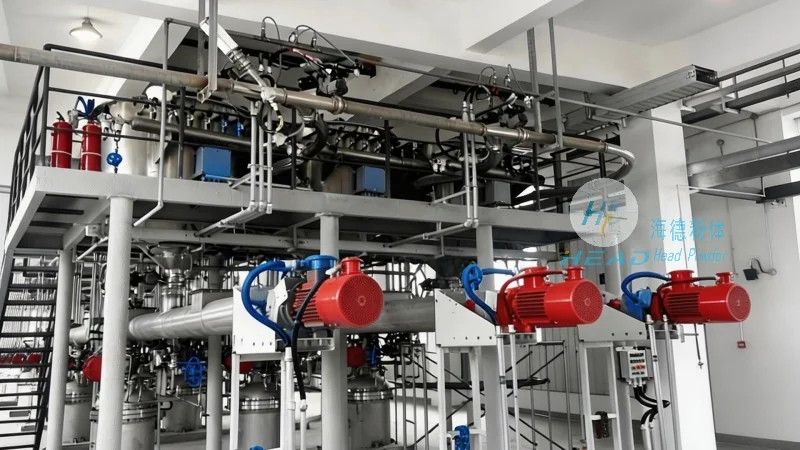
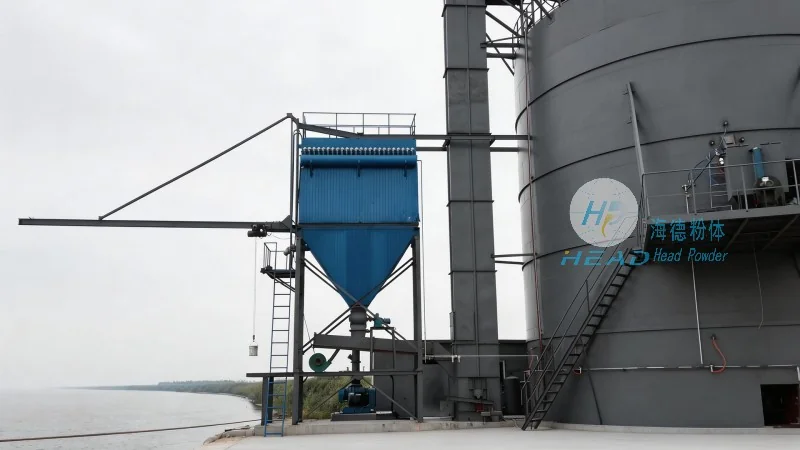
The operation of a suction pneumatic conveying system is fundamentally based on the creation of a vacuum within the conveying line. This vacuum is typically generated by a vacuum pump, a Roots blower, or a liquid ring vacuum pump located at the receiving end of the system. As the vacuum is established, air is drawn into the system, creating a flow that entrains the bulk material. The material is introduced into the conveying line through vacuum hoppers or rotary valves at various points along the line. Once inside the pipeline, the material is transported to a central receiver or separator where the air and material are separated. The clean air is then filtered and recirculated or exhausted, while the material is discharged into a storage silo or processing unit. This method is particularly effective for handling materials that generate dust or require strict containment.
One of the primary benefits of employing a suction pneumatic conveying system is its superior dust control capabilities. Because the system operates under negative pressure, there is no risk of material leakage into the surrounding environment. This feature is critical in industries such as pharmaceuticals, food processing, and chemical manufacturing, where maintaining a clean and sterile environment is paramount. Additionally, suction systems are highly flexible in terms of layout. They can easily handle multiple pickup points, allowing materials to be collected from various silos, hoppers, or storage bins and transported to a single destination. This versatility makes them ideal for complex plant layouts where space may be limited or where material sources are dispersed.
The versatility of the suction pneumatic conveying system allows it to be utilized across a wide spectrum of industries. In the chemical industry, it is often used to transport powders, granules, and flakes safely and efficiently. The food and beverage sector relies on these systems for conveying ingredients like flour, sugar, and starch, ensuring that the product remains uncontaminated throughout the process. Furthermore, the construction industry utilizes suction conveying for materials such as cement, fly ash, and lime, which are prone to dusting. The ability to transport materials over both horizontal and vertical distances with minimal mechanical wear makes this system a preferred choice for bulk material handling operations worldwide.
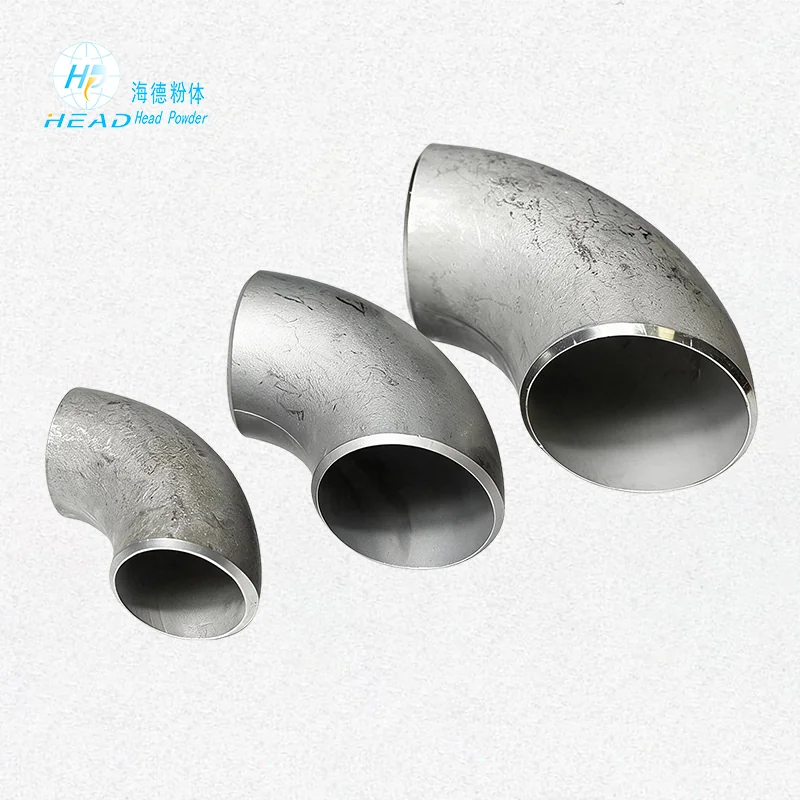
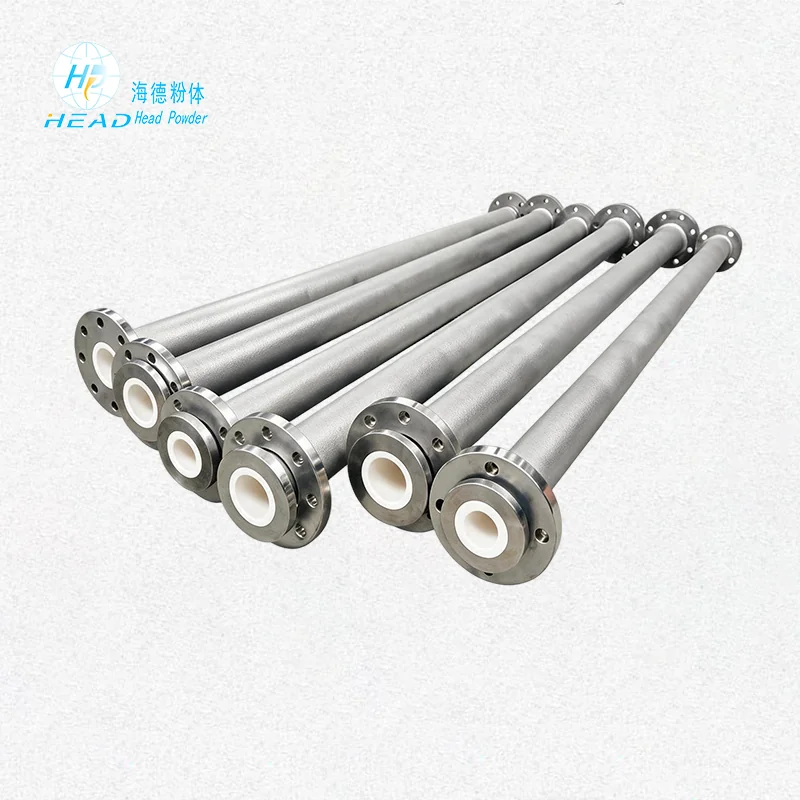
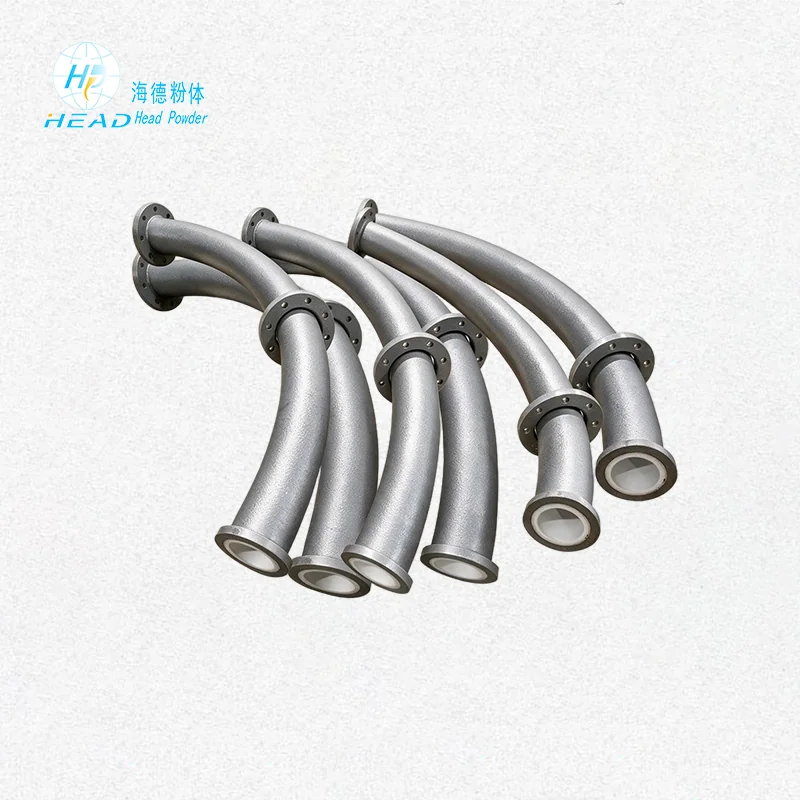
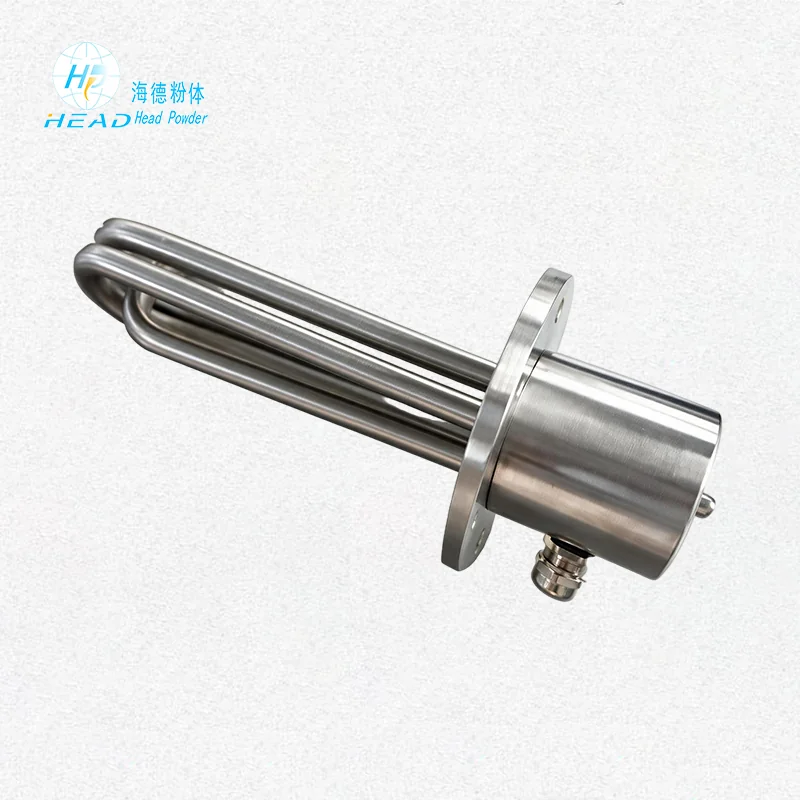
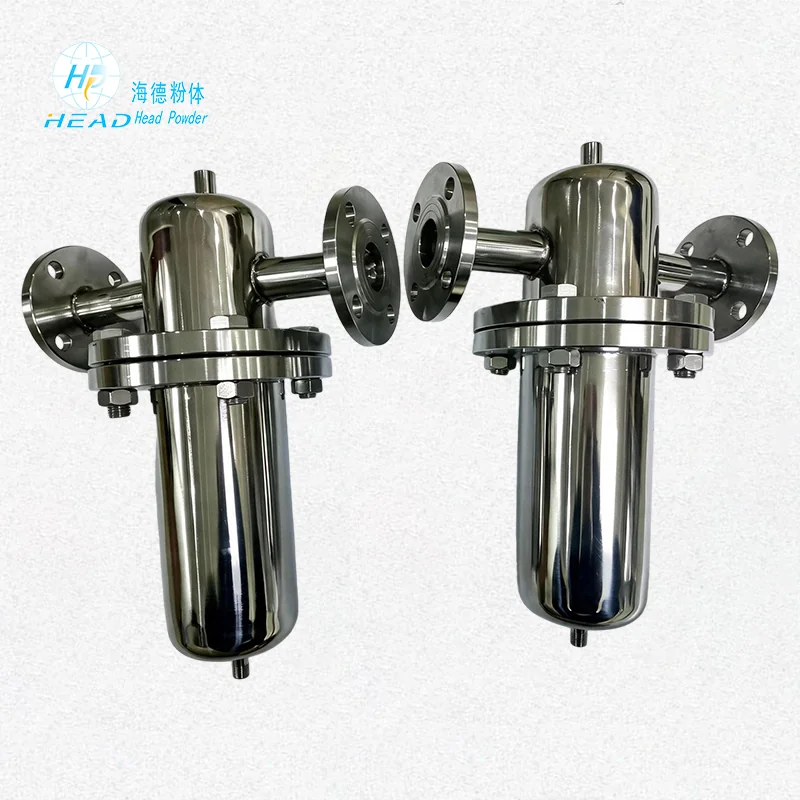
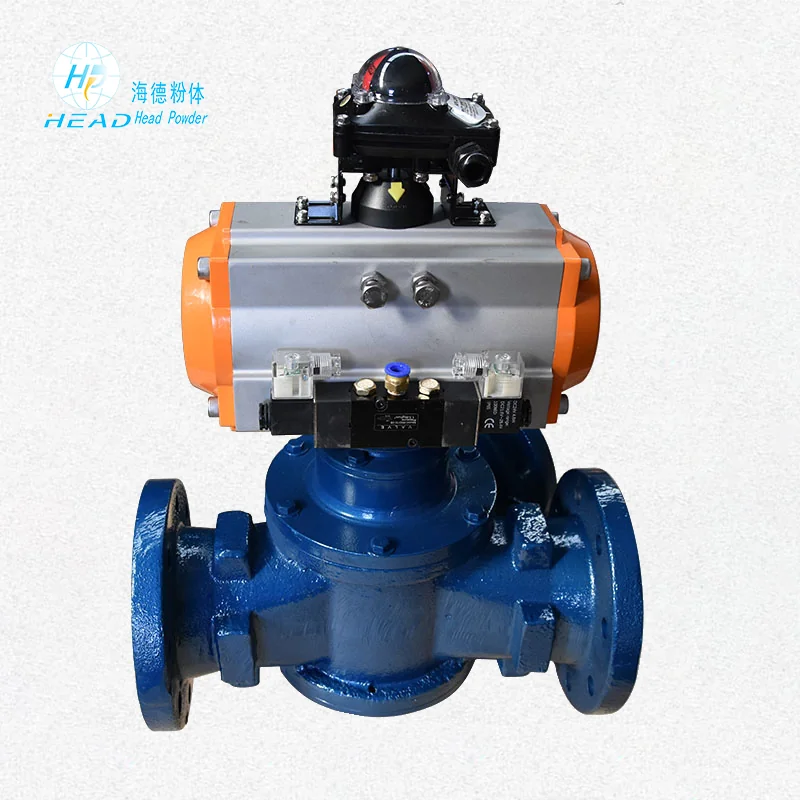
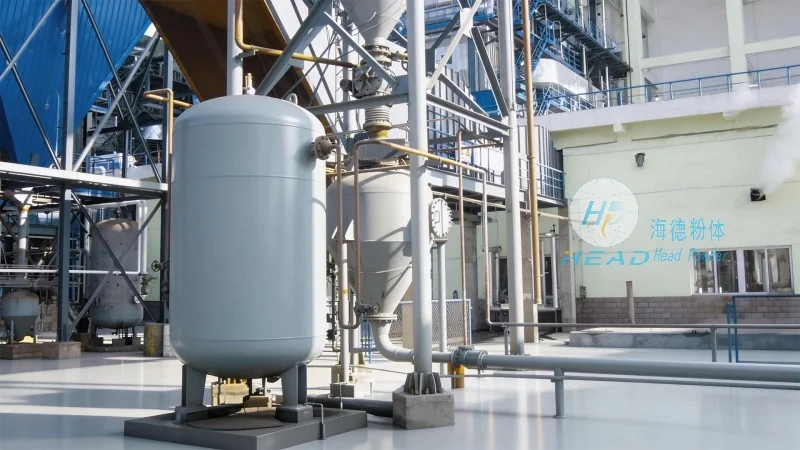
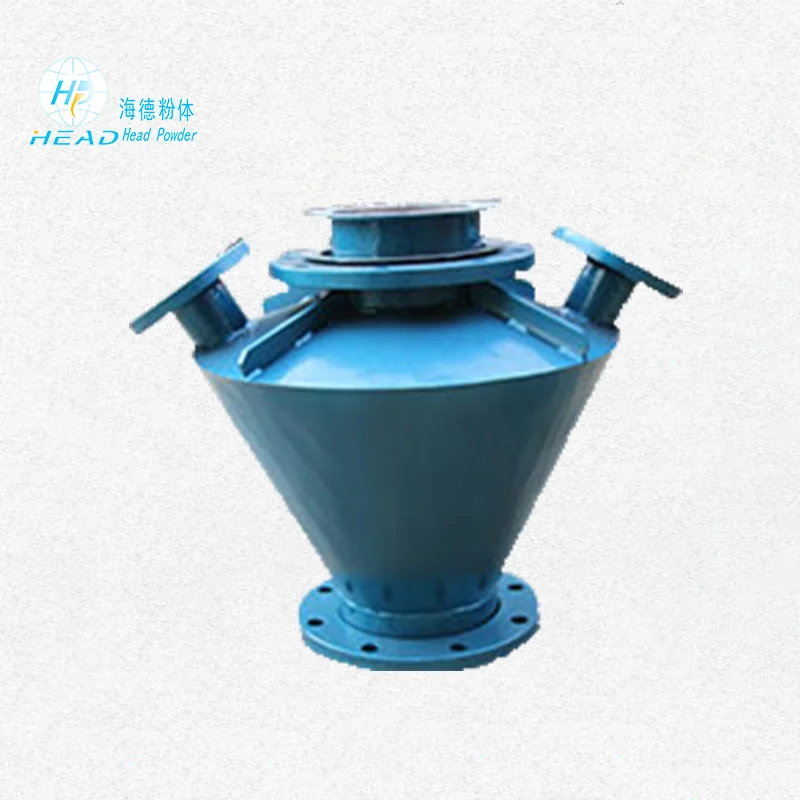
A robust suction pneumatic conveying system is composed of several critical components working in unison. The vacuum source is the heart of the system, determining the overall capacity and pressure rating. The conveying pipeline, usually made of galvanized steel or stainless steel, must be sized correctly to ensure optimal air-to-material ratios. Additionally, rotary airlocks and vacuum valves are essential for regulating the flow of material into the system without compromising the vacuum. Filtration systems are also a vital component, designed to capture fine particles from the exhaust air, ensuring compliance with environmental regulations. Engineers must carefully calculate the specific volume of air required to transport the material at the desired flow rate, taking into account the material's properties such as density, particle size, and abrasiveness.
Beyond environmental safety, the suction pneumatic conveying system is designed to protect the integrity of the material being transported. By utilizing a gentle conveying method, the system minimizes the impact and attrition of the product. This is particularly important for fragile materials or those with specific flow properties that can be easily degraded by mechanical handling equipment. The system's ability to operate continuously also contributes to high operational efficiency. With fewer moving parts compared to mechanical conveyors like screw or belt systems, maintenance requirements are generally lower, leading to reduced downtime and lower long-term operational costs.
When considering the implementation of a pneumatic conveying solution, partnering with an experienced engineering firm is essential. Shandong Headpowder Engineering Co., Ltd. is a distinguished manufacturer and supplier specializing in the design and production of advanced powder handling equipment. Headquartered in Shandong, China, the company has established a strong reputation for delivering high-quality pneumatic conveying systems tailored to meet the specific needs of diverse industries. The company combines technical expertise with innovative manufacturing processes to provide solutions that are both efficient and durable.
Shandong Headpowder Engineering Co., Ltd. focuses on the research and development of suction pneumatic conveying systems that offer exceptional performance. Their products are characterized by precision engineering, robust construction, and energy efficiency. The company understands that every project is unique, and therefore, they offer customized solutions that address specific challenges such as high-temperature transport, corrosive materials, or high-volume requirements. By leveraging their extensive industry knowledge, Headpowder ensures that every system delivered is optimized for reliability and longevity.
Located in the industrial hub of Shandong, Shandong Headpowder Engineering Co., Ltd. serves a global clientele. The company's commitment to quality is reflected in its adherence to international standards and its rigorous quality control processes. Whether the requirement is for a small-scale laboratory setup or a large-scale industrial plant, the company provides comprehensive support from the initial consultation and design phase through to installation, commissioning, and after-sales service. Their team of experienced engineers works closely with clients to ensure that the suction pneumatic conveying system integrates seamlessly into existing production lines.
For businesses seeking to optimize their material handling processes, Shandong Headpowder Engineering Co., Ltd. offers expert guidance and superior equipment. The company is dedicated to building long-term partnerships with its clients by providing reliable products and responsive service. To discuss your specific requirements or to request a detailed quotation, please contact the company directly. You may reach out to Manager Zhang, who will be happy to assist you with your inquiries and provide professional advice tailored to your operational needs.
Connecting with a leading provider like Shandong Headpowder Engineering Co., Ltd. is the first step towards enhancing your production efficiency. The company welcomes inquiries from potential clients around the world. To initiate a conversation regarding your pneumatic conveying project, please contact Manager Zhang via WeChat at 15662777102. The Headpowder team is ready to assist you in selecting the best suction pneumatic conveying system to meet your industrial demands.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top