

Principle and Working Scene Characteristics of Chocolate Material Pneumatic Conveying Equipment
Chocolate material pneumatic conveying equipment is a specialized system designed to handle and transport chocolate powders and related materials efficiently within industrial settings. As a key component in the chocolate production and processing chain, this equipment ensures the safe, hygienic, and reliable movement of chocolate ingredients from storage to processing lines. The technology behind these systems leverages the principles of pneumatic transport, which involves using air to move solid materials through a pipeline network. This approach is particularly advantageous for chocolate processing due to the delicate nature of the product, as it minimizes contamination risks and preserves the quality of the chocolate.
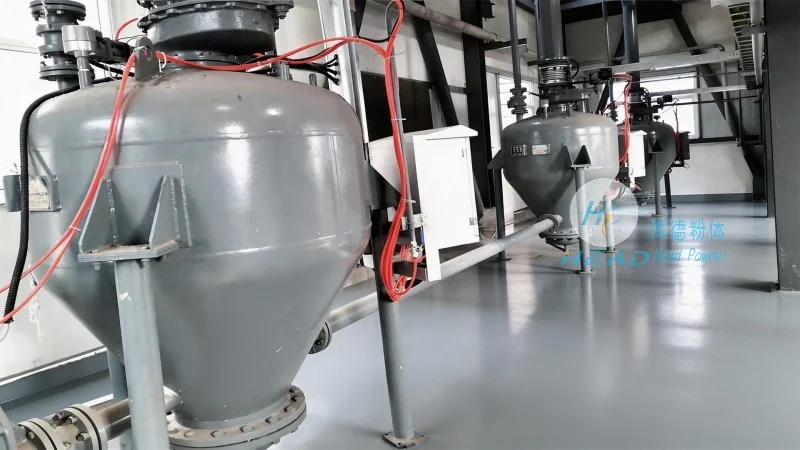
Principle of Pneumatic Conveying for Chocolate Materials
The core principle of chocolate material pneumatic conveying equipment is the use of air pressure to transport solid particles. In this system, chocolate powders or granules are introduced into a pipeline, where they are carried by a stream of air. The equipment typically operates under either positive pressure (where air is forced through the system) or negative pressure (where air is drawn out, creating a vacuum). For chocolate applications, positive pressure systems are more common as they offer better control over material flow and reduce the risk of dust contamination. The system consists of several key components, including a hopper for material storage, a feeder to control the flow rate, a conveying pipe network, and a receiver to collect the material at the destination. The air flow is managed by a blower or fan, which provides the necessary pressure to move the chocolate particles through the system. The design of the conveying line, including the pipe diameter, bends, and fittings, is critical to maintaining efficient and consistent material transport. Proper sizing and placement of these components ensure that the chocolate material moves smoothly without excessive pressure drop or particle degradation.
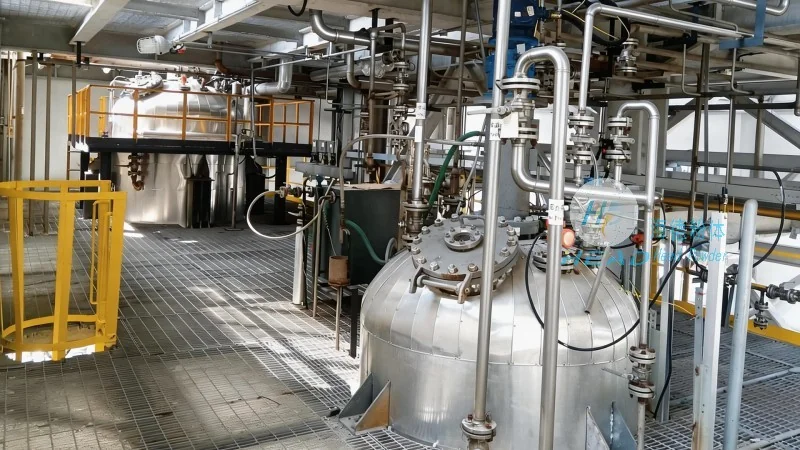
Working Scene Characteristics of Chocolate Material Pneumatic Conveying Equipment
The working scene characteristics of chocolate material pneumatic conveying equipment are tailored to meet the specific demands of chocolate production environments. These systems are commonly used in scenarios where chocolate powders need to be transported from bulk storage silos to processing machines, such as mixers, extruders, or coating lines. The equipment is designed to operate in clean, hygienic conditions, which is essential for maintaining the quality and safety of chocolate products. In industrial settings, the equipment is often integrated into larger production lines, allowing for seamless material transfer without manual handling. This integration enhances operational efficiency and reduces the risk of human error or contamination. The working scene also includes considerations for material handling speed and capacity. Chocolate material pneumatic conveying systems can handle varying flow rates, from low to high, depending on the production requirements. The equipment is capable of transporting chocolate powders over short to medium distances, typically up to several hundred meters, with minimal loss of material or quality. The system's ability to handle different particle sizes and moisture content makes it versatile for various chocolate formulations, including dark, milk, and white chocolate. Additionally, the equipment is designed to be easy to clean and maintain, which is crucial for compliance with food safety regulations. The working scene characteristics also highlight the importance of energy efficiency. Modern chocolate material pneumatic conveying systems are engineered to minimize energy consumption while maintaining optimal performance. This includes using efficient blower designs and optimizing the pipeline layout to reduce pressure losses. The overall working scene demonstrates how the equipment integrates into the chocolate production process, providing a reliable and efficient solution for material transport.
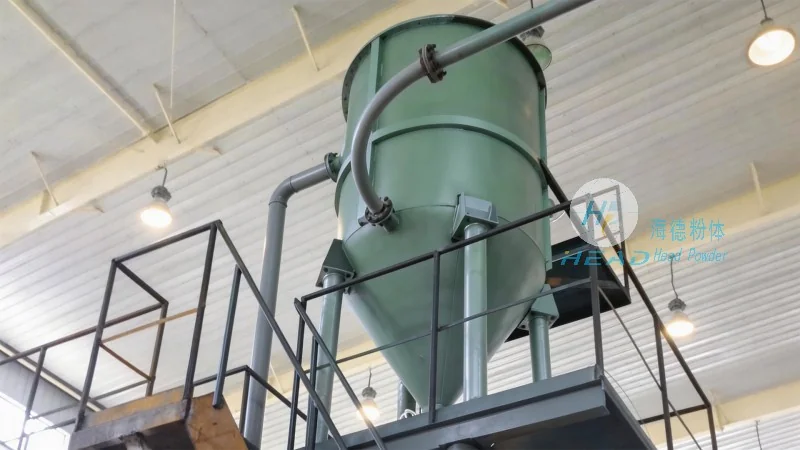
Key Features and Advantages in Chocolate Processing
Chocolate material pneumatic conveying equipment offers several key features and advantages that make it a preferred choice in the chocolate industry. One of the primary advantages is the hygienic nature of the system. By using enclosed pipelines and controlled air flow, the equipment prevents cross-contamination and maintains the purity of the chocolate material. This is particularly important in food processing, where product safety is a top priority. Another advantage is the ability to handle delicate chocolate powders without causing degradation. The gentle handling of the material ensures that the texture and flavor of the chocolate are preserved, which is critical for maintaining product quality. The equipment also offers flexibility in terms of material handling. It can transport various chocolate formulations, including powders, granules, and even small chunks, depending on the system design. This versatility allows manufacturers to use the same equipment for different chocolate products, reducing the need for multiple handling systems. Additionally, the system provides a compact and space-efficient solution for material transport. Unlike traditional bulk handling methods, such as conveyor belts or elevators, pneumatic conveying systems can be installed in confined spaces, making them suitable for modern industrial facilities with limited floor space. The equipment is also designed for easy integration with other production equipment, such as mixers and extruders, allowing for a streamlined production process. The overall key features and advantages of chocolate material pneumatic conveying equipment highlight its role in enhancing the efficiency, safety, and quality of chocolate production.
Application Examples in Chocolate Production
Chocolate material pneumatic conveying equipment is widely used in various applications within chocolate production facilities. One common application is the transfer of chocolate powders from bulk storage silos to mixing machines. In this scenario, the equipment ensures that the chocolate material is delivered to the mixer in a controlled and consistent manner, which is essential for achieving uniform product quality. Another application is the transport of chocolate granules from a processing line to a packaging station. The system efficiently moves the granules through the pipeline, reducing the need for manual handling and minimizing the risk of product damage. Additionally, the equipment is used in the production of chocolate coatings, where it transports the coating material to the coating line. The system's ability to handle different particle sizes and moisture content makes it suitable for various coating formulations, including dark and milk chocolate coatings. The application examples also include the use of the equipment in chocolate confectionery production, where it transports ingredients to the extrusion or molding machines. The equipment's reliability and efficiency make it a critical component in these production processes, ensuring that the chocolate products meet the required quality standards. The overall application examples demonstrate the versatility and importance of chocolate material pneumatic conveying equipment in the chocolate industry, supporting various production stages and enhancing overall operational efficiency.
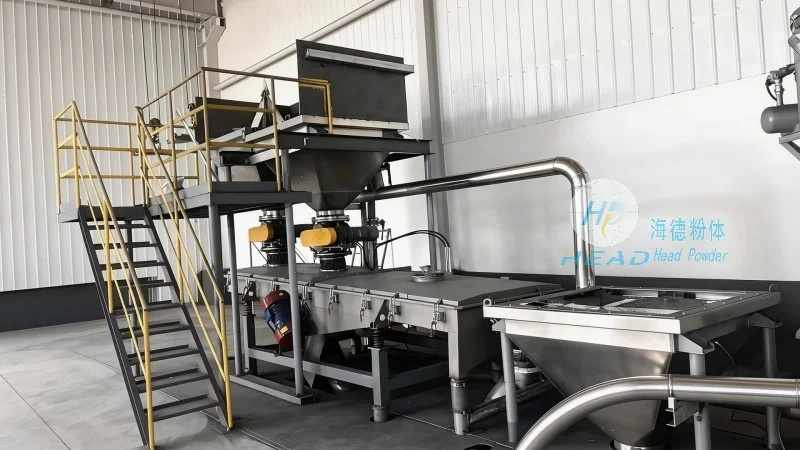
Conclusion and Company Overview
Chocolate material pneumatic conveying equipment plays a vital role in modern chocolate production, providing an efficient and hygienic solution for material transport. The principles of pneumatic transport, combined with specialized design considerations for chocolate materials, ensure that the equipment meets the demanding requirements of the industry. The working scene characteristics, including its ability to handle delicate materials and operate in clean environments, make it an essential component in chocolate processing facilities. The key features and advantages, such as hygienic operation and flexibility, further enhance its value to manufacturers. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality chocolate material pneumatic conveying systems. With a focus on innovation and customer satisfaction, the company delivers equipment that meets the specific needs of chocolate producers, ensuring optimal performance and reliability. HeadPowder's commitment to quality and efficiency has made it a trusted partner in the chocolate industry, supporting manufacturers in achieving their production goals while maintaining the highest standards of product quality and safety. Based in Shandong, China, HeadPowder leverages its expertise and experience to provide tailored solutions for chocolate material handling, contributing to the success of its clients in the competitive chocolate market.