With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and supply of advanced material handling systems tailored for calcite processing applications. Our expertise lies in creating efficient and reliable equipment that addresses the unique challenges of calcite material handling, ensuring optimal performance in various industrial settings. With a strong commitment to innovation and quality, HeadPowder has established itself as a trusted partner in the calcite industry, providing solutions that enhance operational efficiency and product quality.
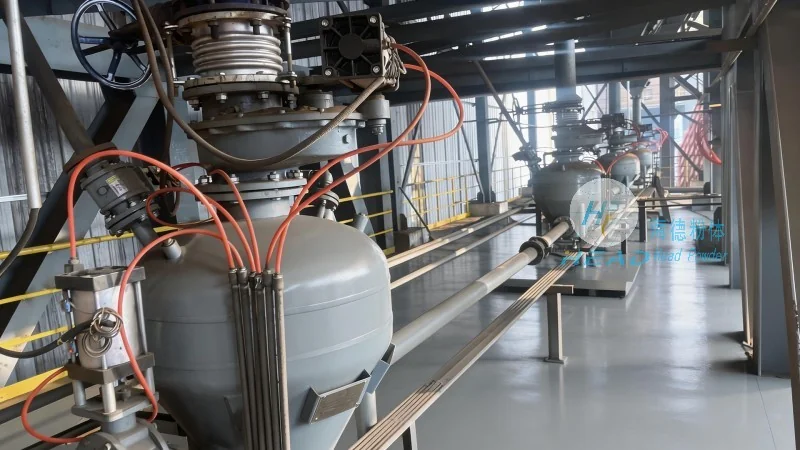
Calcite, a widely used calcium carbonate mineral, is essential in industries such as construction, pharmaceuticals, and food processing. The efficient transportation of calcite from extraction sites to processing facilities is critical for maintaining production efficiency and product quality. At HeadPowder, we understand these demands and have engineered specialized equipment to meet them. Our systems are designed to handle the physical properties of calcite, including its particle size, density, and flow characteristics, ensuring smooth and consistent material movement throughout the production line. The systems are built with durability and reliability in mind, capable of withstanding the rigorous demands of industrial operations.
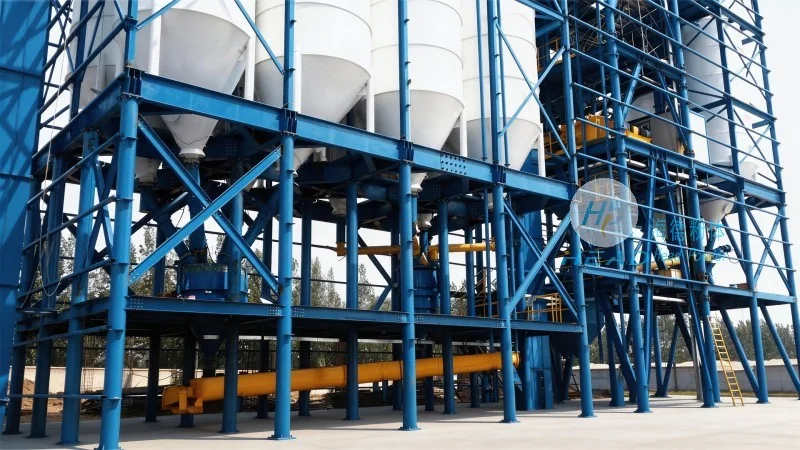
The core of our calcite material handling systems involves several key components that work in tandem to ensure seamless operation. The primary components include feeders, conveyors, and control systems. The working principle is based on mechanical energy transfer, where materials are moved through a series of mechanisms such as screw conveyors, belt conveyors, or pneumatic systems. Each component is engineered to handle the specific characteristics of calcite, minimizing friction and wear while maximizing throughput. For instance, our screw conveyors are designed with smooth, corrosion-resistant surfaces to prevent calcite buildup and ensure consistent material flow. The control systems are equipped with advanced sensors and automation features that monitor and adjust the system's performance in real-time, optimizing energy consumption and operational efficiency. Additionally, the systems incorporate safety features to prevent overloading and material blockages, ensuring continuous and safe operation.
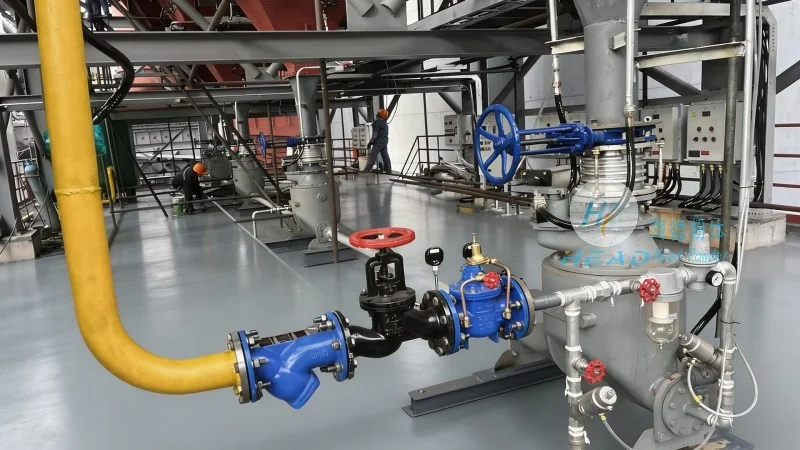
Our calcite material handling systems are versatile and adaptable to a wide range of working environments. They are commonly used in mining operations, where calcite is extracted from quarries and transported to processing plants. The systems are also suitable for industrial plants that require continuous material supply for production processes. The design allows for easy integration into existing production lines, reducing downtime and increasing overall productivity. Additionally, the systems are built to withstand harsh conditions, such as high humidity and dust, which are common in calcite processing facilities. This adaptability makes our equipment ideal for both small-scale and large-scale operations, catering to the diverse needs of the calcite industry. The systems are also designed with modular components, allowing for easy maintenance and replacement of parts, further enhancing their longevity and reliability.
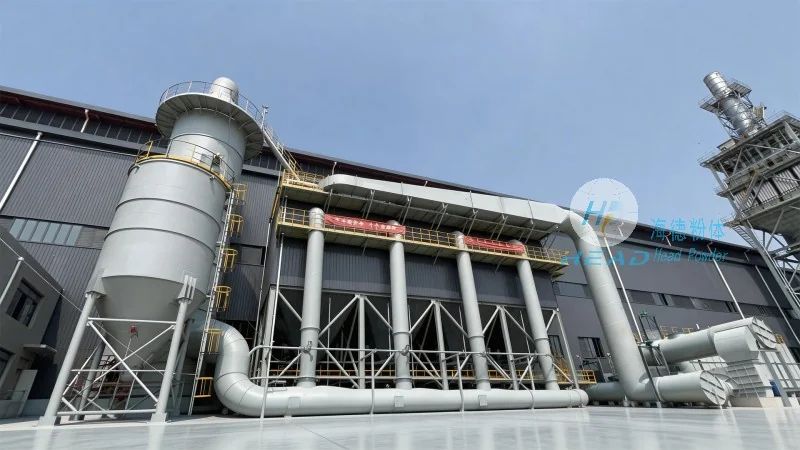
HeadPowder's calcite material handling systems have been successfully implemented in various applications across different industries. In the construction sector, our equipment is used to transport calcite for cement production, where consistent material flow is crucial for maintaining product quality. The systems have demonstrated high throughput rates, often exceeding 500 tons per hour, while consuming less energy compared to traditional methods. In the pharmaceutical industry, the systems ensure that calcite is delivered to processing units with minimal contamination, meeting stringent quality standards. The performance of our systems is measured by key indicators such as throughput capacity, energy efficiency, and maintenance frequency. Our systems typically achieve high throughput rates while consuming less energy compared to traditional methods. The durability of our equipment, combined with low maintenance requirements, results in long-term cost savings for our clients. Furthermore, the systems are designed with safety features to protect operators and prevent material spills, ensuring a secure working environment. Clients have reported significant improvements in production efficiency and reduced operational costs after implementing our calcite material handling systems.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top